Explore our flagship heavy-duty racking, automated shuttle systems, and precision-engineered logistics infrastructure.


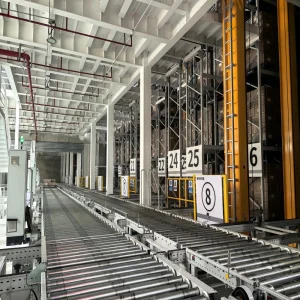
The global industrial packaging machinery and intelligent material handling sector is undergoing a profound paradigm shift driven by e-commerce velocity, supply chain localization, labor cost inflation, and the imperative for real-time inventory visibility. Industrial enterprises are transitioning from static, fragmented storage infrastructures to interconnected, highly automated, and modular packaging and racking ecosystems. In modern industrial operations, packaging machinery and high-density warehouse storage are no longer isolated silos; they form a unified continuous throughput pipeline.
According to recent industrial whitepaper data, the global packaging machinery market is expanding at a CAGR of 5.8%, while automated material handling systems (AMHS) and automated storage/retrieval systems (AS/RS) are surging at over 9.4% annually. Key vectors driving this evolution include:
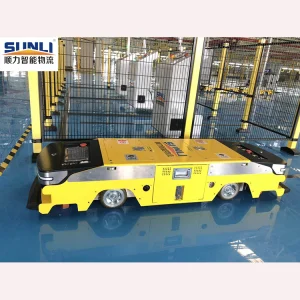
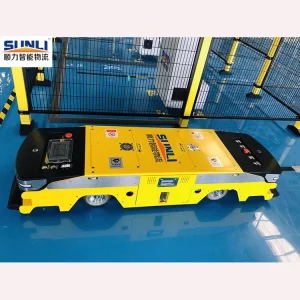
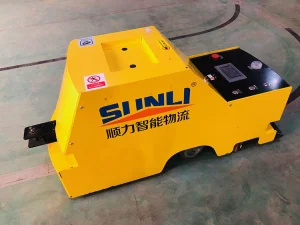
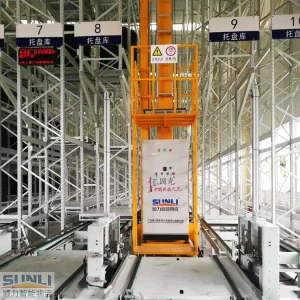
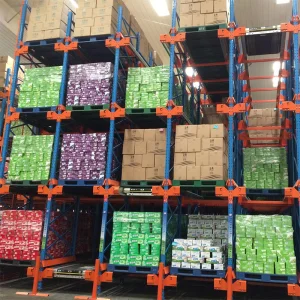
Seamless integration between end-of-line secondary packaging machines (palletizers, shrink wrappers, strapping systems) and automated radio shuttle racks or AGV (Automated Guided Vehicle) transport systems.
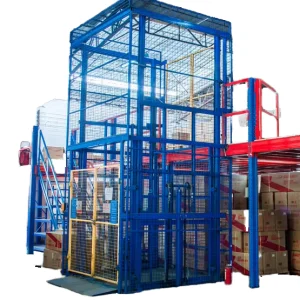
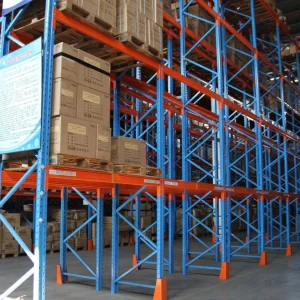
Maximizing vertical cubic utilization in expensive logistics hubs via self-supporting warehouse structures, heavy-duty mezzanine levels, and ultra-narrow aisle (UNA) high-bay pallet racking.
Enhanced engineering compliance to sustain seismic forces, dynamic load distributions, electrostatic discharge (ESD) protection for electronics, and extreme corrosion resistance for cold-chain facilities.
Shenzhen Sunli Intelligent Logistics Equipment Co., Ltd. stands as a benchmark manufacturer and systemic solution provider within the global industrial storage and material handling equipment industry.
Established in 2015, Shenzhen Sunli Intelligent Logistics Equipment Co., Ltd. is a leading manufacturer specializing in heavy-duty industrial racking and smart warehouse storage solutions. Operating from a modern production facility spanning 38,000 m², we leverage over 12 years of industry experience and 8 years of international trade expertise to serve global logistics and industrial sectors. Our high-performance storage solutions generate an annual export revenue ranging between $18 million and $25 million, with core markets spanning North America, Western Europe, Southeast Asia, and the Middle East.
Quality and precision are central to our operations. Our dynamic team of 35 dedicated QC professionals implements rigorous product inspection methods, including full raw material load-bearing analysis, high-precision weld seam testing, and comprehensive anti-corrosion powder-coating thickness checks. Driven by strong R&D capabilities, our team of 28 skilled R&D engineers continuously innovates to meet evolving supply chain requirements, introducing over 120 new products and structural improvements annually.
We offer extensive OEM/ODM custom options, including tailored load capacities, custom rack dimensions, color powder coatings, and fully integrated automated shuttle systems (AS/RS). Backed by a strong network of over 800 supply chain partners, we primarily partner with large-scale 3PL providers, industrial distributors, ecommerce logistics hubs, and global retail enterprises to deliver reliable, efficient, and scalable storage infrastructure worldwide.
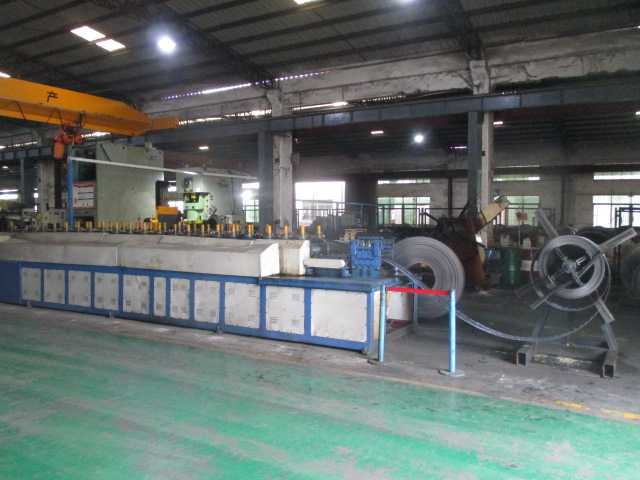
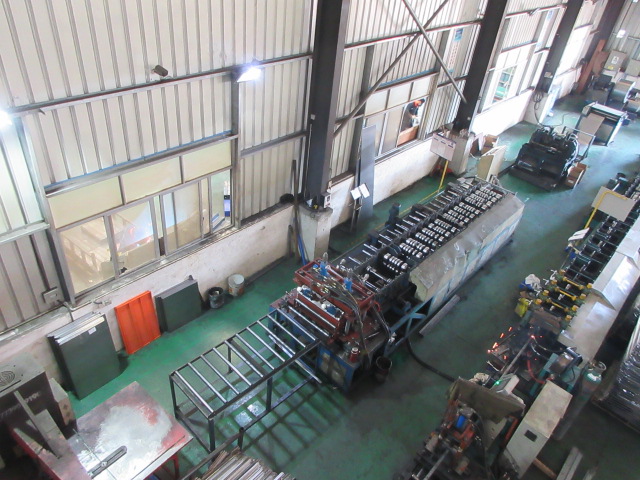
Our 38,000 m² manufacturing facility incorporates fully automated cold-roll forming, robotic continuous welding, multi-stage surface pre-treatment, and computerized thermosetting powder coating lines. This state-of-the-art infrastructure enables Sunli to maintain precise physical tolerances, high throughput capacities, and consistent structural integrity across millions of steel members annually.
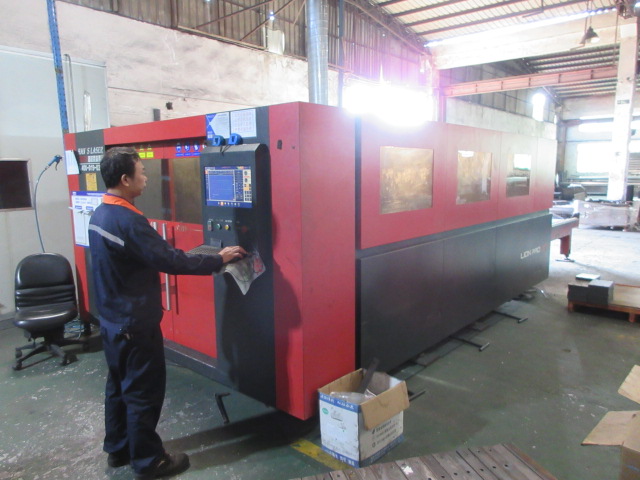
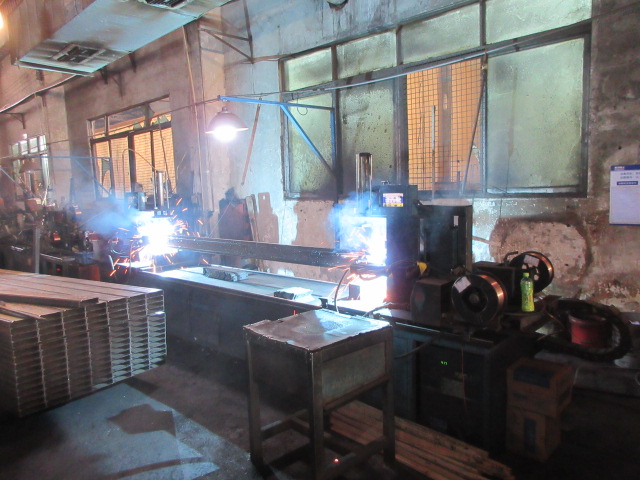
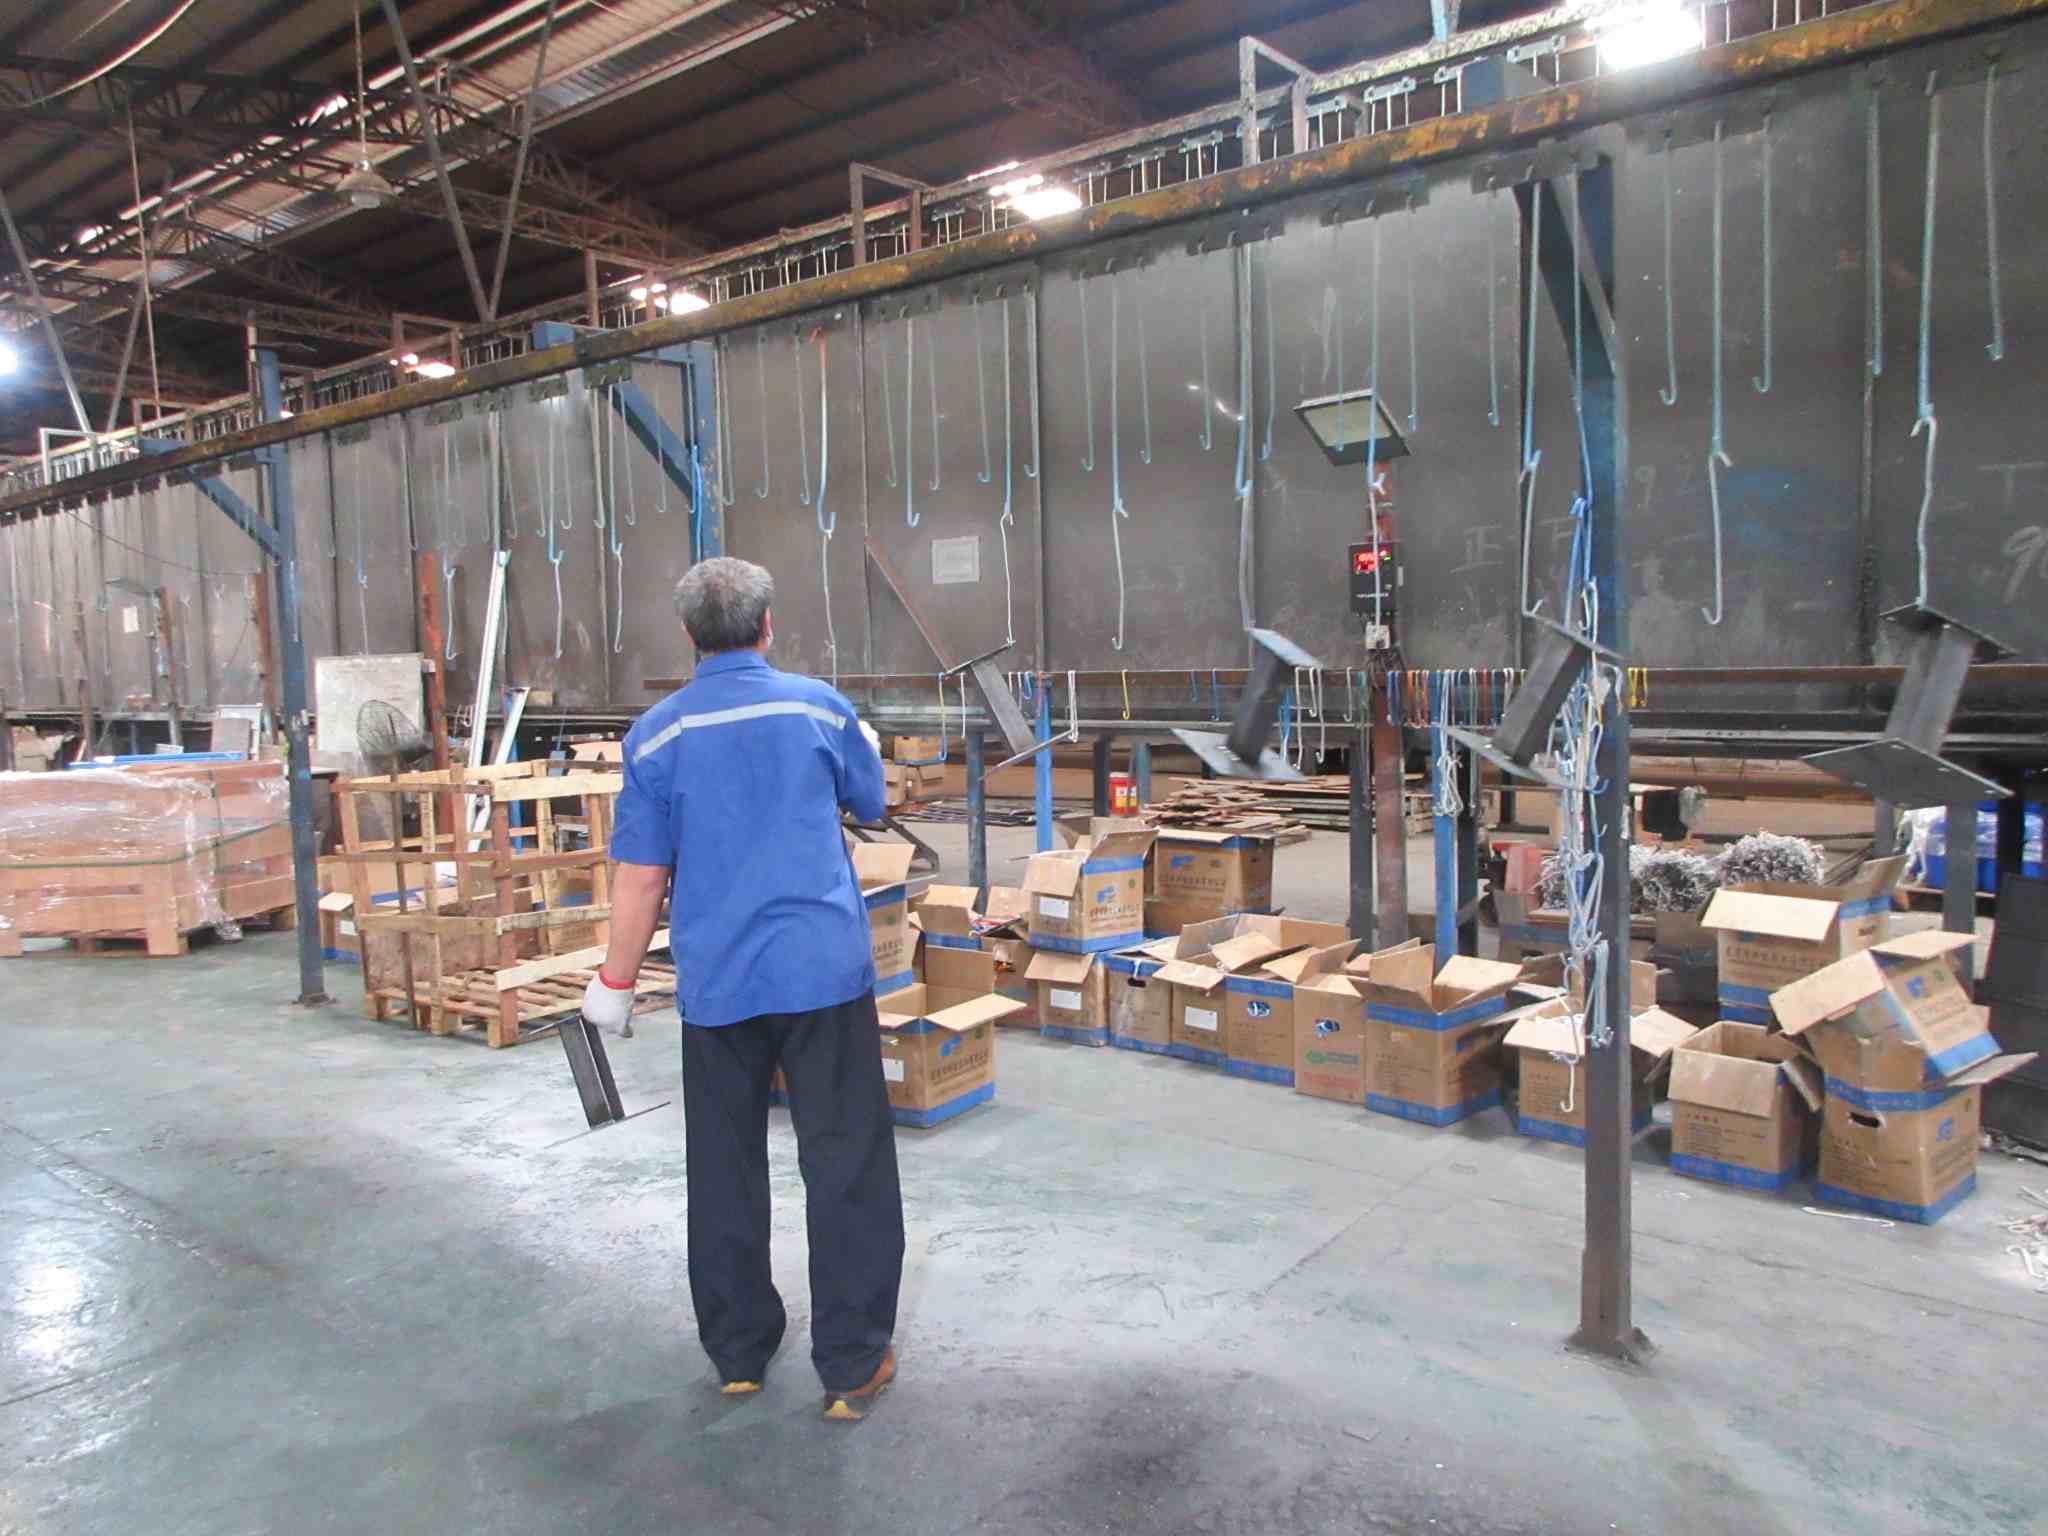
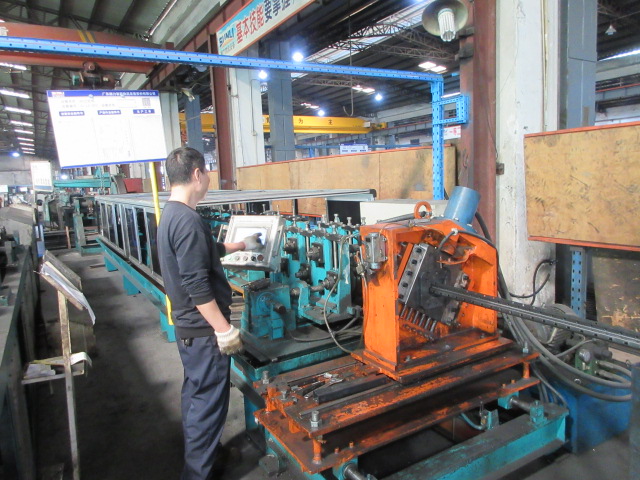
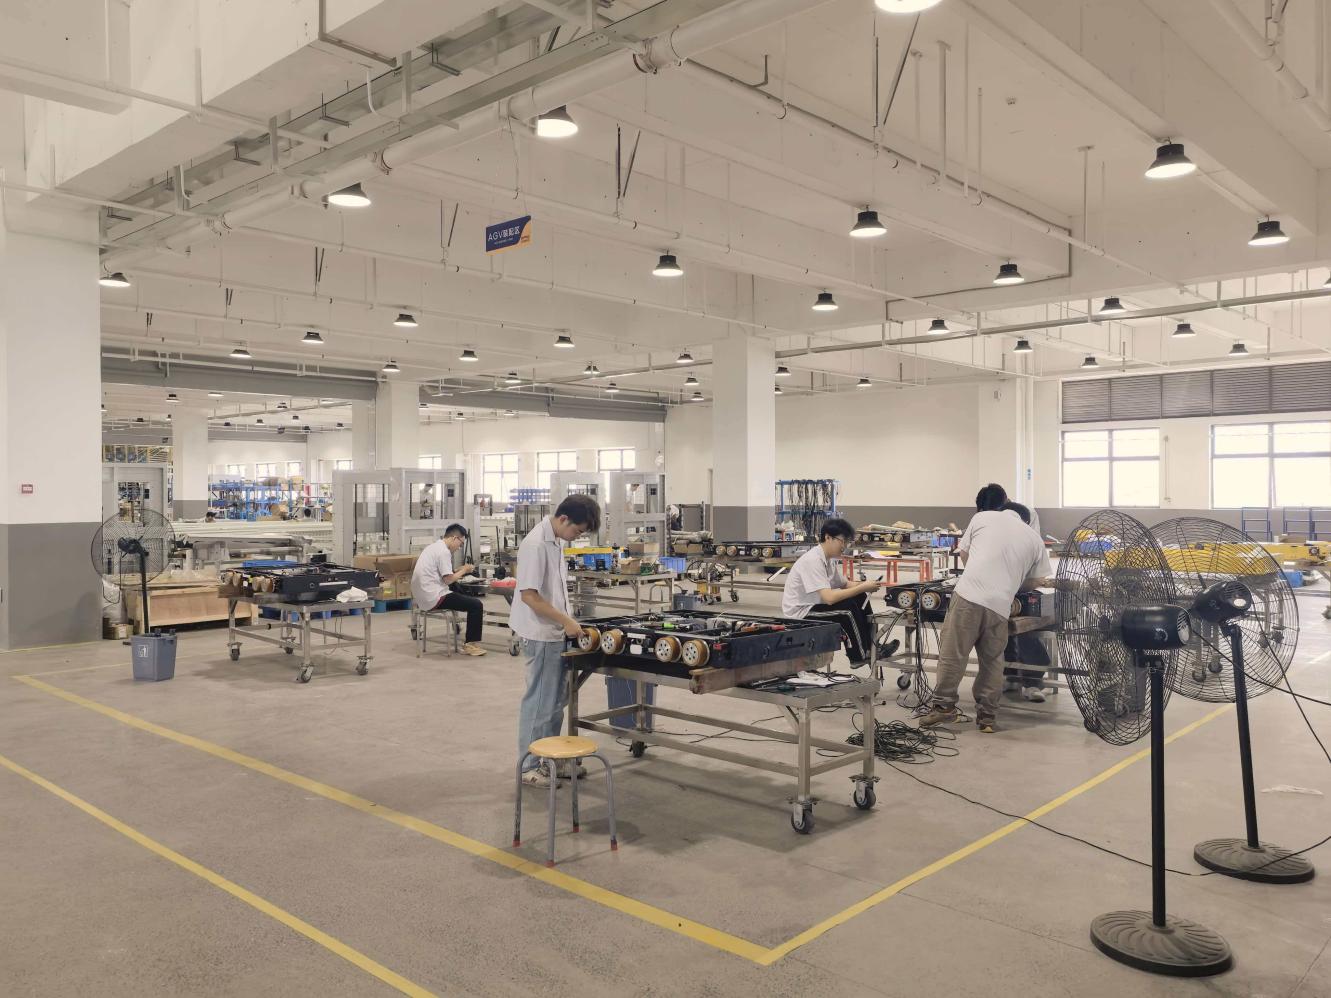
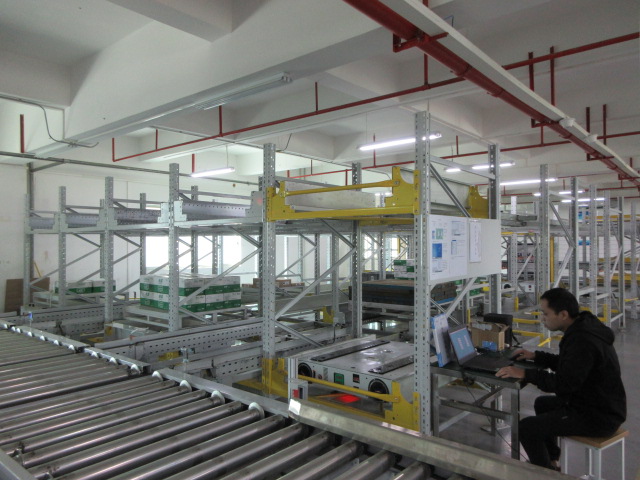
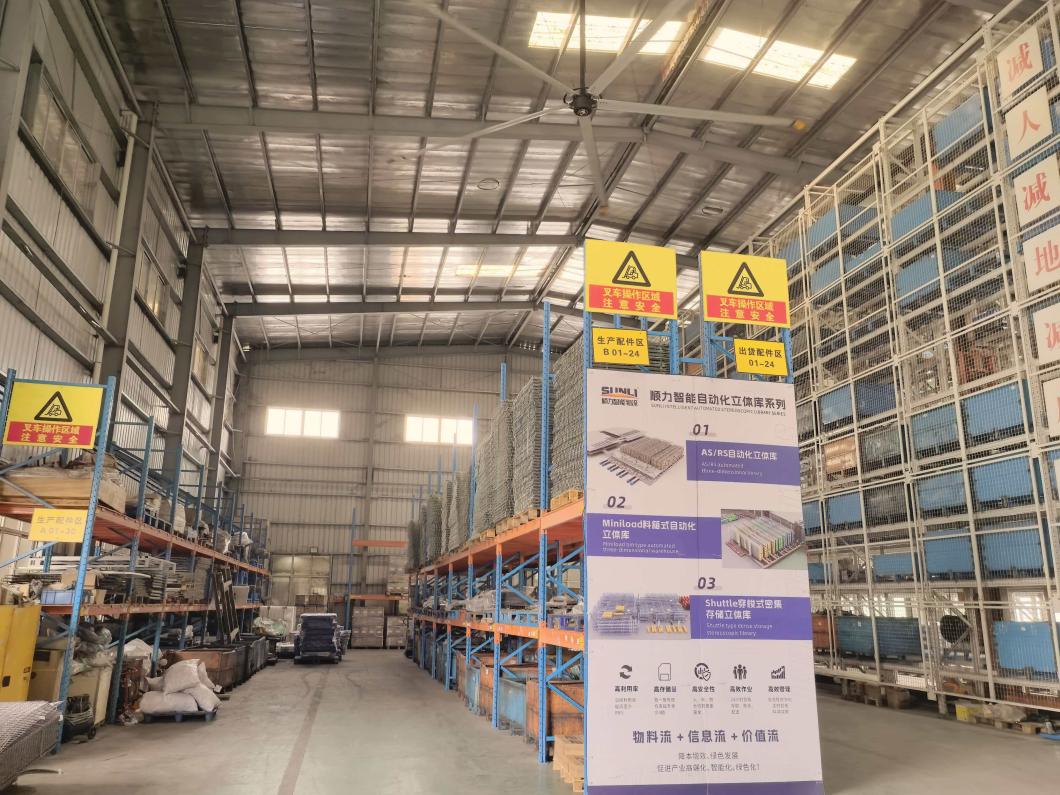
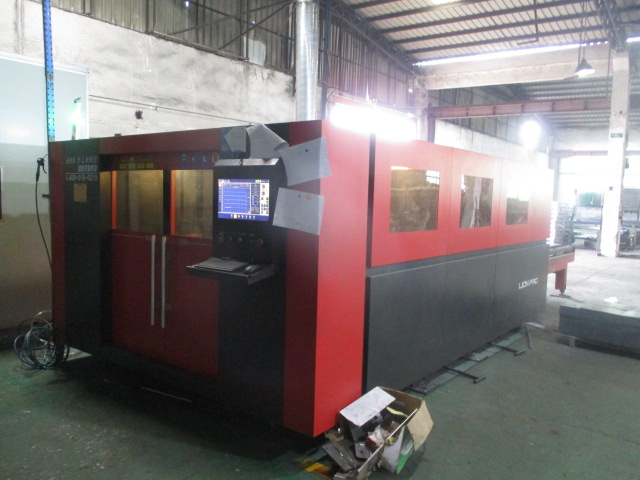
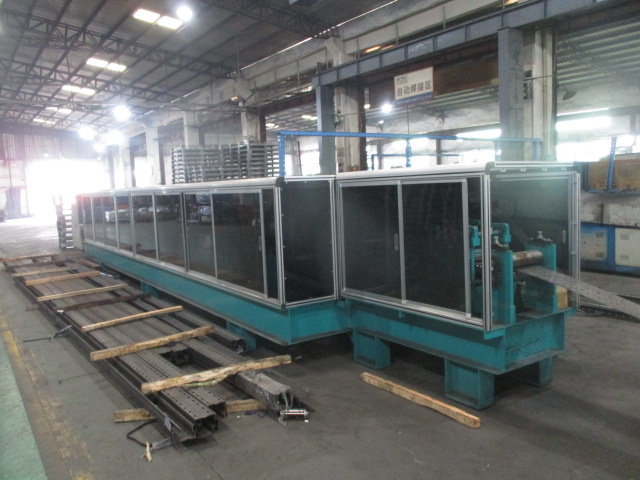
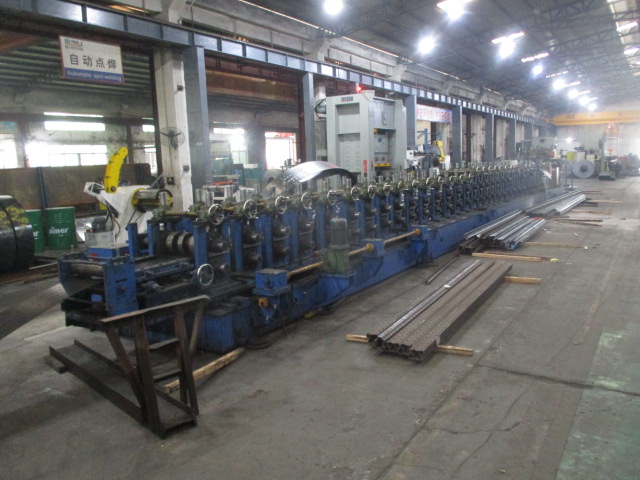
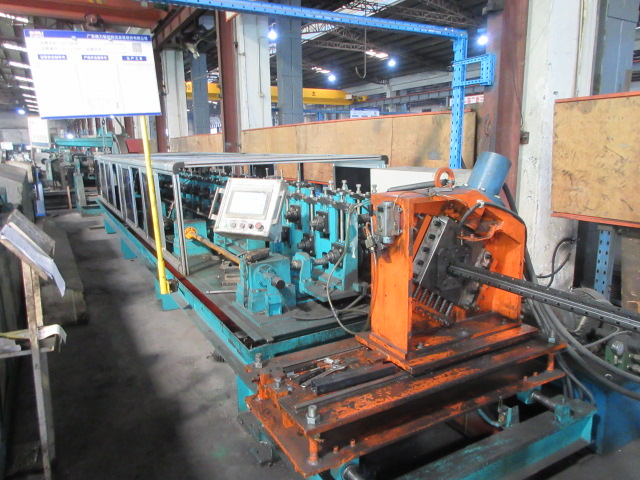
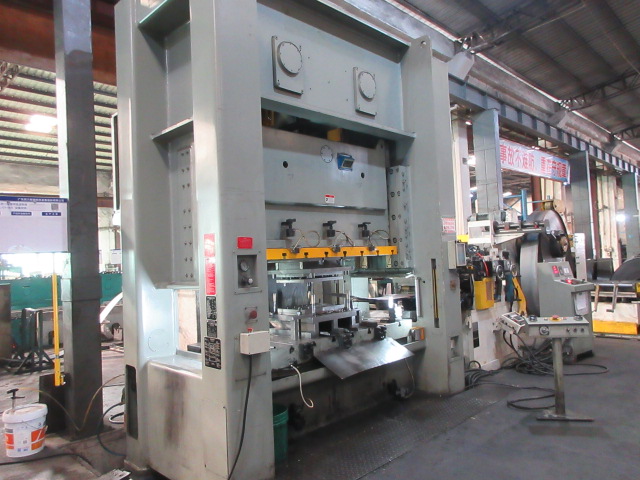
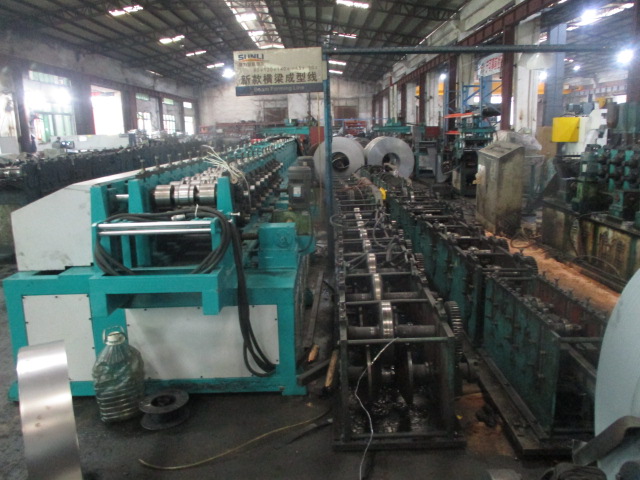
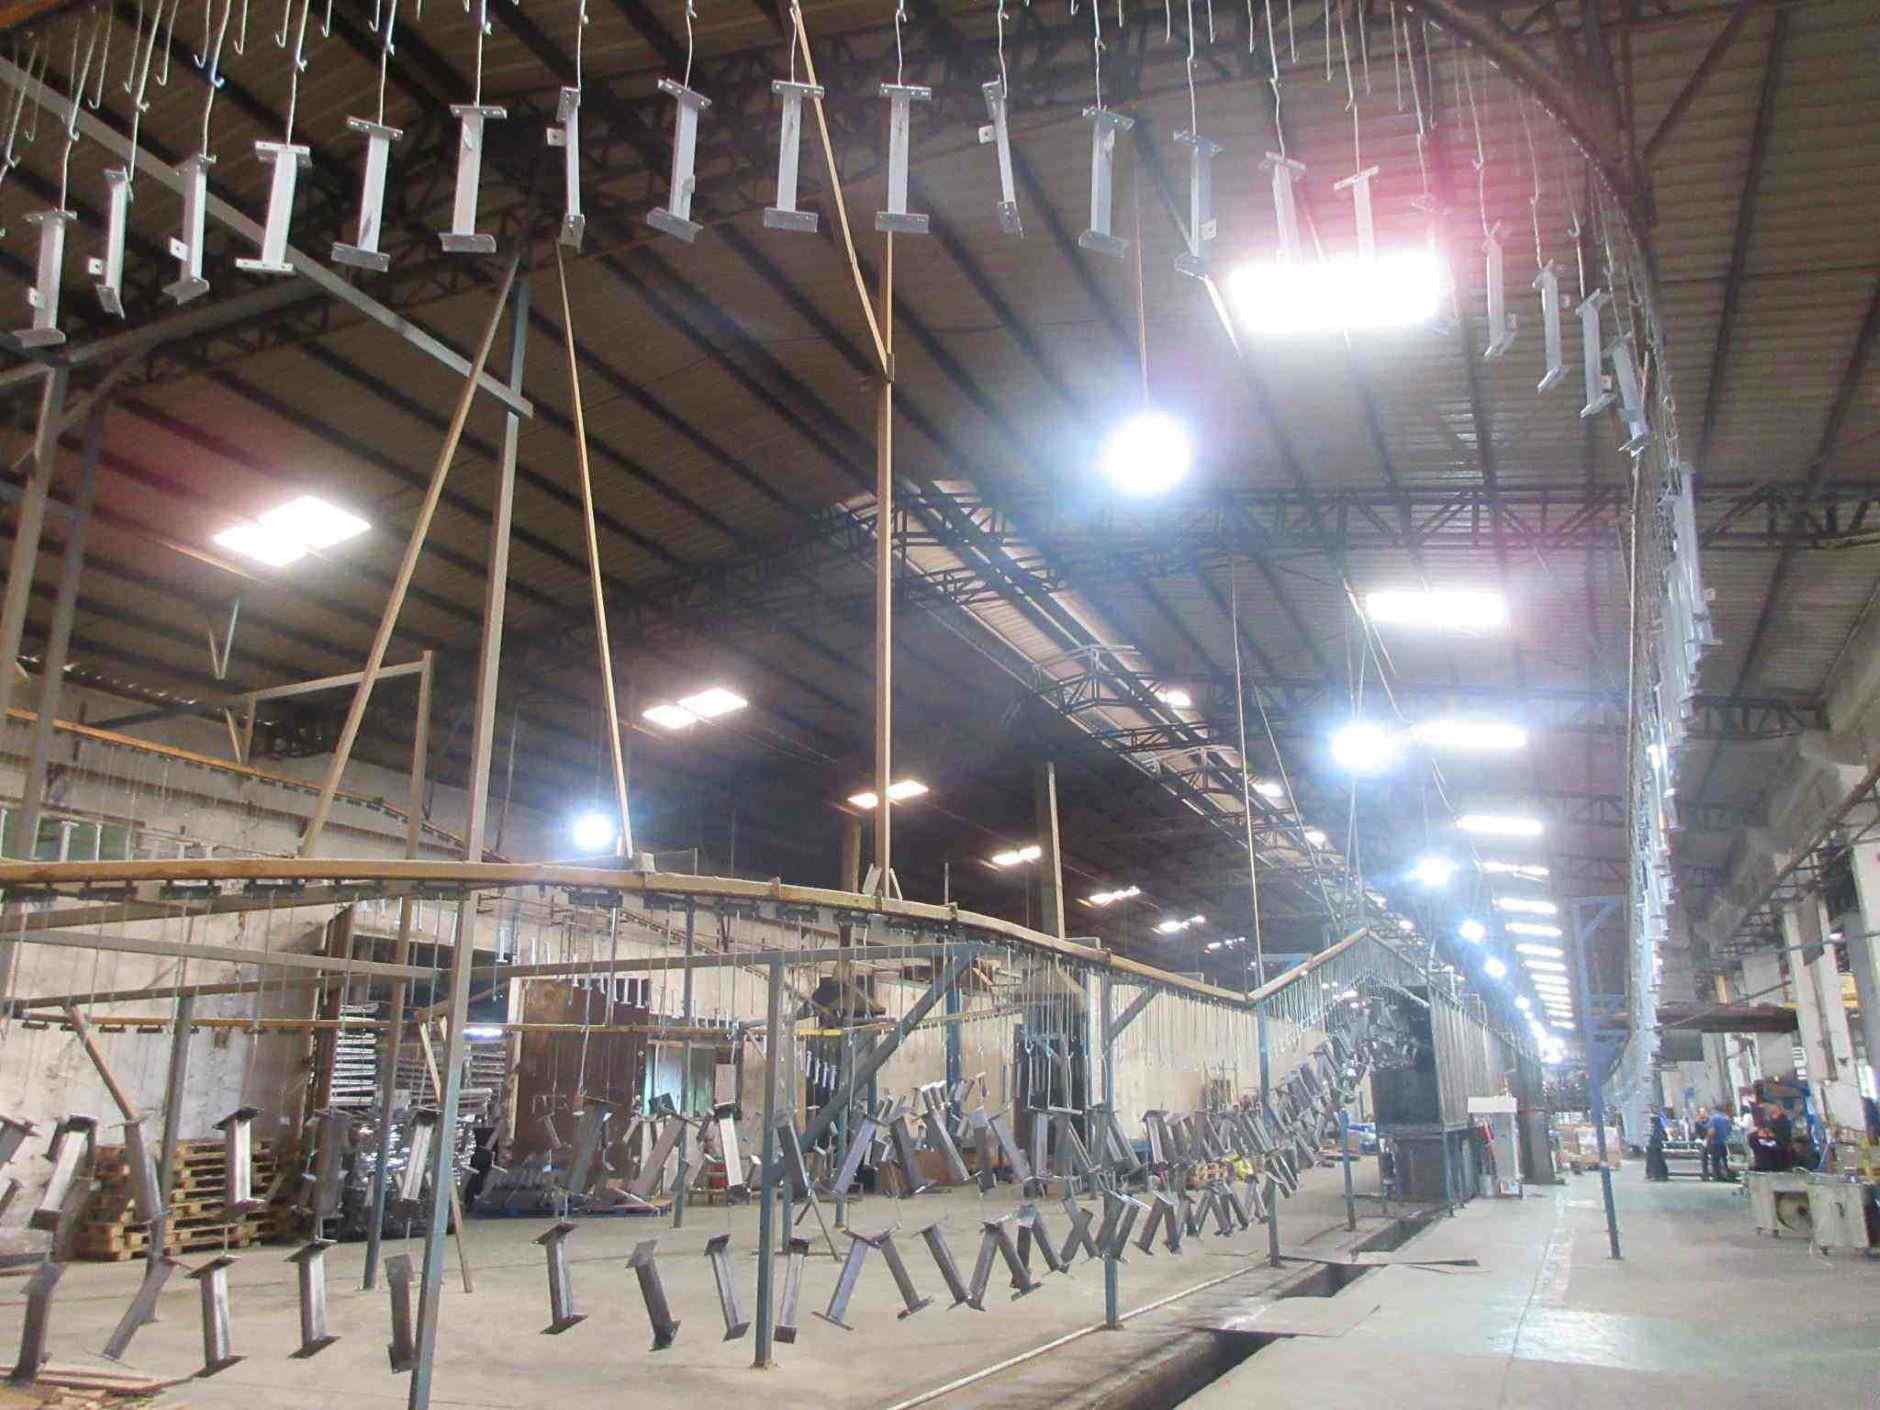
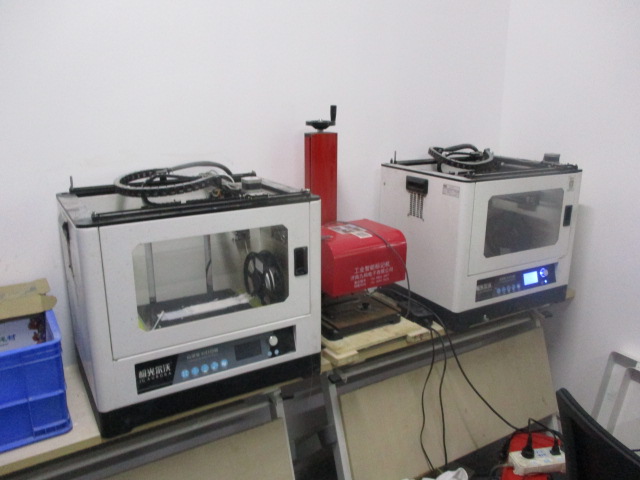
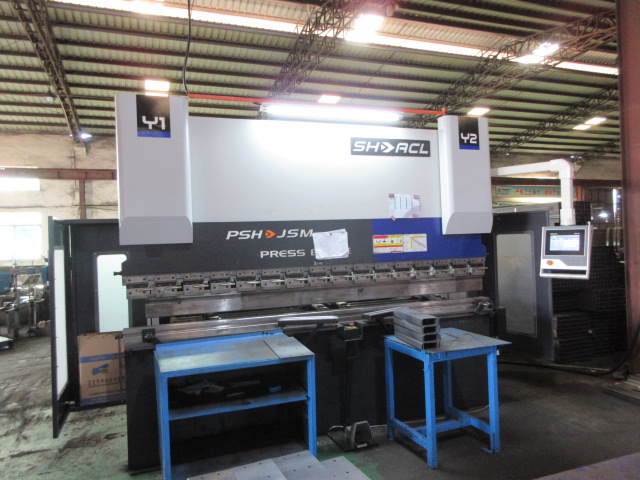
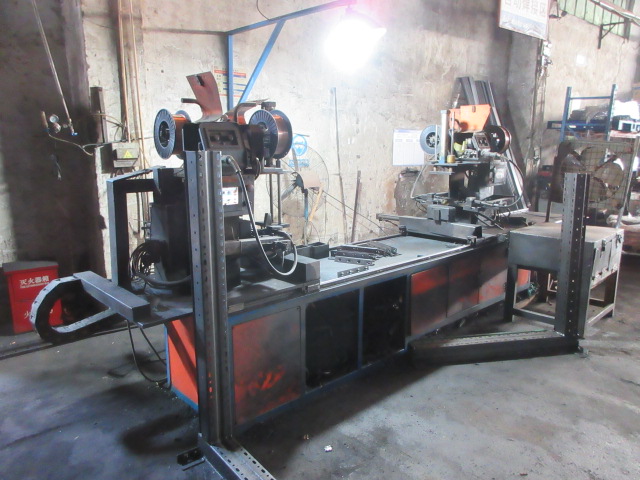
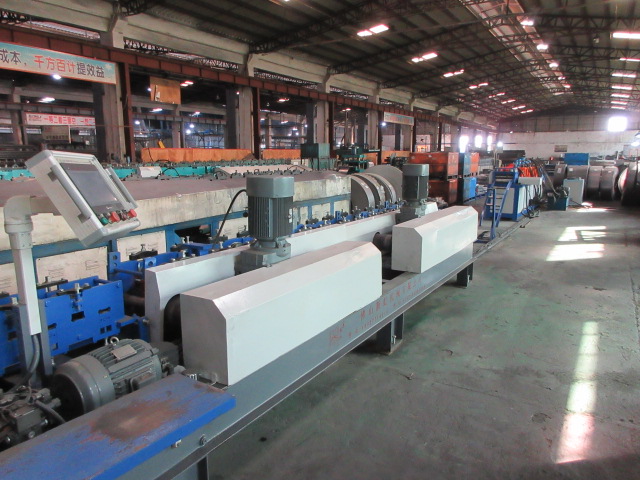
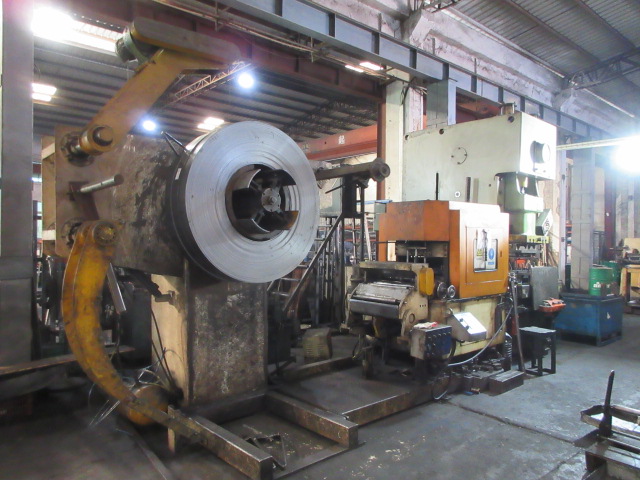
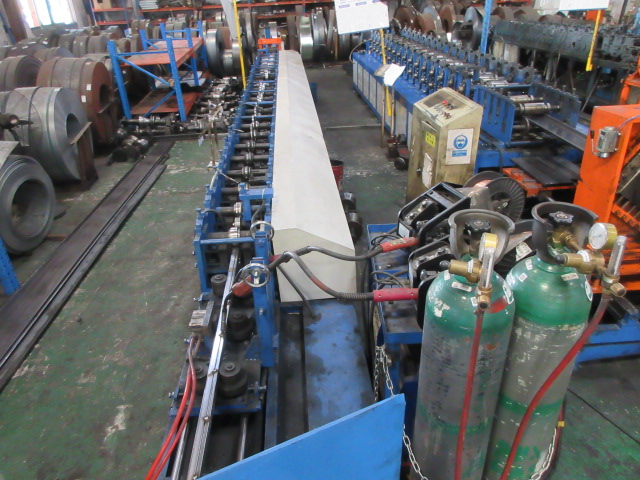
To comply with rigorous FEM 10.2.02, RMI, and ISO 9001 quality frameworks, Sunli maintains a state-of-the-art metrology laboratory. Our 35-member QC department performs continuous statistical process control (SPC) covering chemical composition, structural deformation, coating adhesion, and dynamic torque capacity.
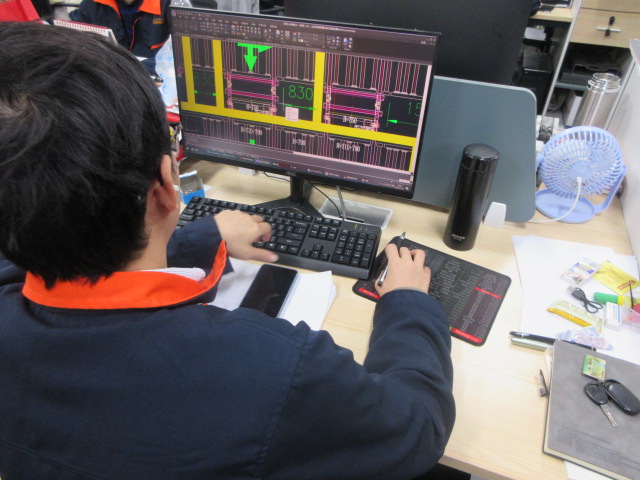
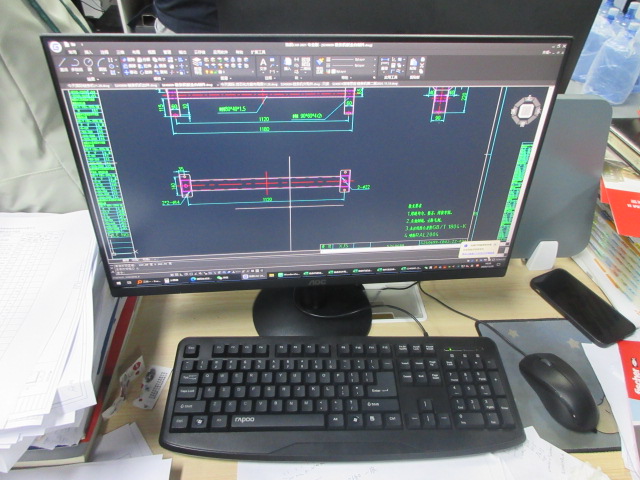
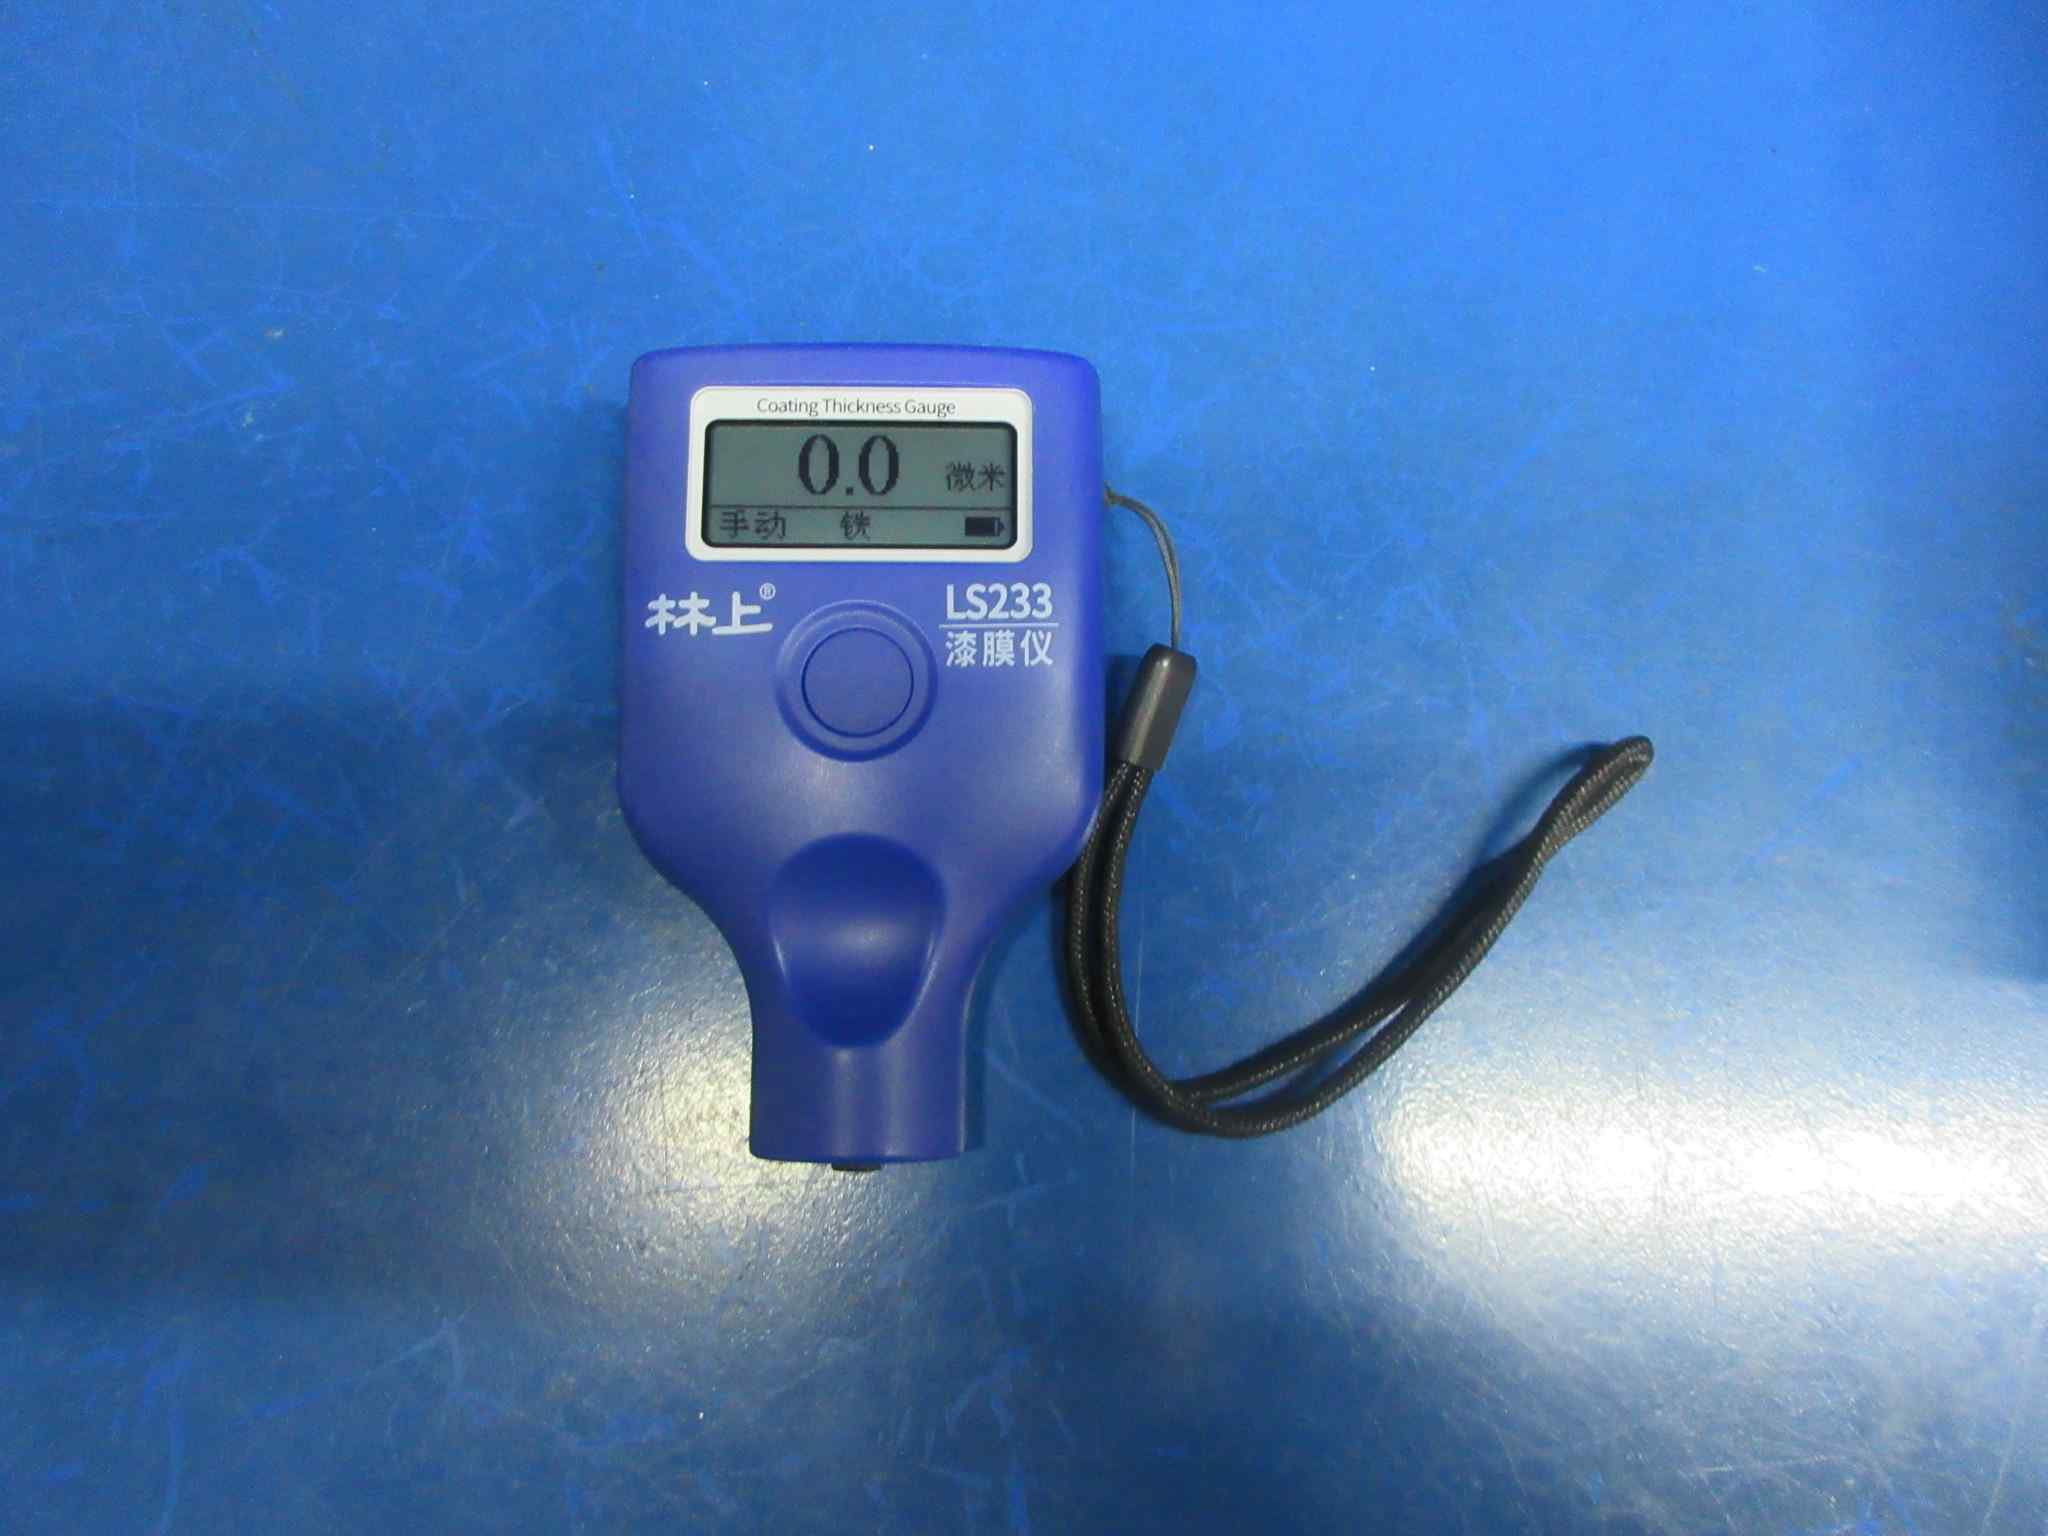
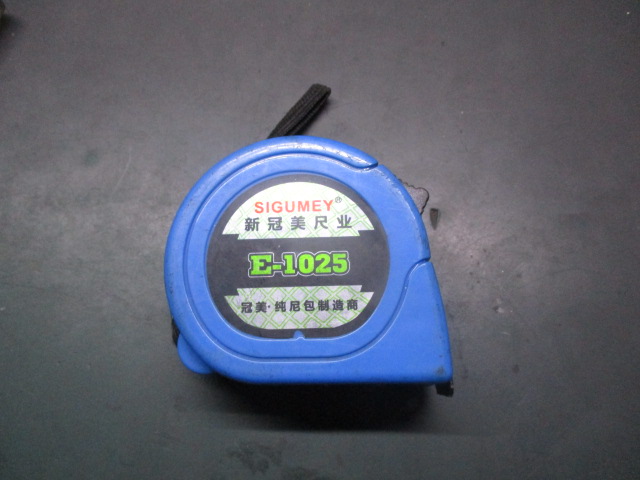
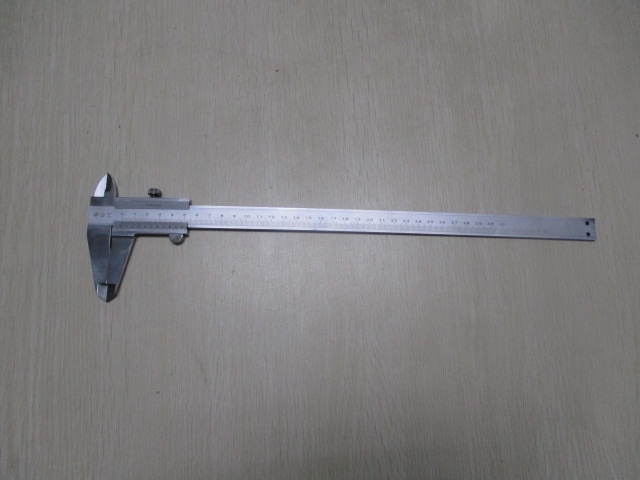
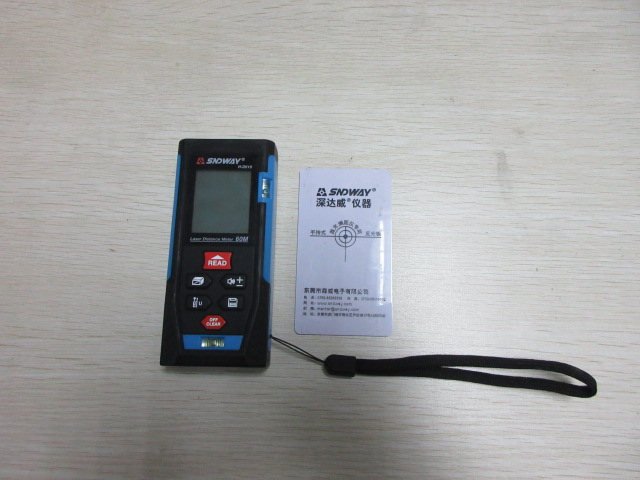
Global enterprise procurement directors choose Shenzhen Sunli as their strategic OEM/ODM partner due to China’s unmatched industrial ecosystem density, technological maturity, and integrated supply chain efficiencies. The Shenzhen-Guangdong industrial belt provides access to high-grade cold-rolled steel mills, precision tool makers, and advanced electronics suppliers within a 50-kilometer radius.
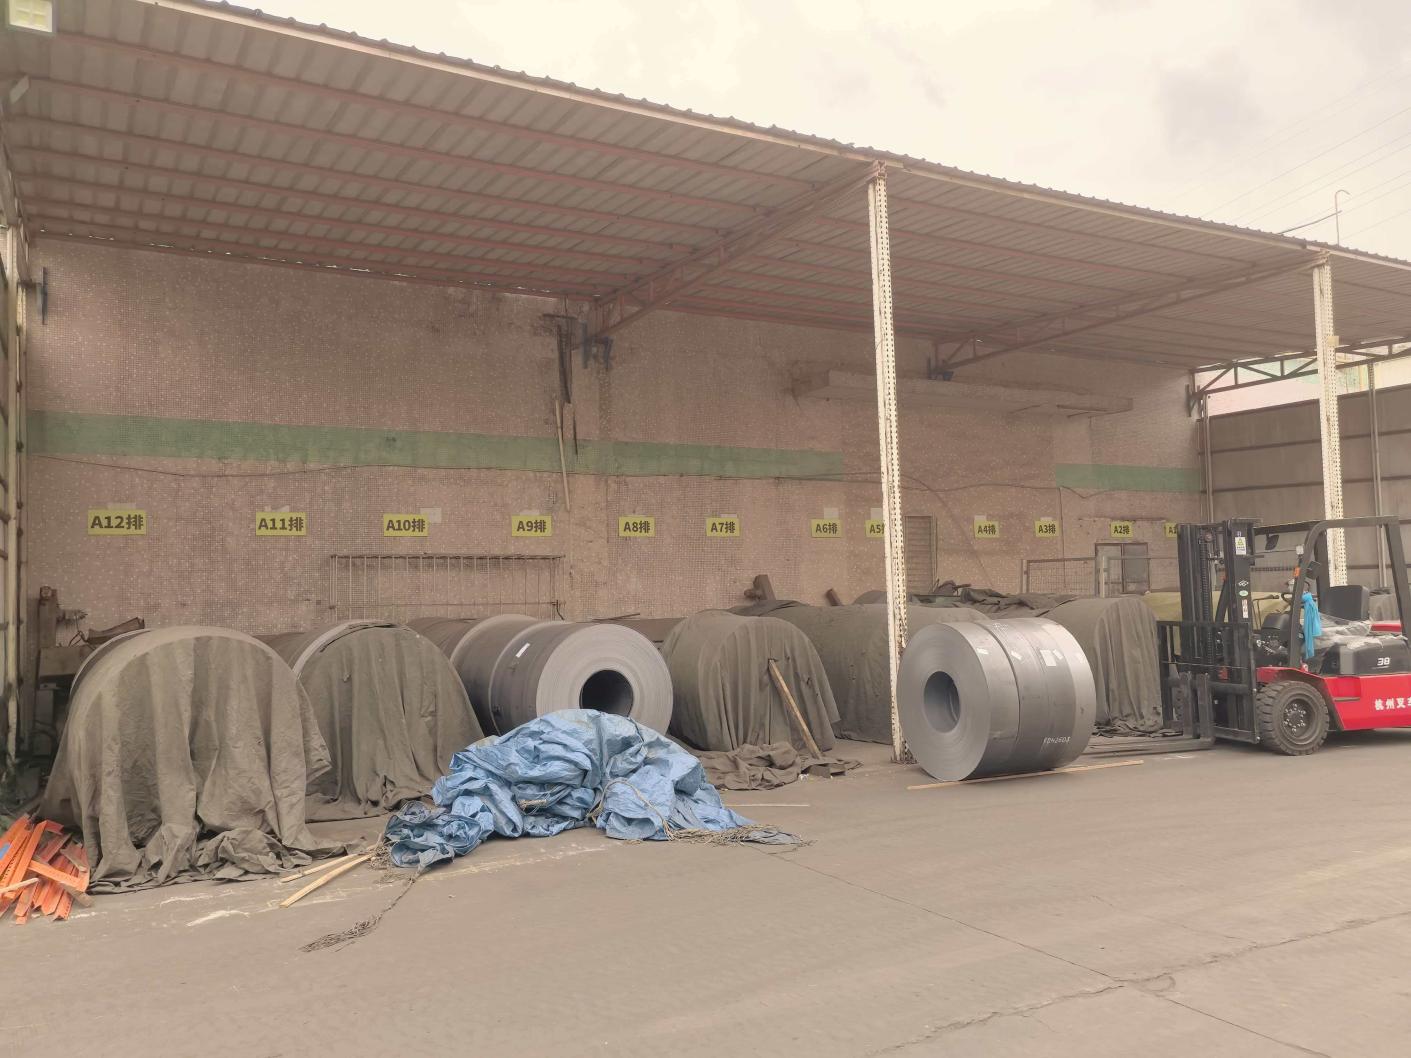
From prime Q235B/Q355B coil sourcing to automated punch-rolling, robotic MIG welding, epoxy powder coating, and final assembly, Sunli manages the entire value chain in-house. This eliminates intermediary markups and reduces project lead times by up to 35% compared to Western manufacturers.
With multi-line continuous roll-forming systems and automated 3D printing prototyping capabilities, Sunli handles ultra-large enterprise orders (over 50,000 pallet positions per project) with consistent unit-to-unit precision and rapid delivery schedules.
Located in Shenzhen, adjacent to Yantian and Shekou major deep-water ports, Sunli streamlines international freight handling, ocean container loading efficiency, and export customs clearance to North America, Europe, and Asia-Pacific destinations.
Sunli’s OEM/ODM storage machinery and automated racking systems are custom-engineered for diverse industrial sectors requiring targeted mechanical performance:
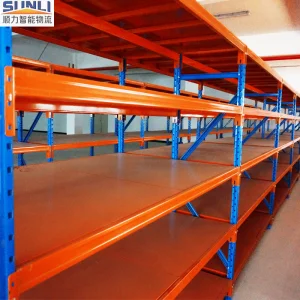
Multi-level selective platforms, high-density mezzanine flooring, and medium-duty anti-rust shelving designed for high pick frequencies, SKUs management, and fast conveyor integration.
Automated Two-Way Radio Shuttle Racks engineered for reliable operation down to -30°C, maximizing density and thermal efficiency in cold storage facilities.
Custom AGV material handling robots and ESD-protected steel shelving units preventing micro-electronic degradation during assembly and parts distribution.
Corrosion-resistant epoxy-coated rack systems featuring seamless continuous welds, smooth surface profiles, and easy-washdown hygiene compliance.
As industry 4.0 matures, the integration of physical racking structures with digital automation software (WMS/WCS) is accelerating rapidly. Key trends shaping procurement decisions include:
Transitioning from manual forklift loading to fully automated dual-direction AGVs and self-navigating shuttle carts. This reduces labor dependency and eliminates structural warehouse damage caused by operator errors.
Embedding strain sensors and vibration monitors into high-bay pallet racking uprights to continuously report load stress levels and detect impact anomalies before structural failures occur.
Adopting zero-VOC, heavy-metal-free thermosetting powder coatings applied via electro-static deposition lines, lowering operational carbon footprints while offering superior scratch resistance.
When sourcing heavy-duty racking and packaging machinery from global manufacturers, procurement managers must evaluate several technical benchmarks to guarantee safety, operational longevity, and regulatory compliance:
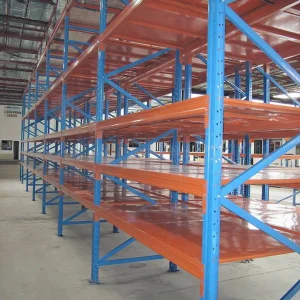
Always verify raw material certificates. Sunli utilizes premium cold-rolled Q235B and Q355B structural steel, ensuring certified tensile yield strengths capable of supporting up to 5,000 kg per beam level under static and dynamic loading.
High-quality selective pallet racking should observe a maximum beam deflection ratio of L/200 under nominal load, engineered with safety factors exceeding 1.65 in compliance with RMI and FEM specifications.
Ensure a 7-stage chemical washing and phosphating process prior to powder spraying. Coating thickness must be verified between 60 to 90 microns using digital magnetic thickness gauges to guarantee anti-corrosion protection in humid climates.
Comprehensive answers regarding OEM/ODM capability, structural engineering, export logistics, and quality assurance.
Advanced AGVs, radio shuttle solutions, and high-payload adjustable racking systems.
 SunliRack