Engineered for extreme environments, precision temperature retention facilities, and ultra-high density automated storage integration.
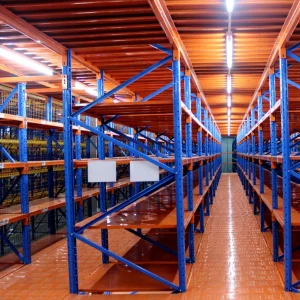
Analyzing modern temperature-controlled supply chains, pharmaceutical distribution, and perishable e-commerce growth drivers.
The global transition toward fresh food delivery, biologics, and temperature-sensitive pharmaceuticals demands ultra-reliable cold chain infrastructure. Standard warehouse racking fails under sub-zero thermal contraction; specialized cold-resistant alloy steels and anti-corrosive powder coatings are now critical industry mandates.
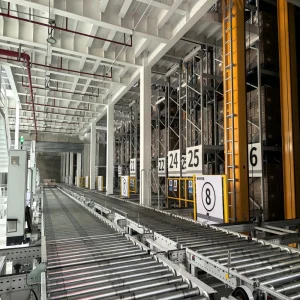
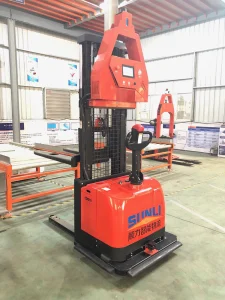
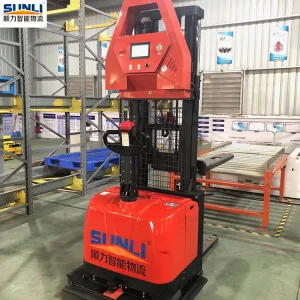
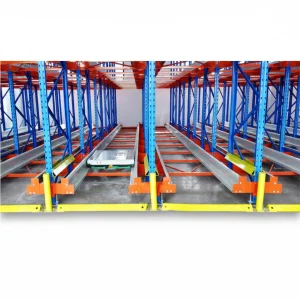
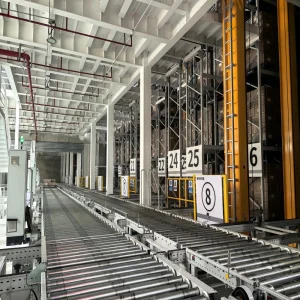
Labor shortages and skyrocketing real estate costs in urban fulfillment hubs compel operators to adopt high-density AS/RS, radio shuttle systems, and AGV/AMR autonomous forklifts, maximizing cubic meter storage utilization while minimizing thermal loss in refrigerated enclosures.
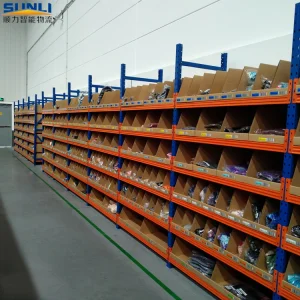
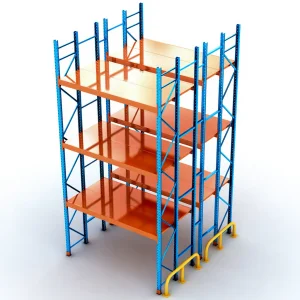
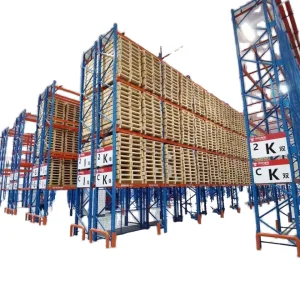
Optimizing cold chain storage layout directly translates to reduced energy consumption for refrigeration units. Efficient airflow management enabled by open-profile selective and drive-in racks prevents localized temperature hot-spots, preserving product integrity and cutting operational expenditure.
Strategic deployment paths for smart cold storage facilities across diverse global regulatory environments.
Tailoring seismic-resistant steel structures for North American and Japanese seismic zones, combined with tropical humidity-proof zinc-nickel coatings for Southeast Asian coastal distribution centers.
Future-proofing warehouses with embedded structural strain sensors, wireless telemetry tracking rack fatigue under sub-zero temperatures, and real-time inventory synchronization through cloud-based WMS platforms.
Designing structures compatible with rooftop solar arrays and energy-efficient LED warehouse lighting grids, supporting corporate net-zero sustainability goals without compromising load-bearing performance.
How integrated industrial clusters deliver unmatched cost efficiency, rapid prototyping, and supreme structural quality.
Direct access to premium Q235 and Q355 cold-rolled steel mills within a 100km radius enables Shenzhen Sunli to maintain strict cost control, eliminate supply bottlenecks, and guarantee raw material traceability for every project batch.
With an in-house team of 28 R&D engineers and automated rolling/welding lines, custom dimensional designs and non-standard load ratings are prototyped and verified within 7 business days.
Our dedicated 35-member QC taskforce executes destructive load testing, weld seam ultrasonic inspections, and electrostatic coating thickness checks conforming strictly to international CE and ISO9001 standards.
Established in 2015, operating from a 38,000 m² advanced manufacturing facility with over 12 years of industry mastery.
Shenzhen Sunli Intelligent Logistics Equipment Co., Ltd.
Established in 2015, Shenzhen Sunli Intelligent Logistics Equipment Co., Ltd. is a leading manufacturer specializing in heavy-duty industrial racking and smart warehouse storage solutions. Operating from a modern production facility spanning 38,000 m², we leverage over 12 years of industry experience and 8 years of international trade expertise to serve global logistics and industrial sectors. Our high-performance storage solutions generate an annual export revenue ranging between $18 million and $25 million, with core markets spanning North America, Western Europe, Southeast Asia, and the Middle East.
Quality and precision are central to our operations. Our dynamic team of 35 dedicated QC professionals implements rigorous product inspection methods, including full raw material load-bearing analysis, high-precision weld seam testing, and comprehensive anti-corrosion powder-coating thickness checks. Driven by strong R&D capabilities, our team of 28 skilled R&D engineers continuously innovates to meet evolving supply chain requirements, introducing over 120 new products and structural improvements annually.
We offer extensive OEM/ODM custom options, including tailored load capacities, custom rack dimensions, color powder coatings, and fully integrated automated shuttle systems (AS/RS). Backed by a strong network of over 800 supply chain partners, we primarily partner with large-scale 3PL providers, industrial distributors, ecommerce logistics hubs, and global retail enterprises to deliver reliable, efficient, and scalable storage infrastructure worldwide.
Visual overview of our state-of-the-art automated machinery, precision rolling lines, and strict laboratory testing apparatus.
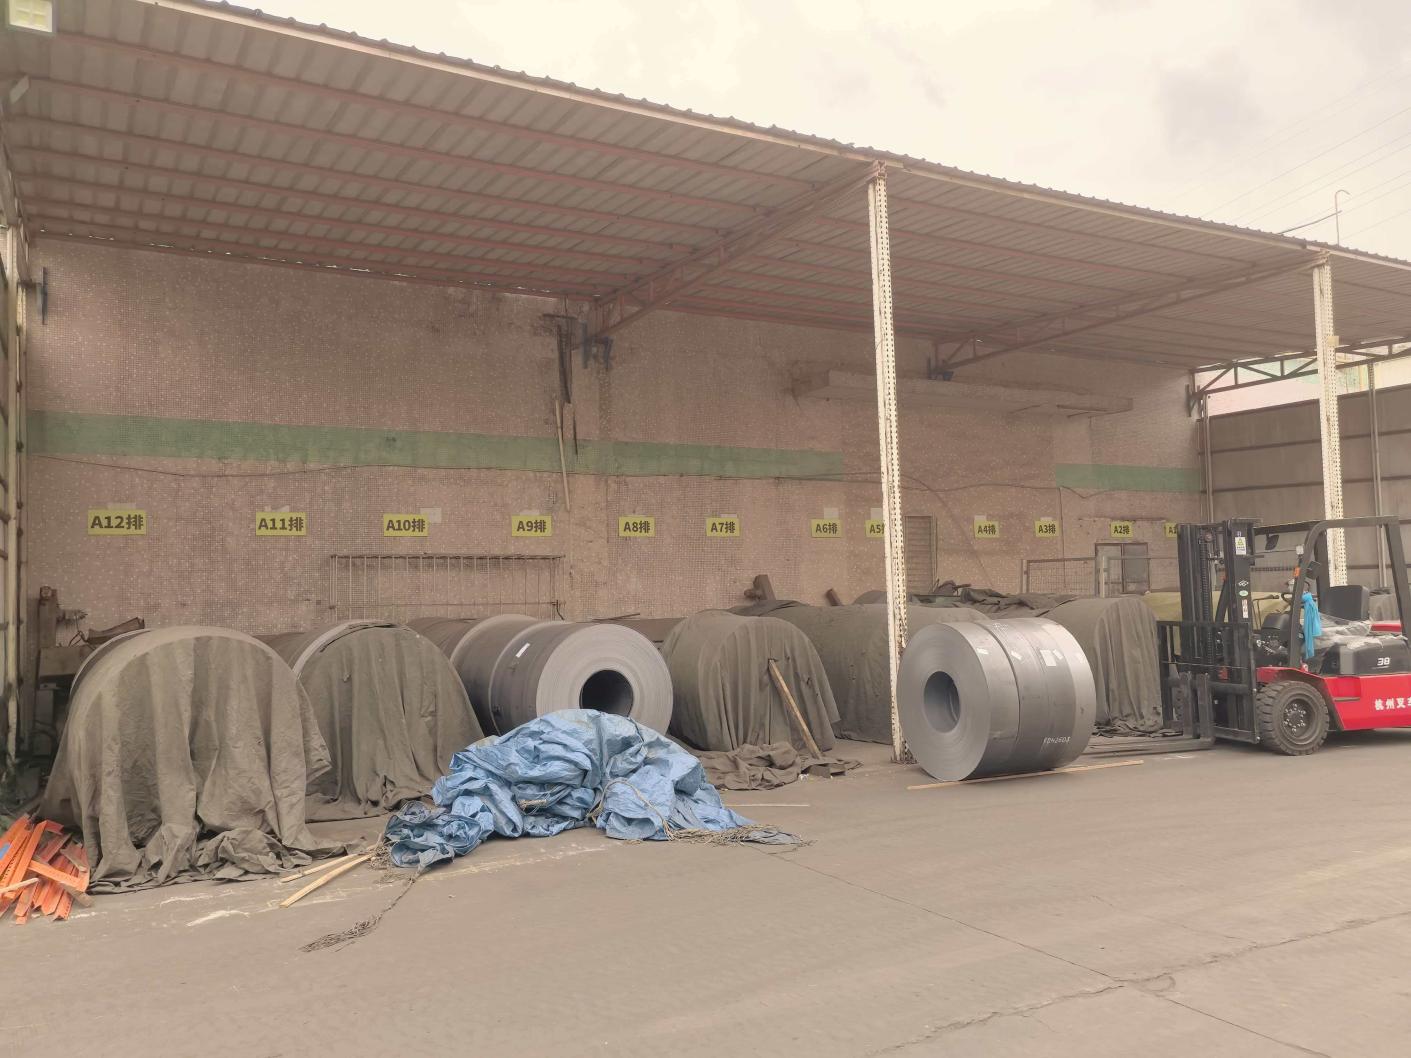 Raw Material
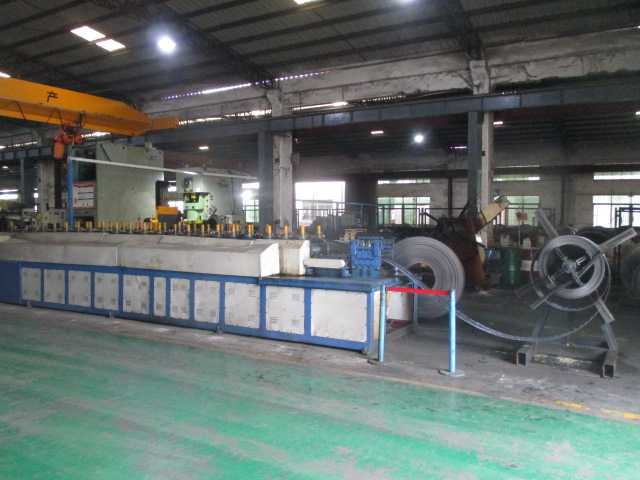 Rolling Line
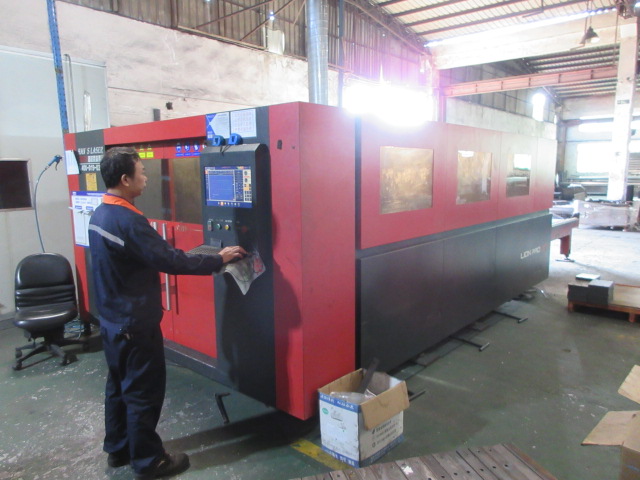 Cutting
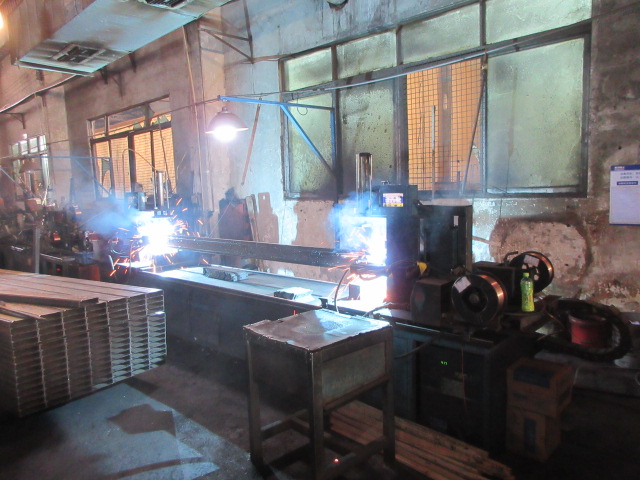 Automatic Welding
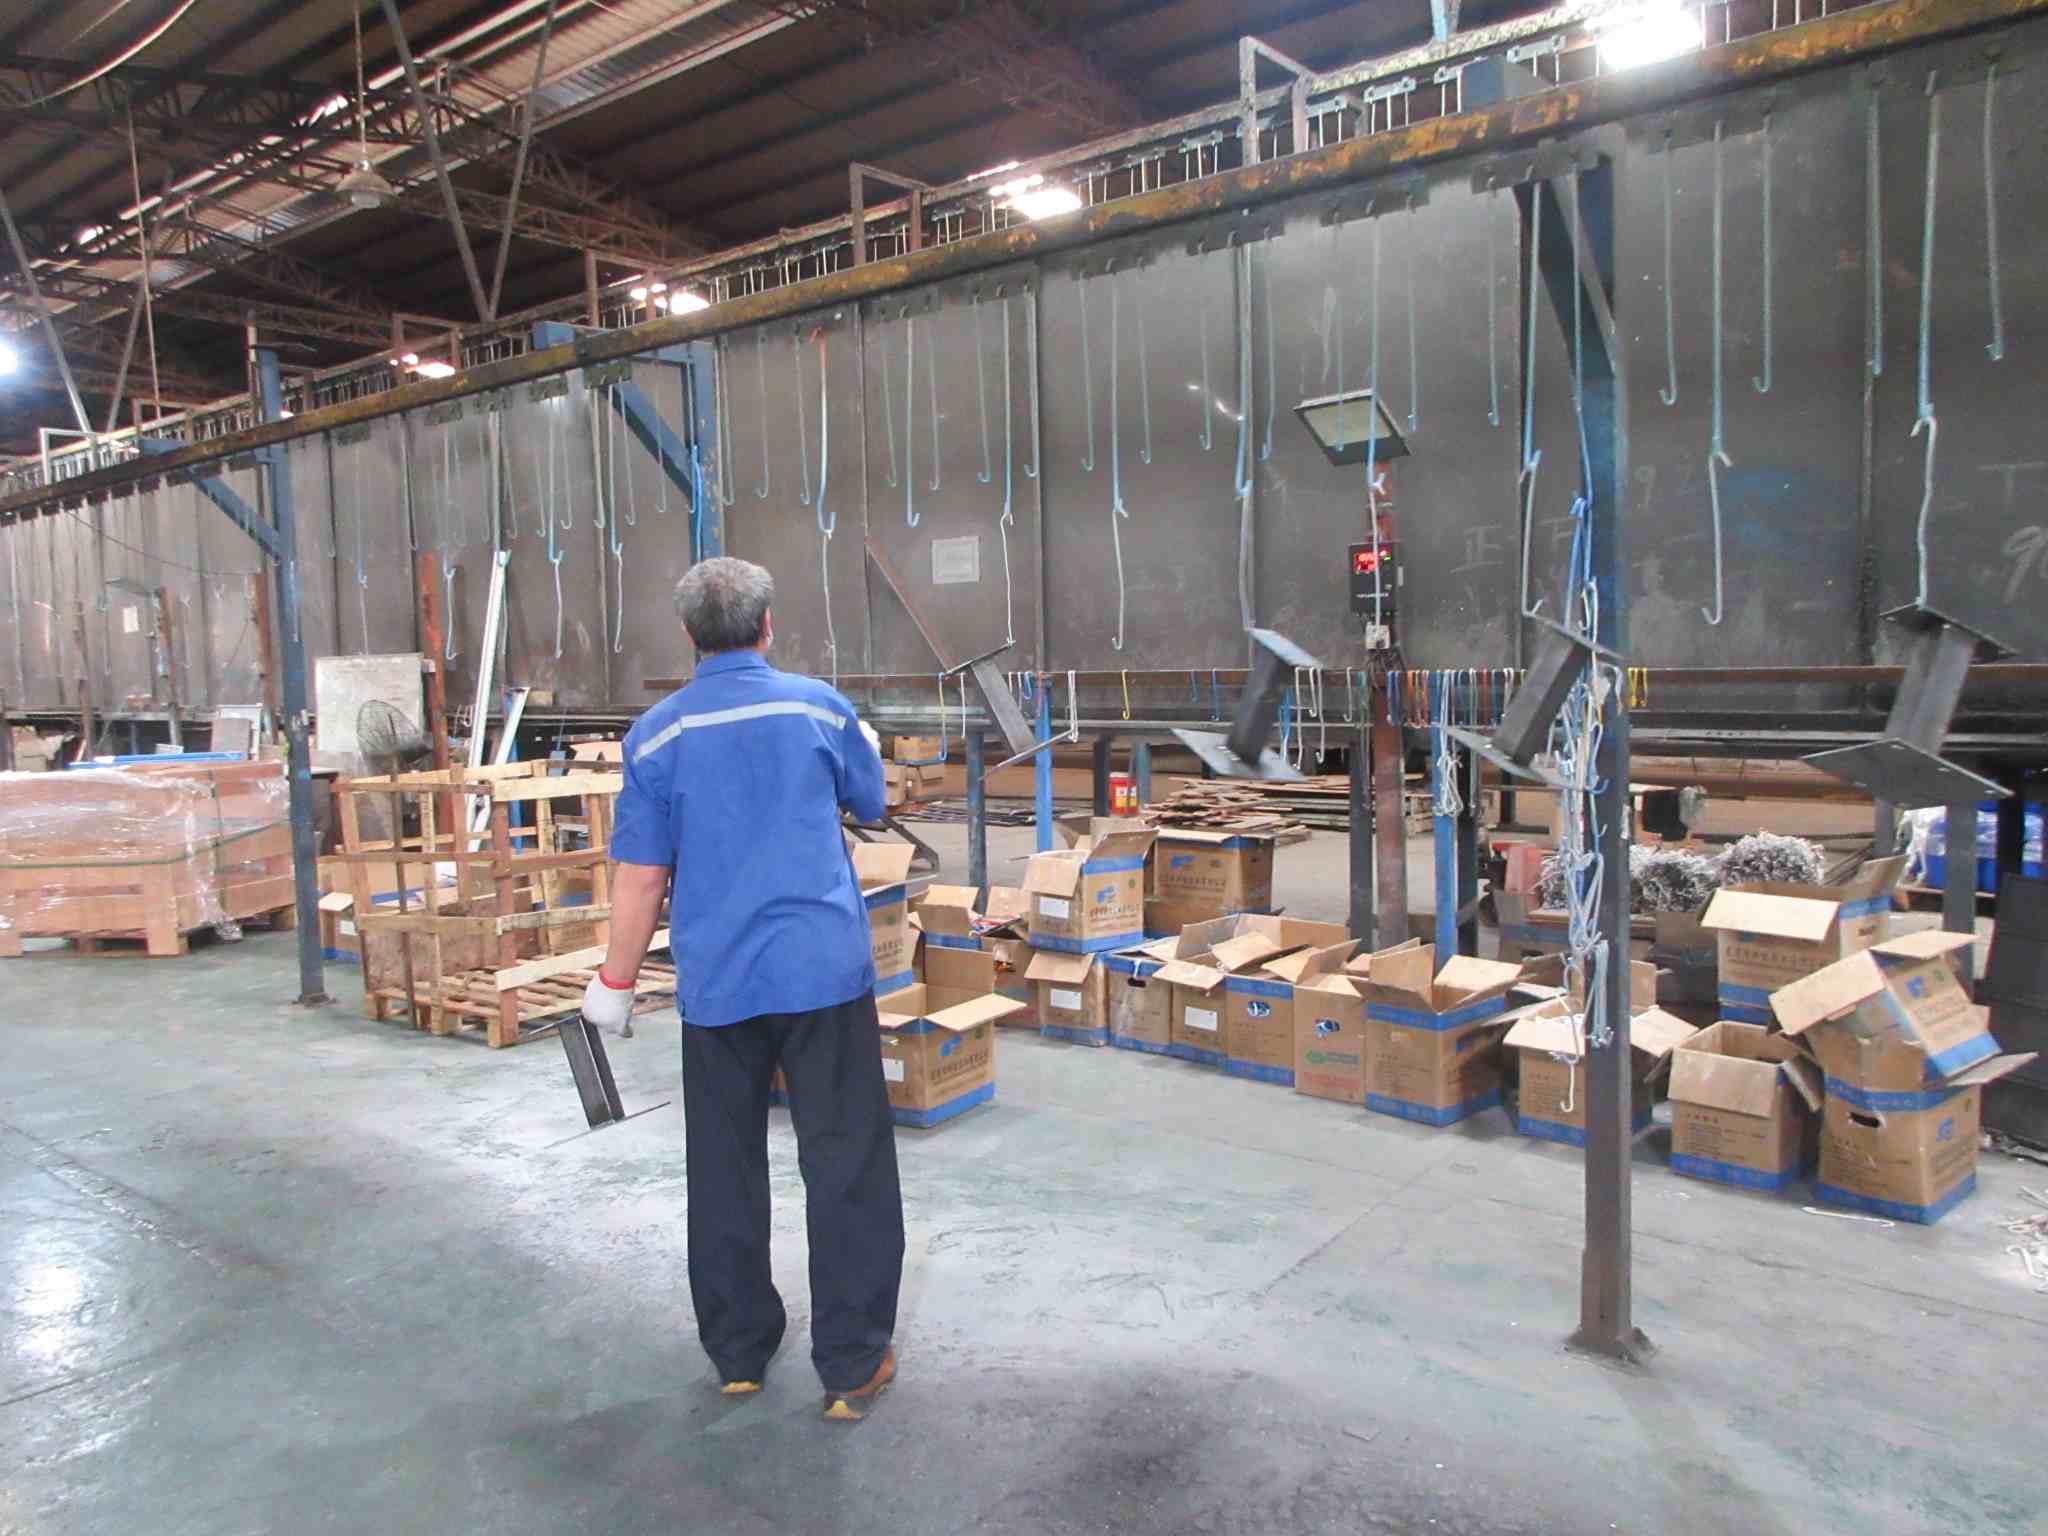 Spray Coating Line
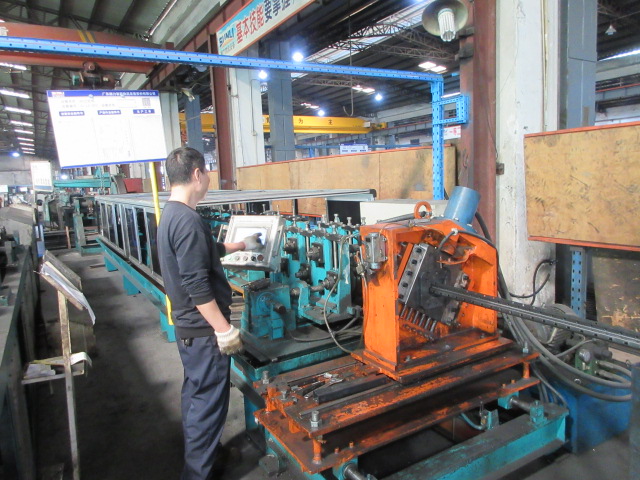 Molding
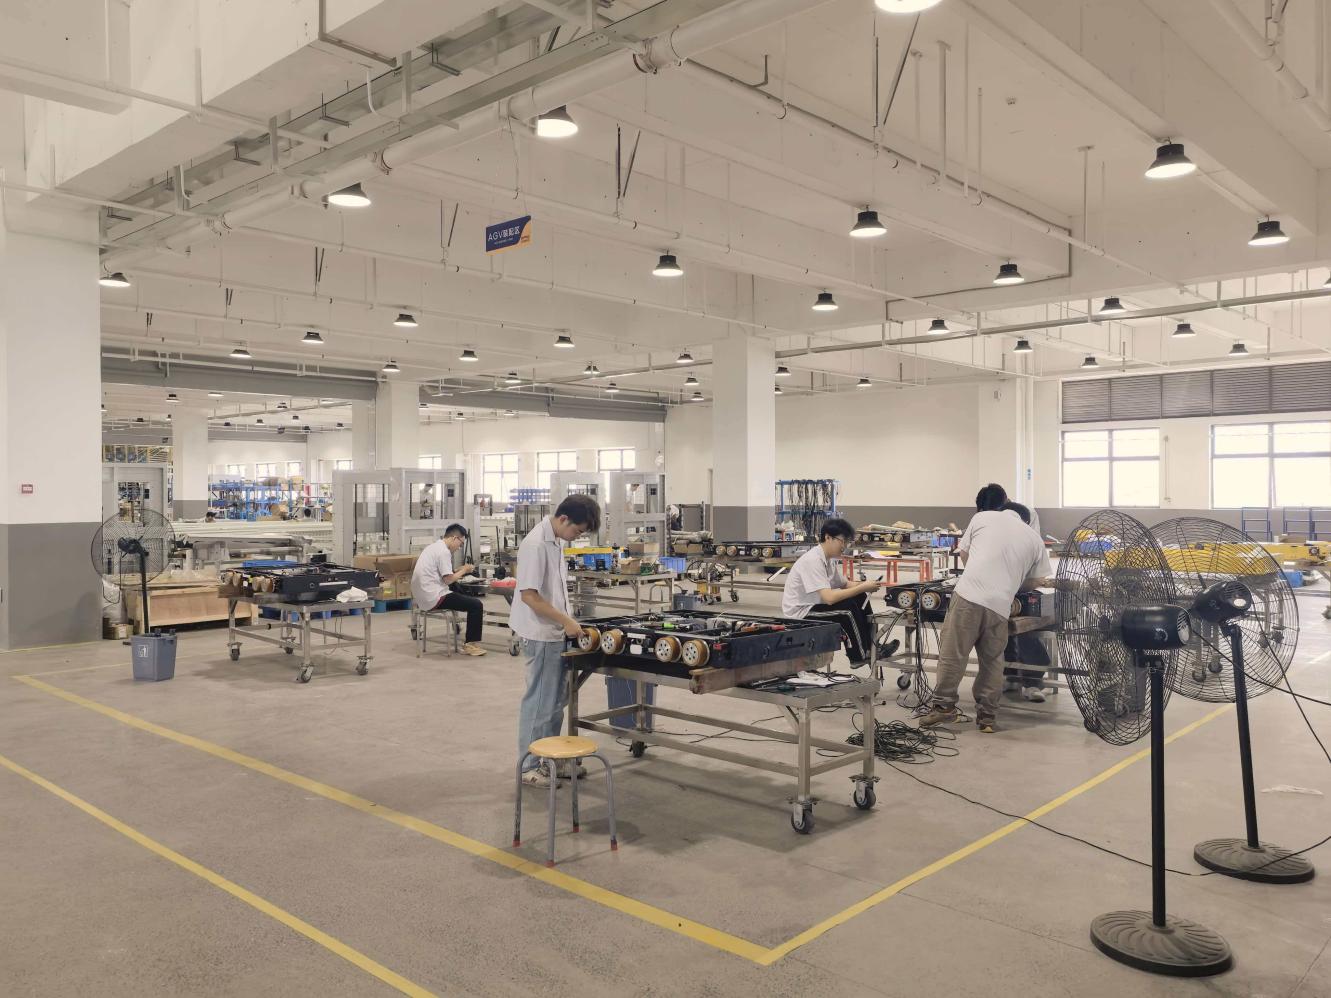 Assembly
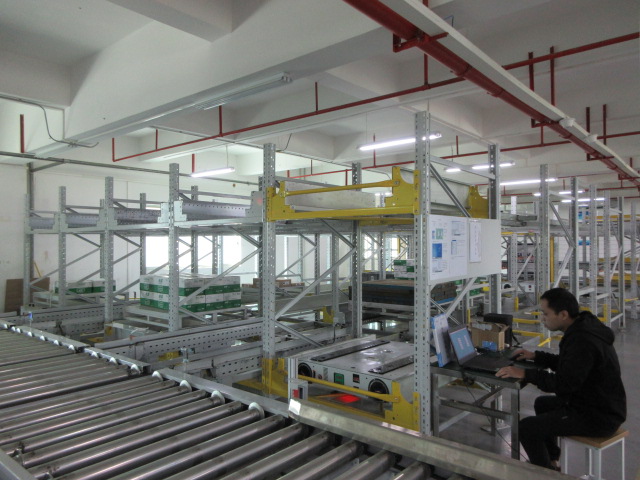 Testing
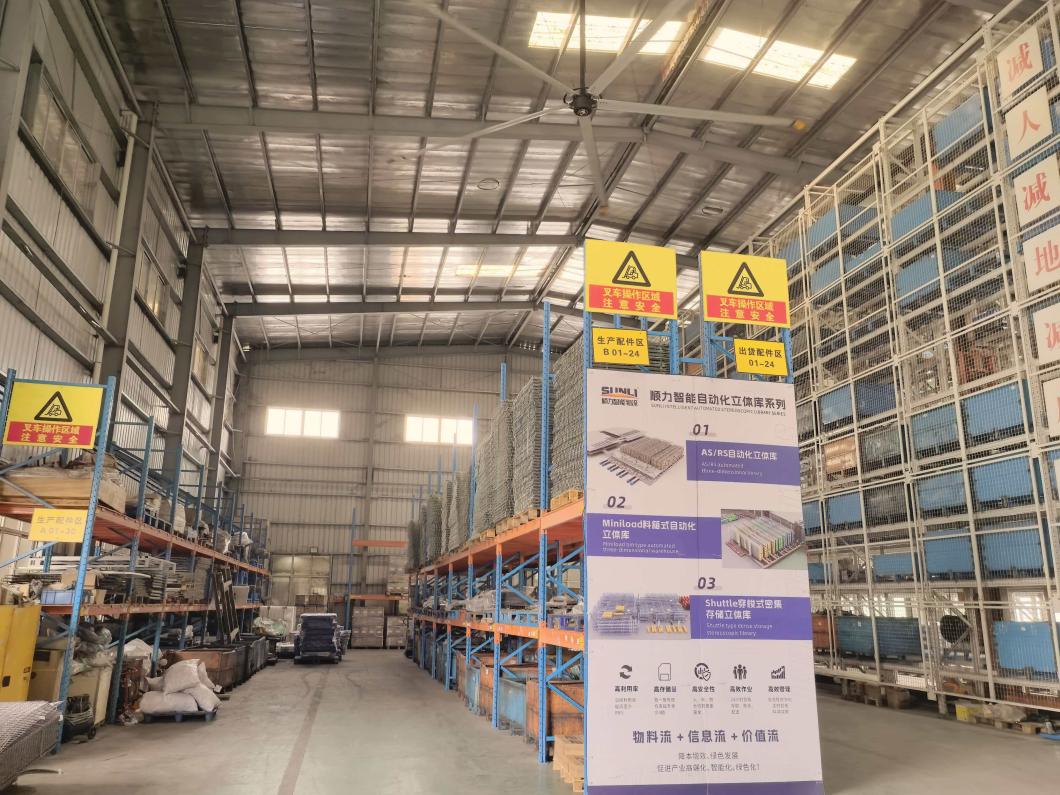 Storage
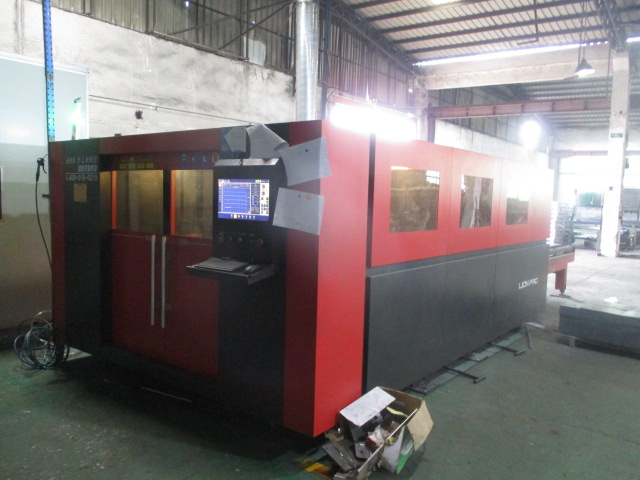 Cutting Machine
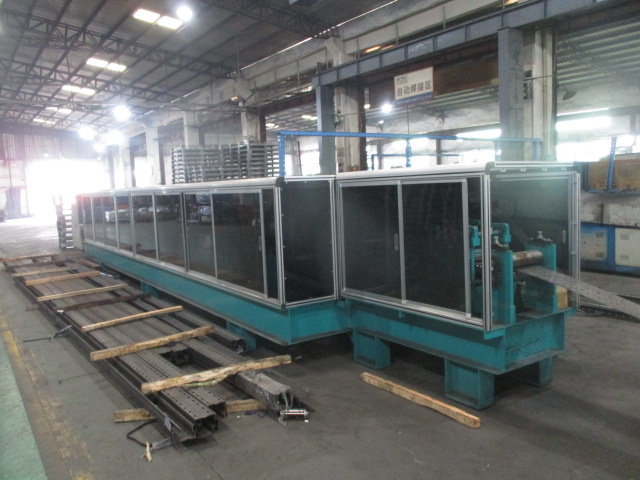 Neutralupright Rolling Line
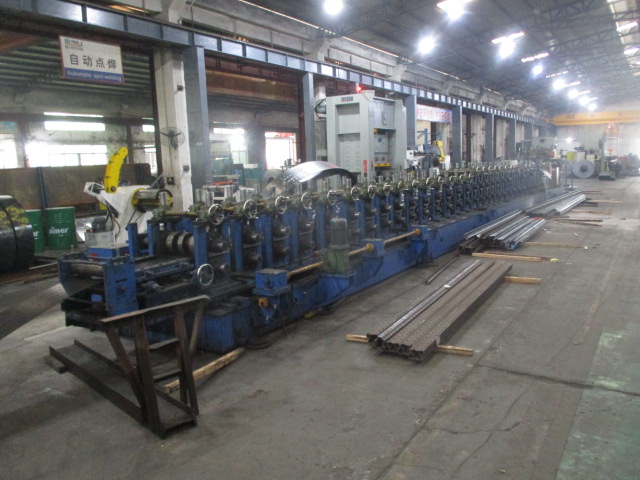 Medium-duty Upright Rolling Line
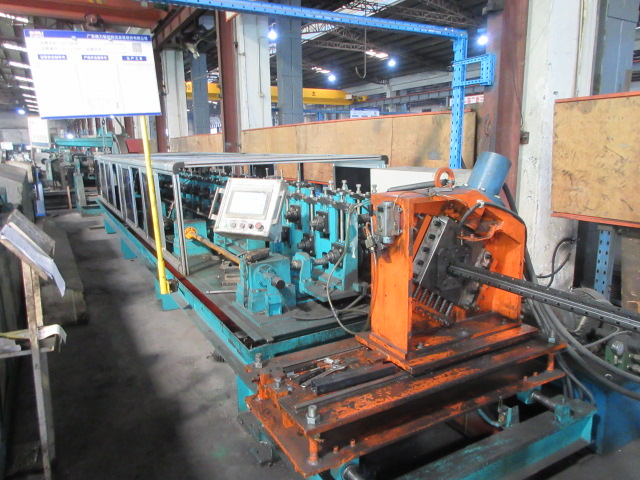 Light-duty Upright Rolling Line
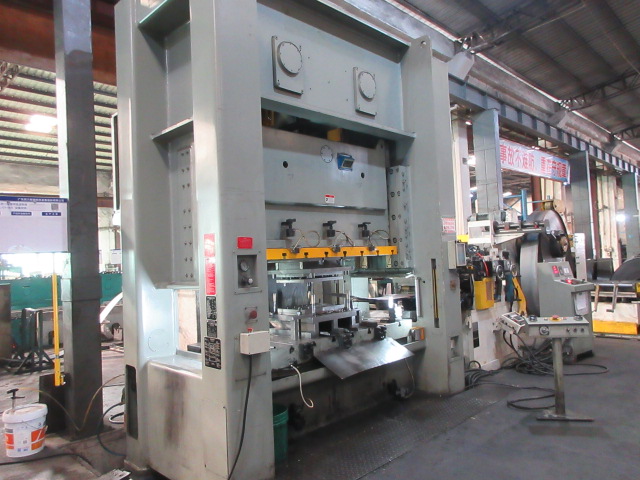 Puncher Machine
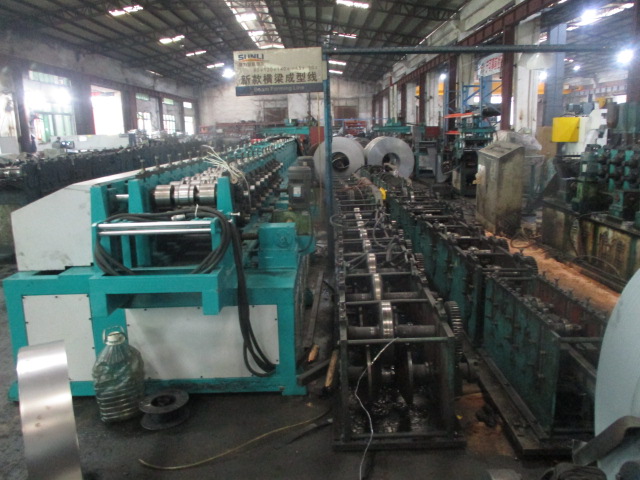 Beam Forming Line
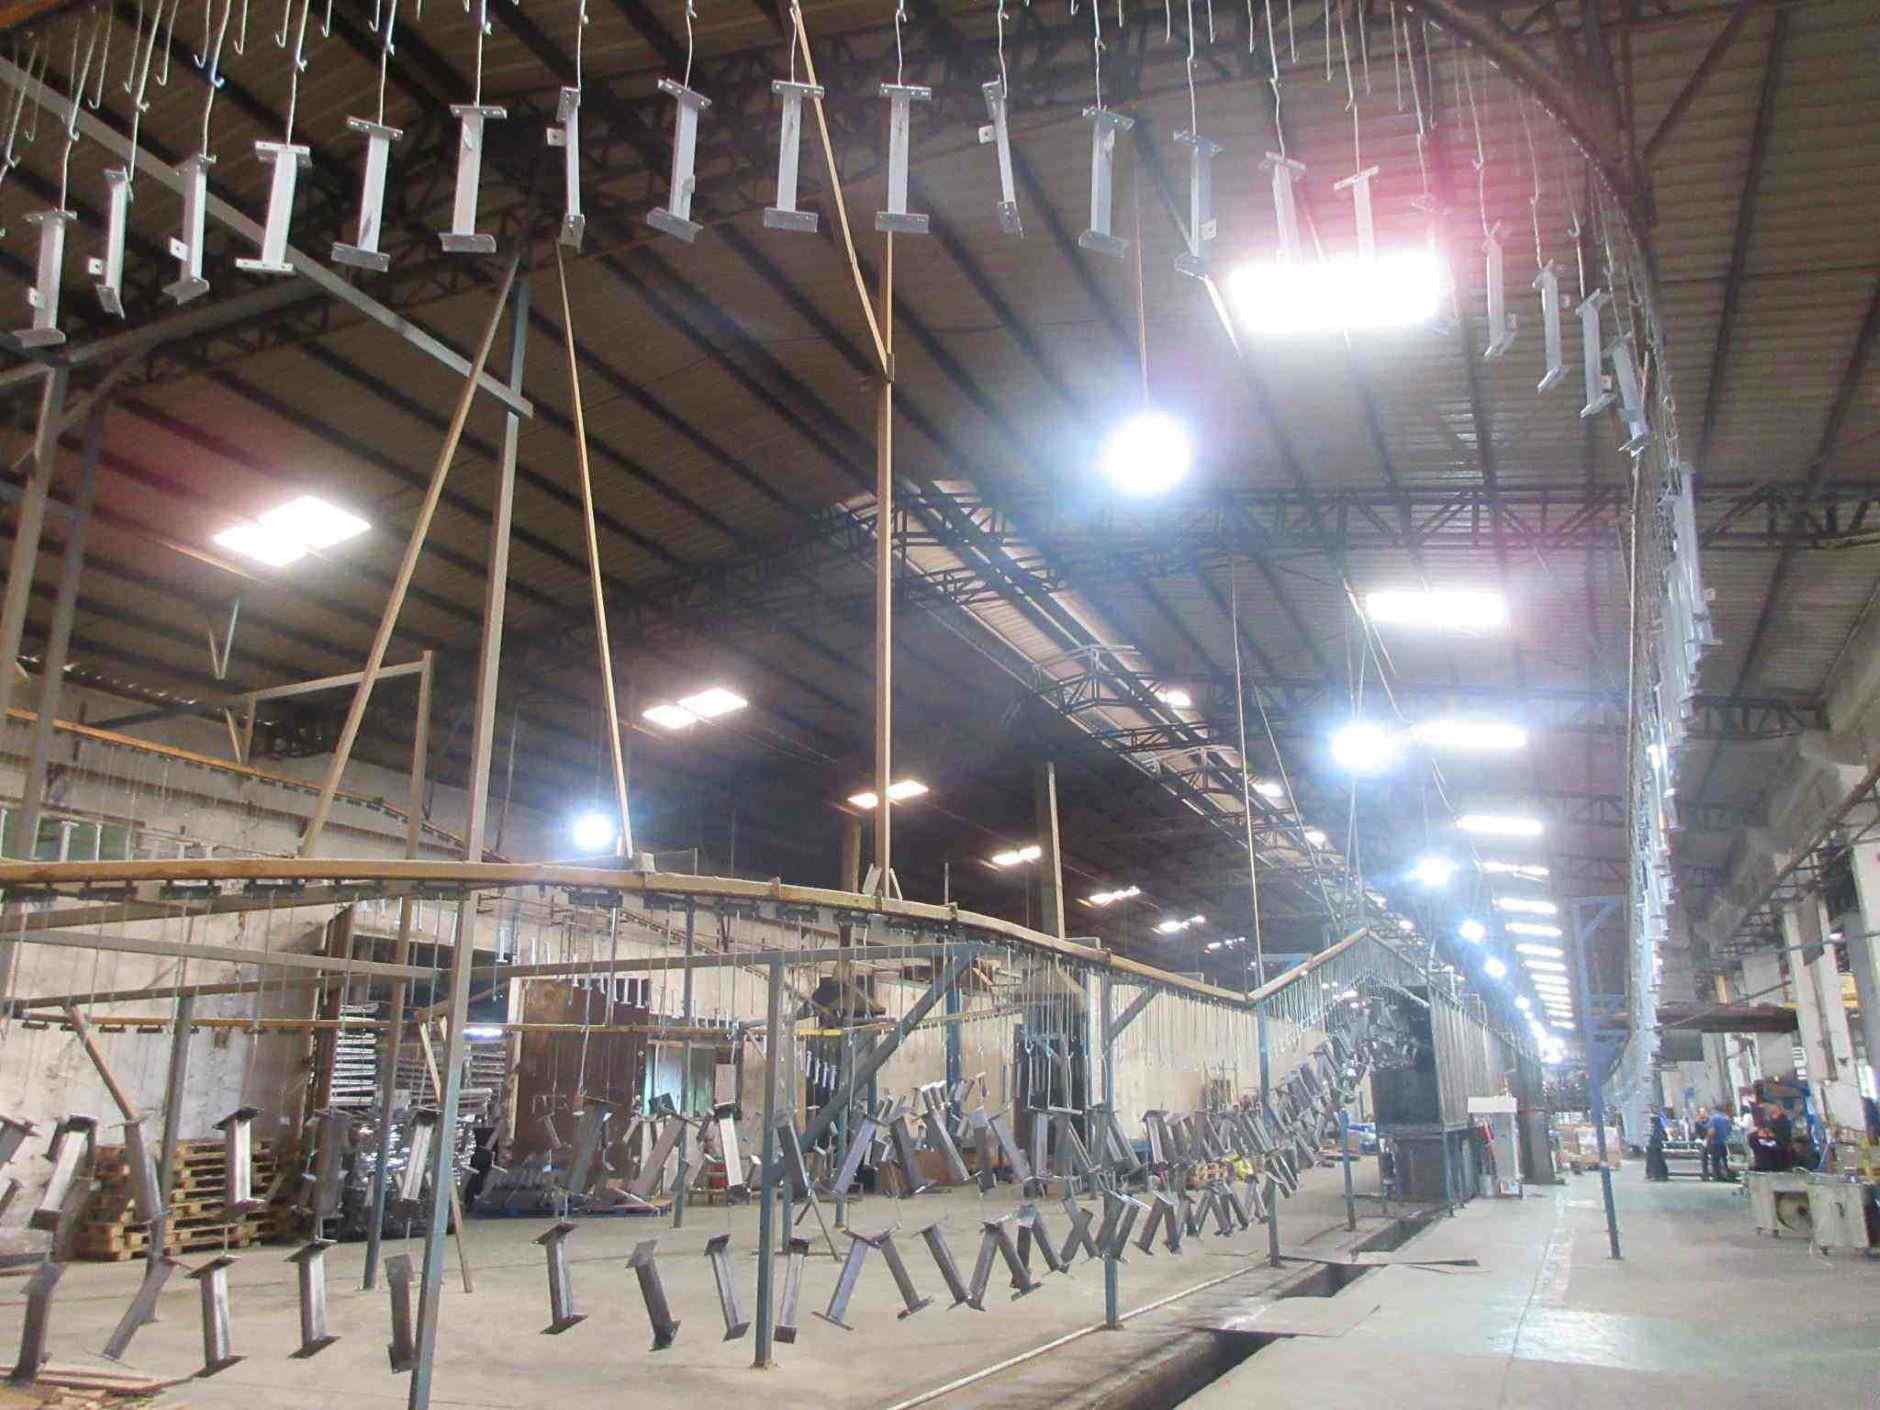 Spray Coating Line
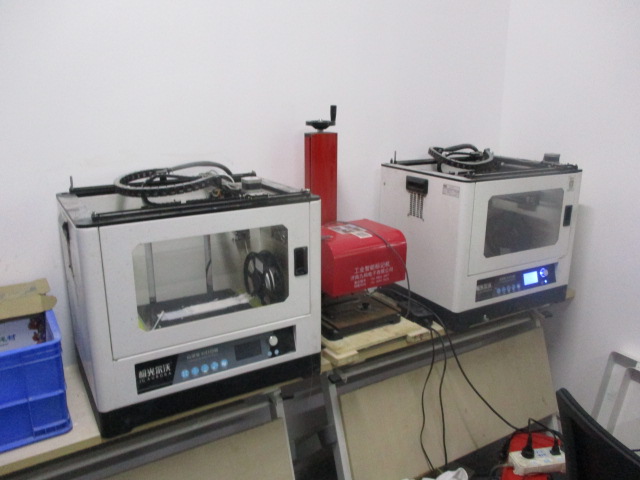 3D Printer
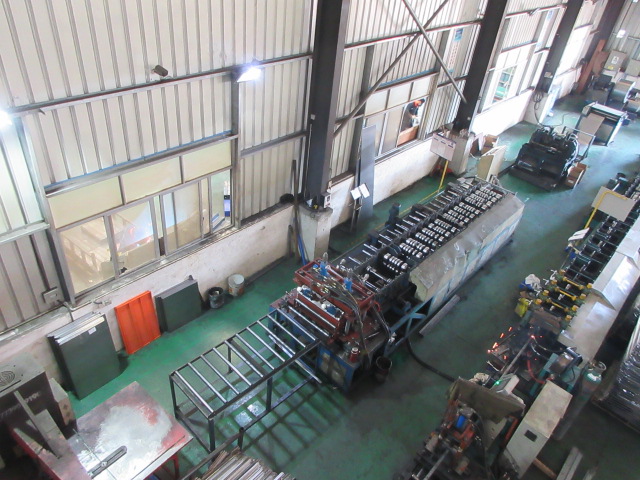 Steel Laminate Machine
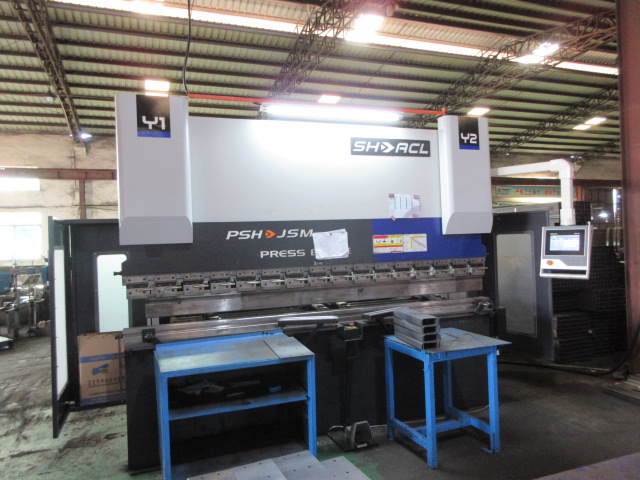 Press Brake Machine
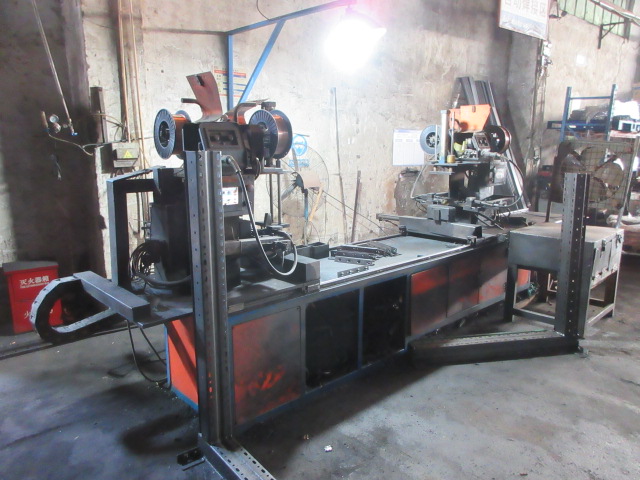 Automatic Welding Machine
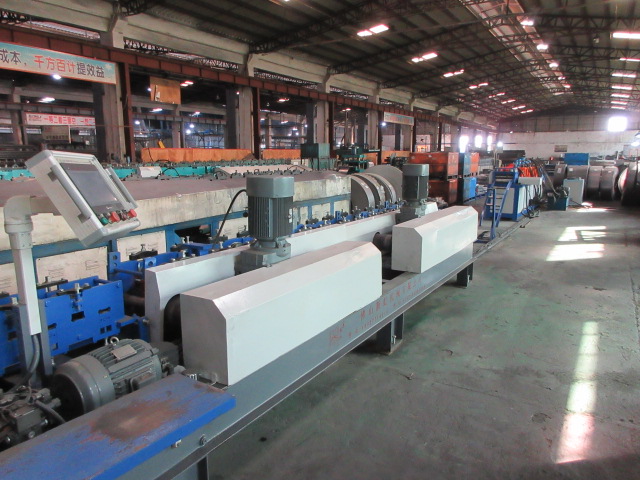 Multi Crossing Beam Line
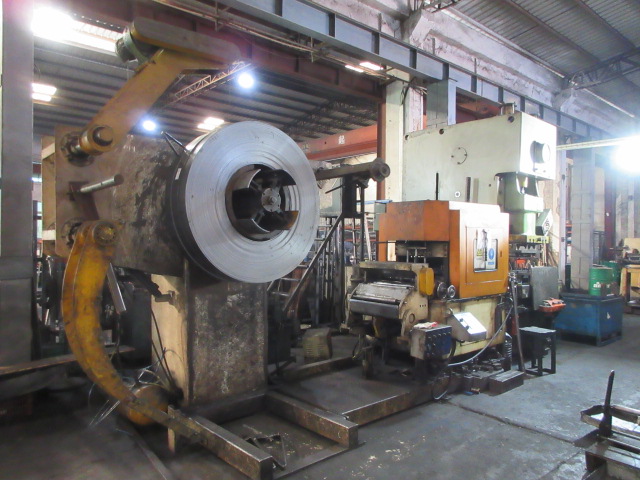 Punching Press Machine
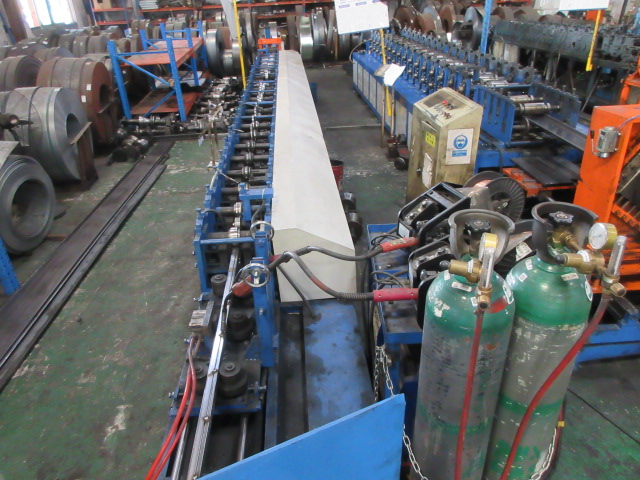 Stepped Beam Line
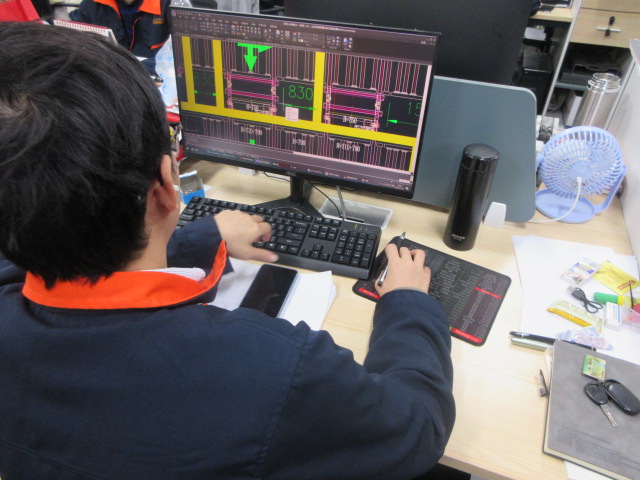 Drawing
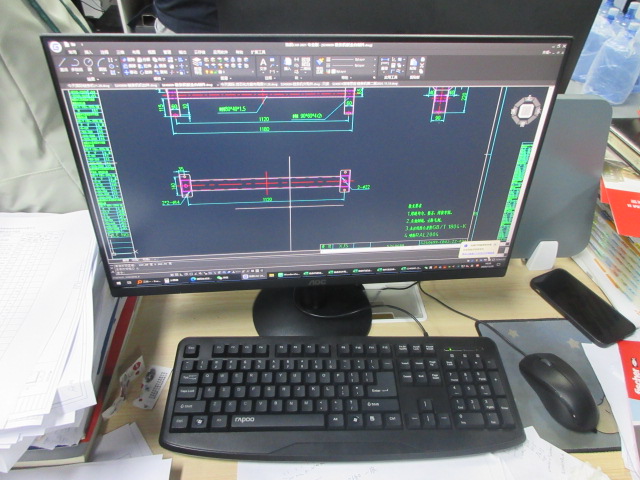 Computer
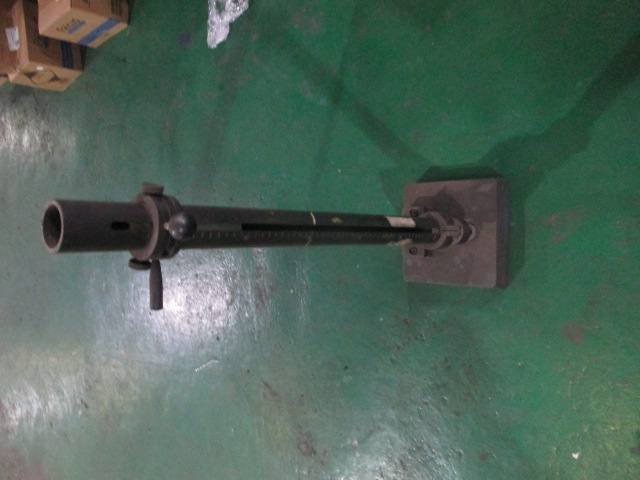 Impact Tester
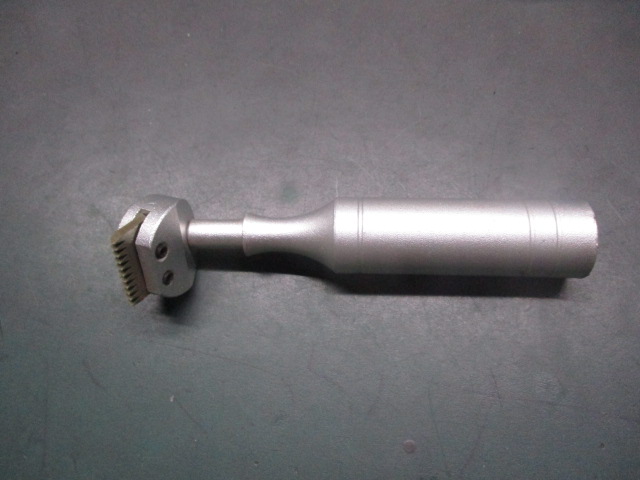 Cross-cut Tester
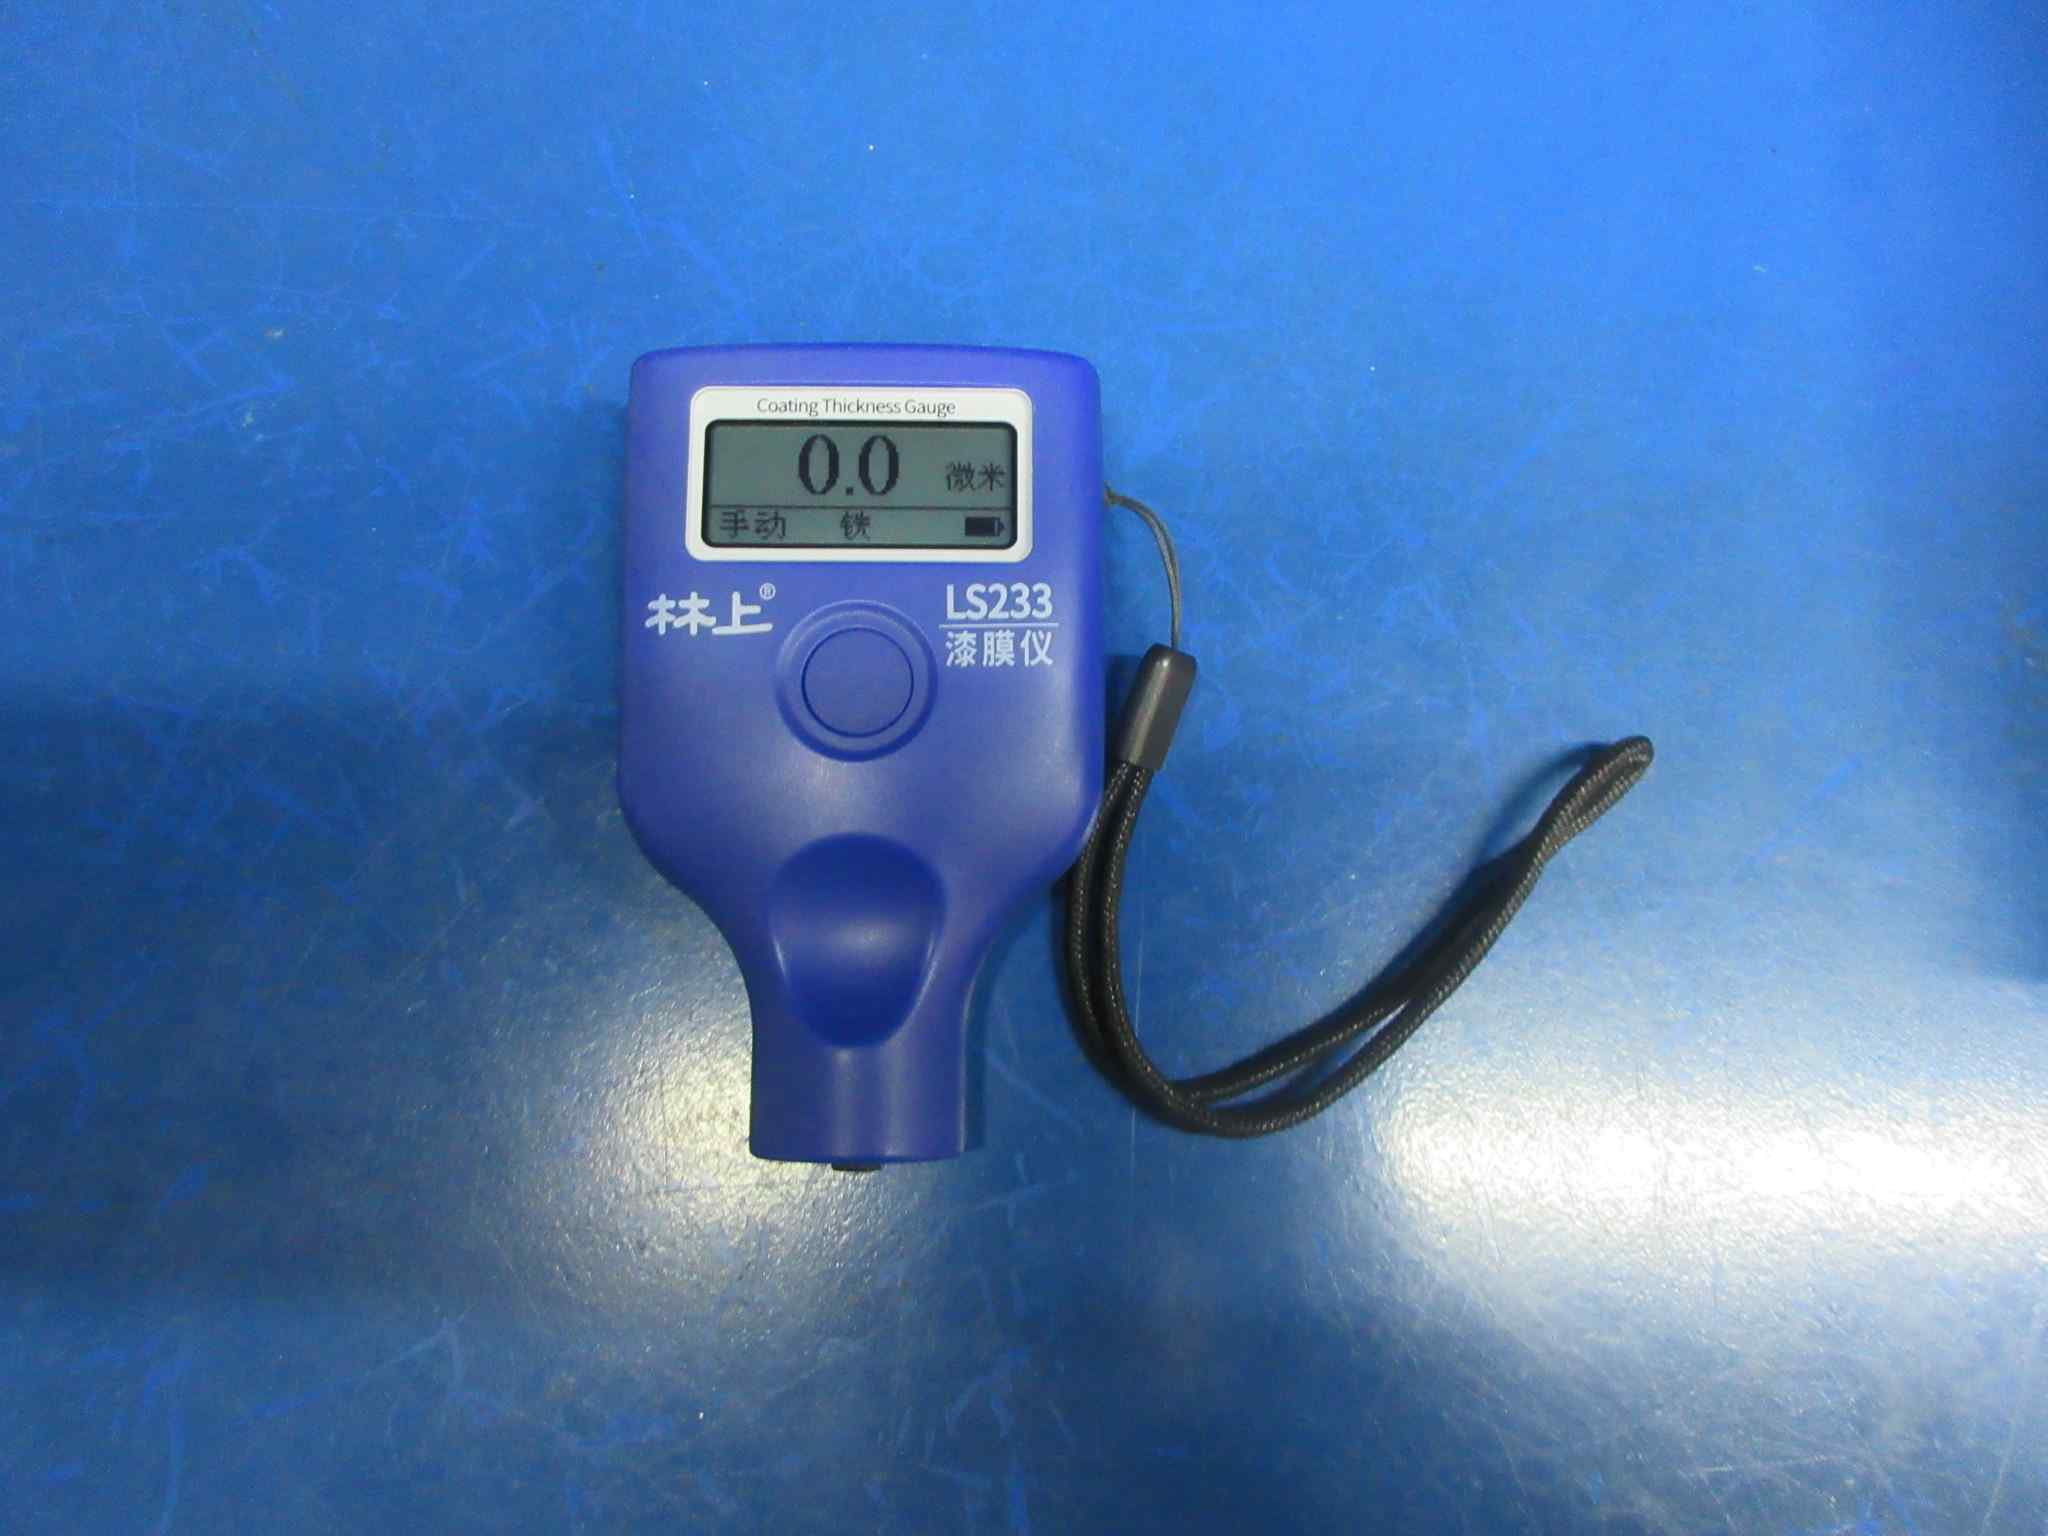 Coating Thickness Tester
 Metal Tape
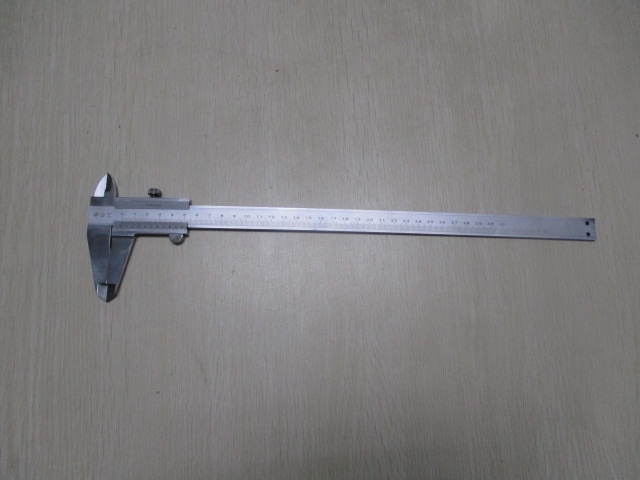 Micrometer
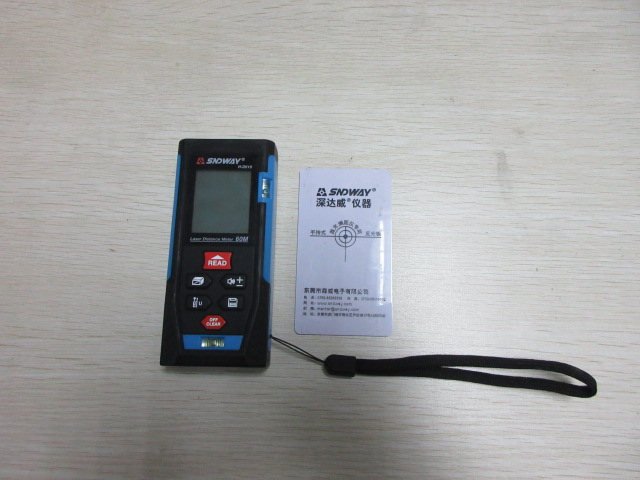 Laser Ruler
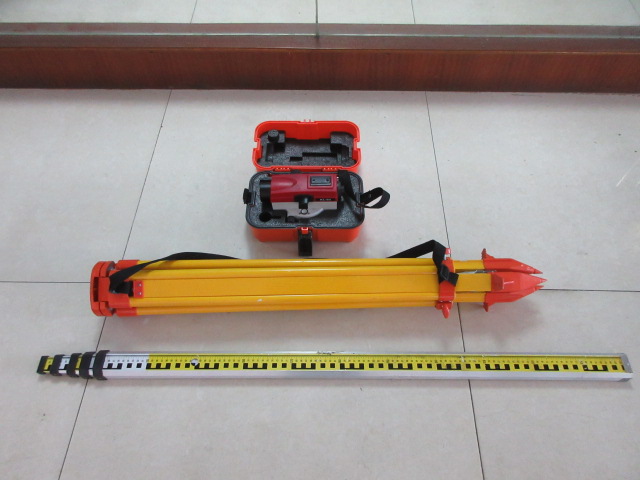 Level Instrument
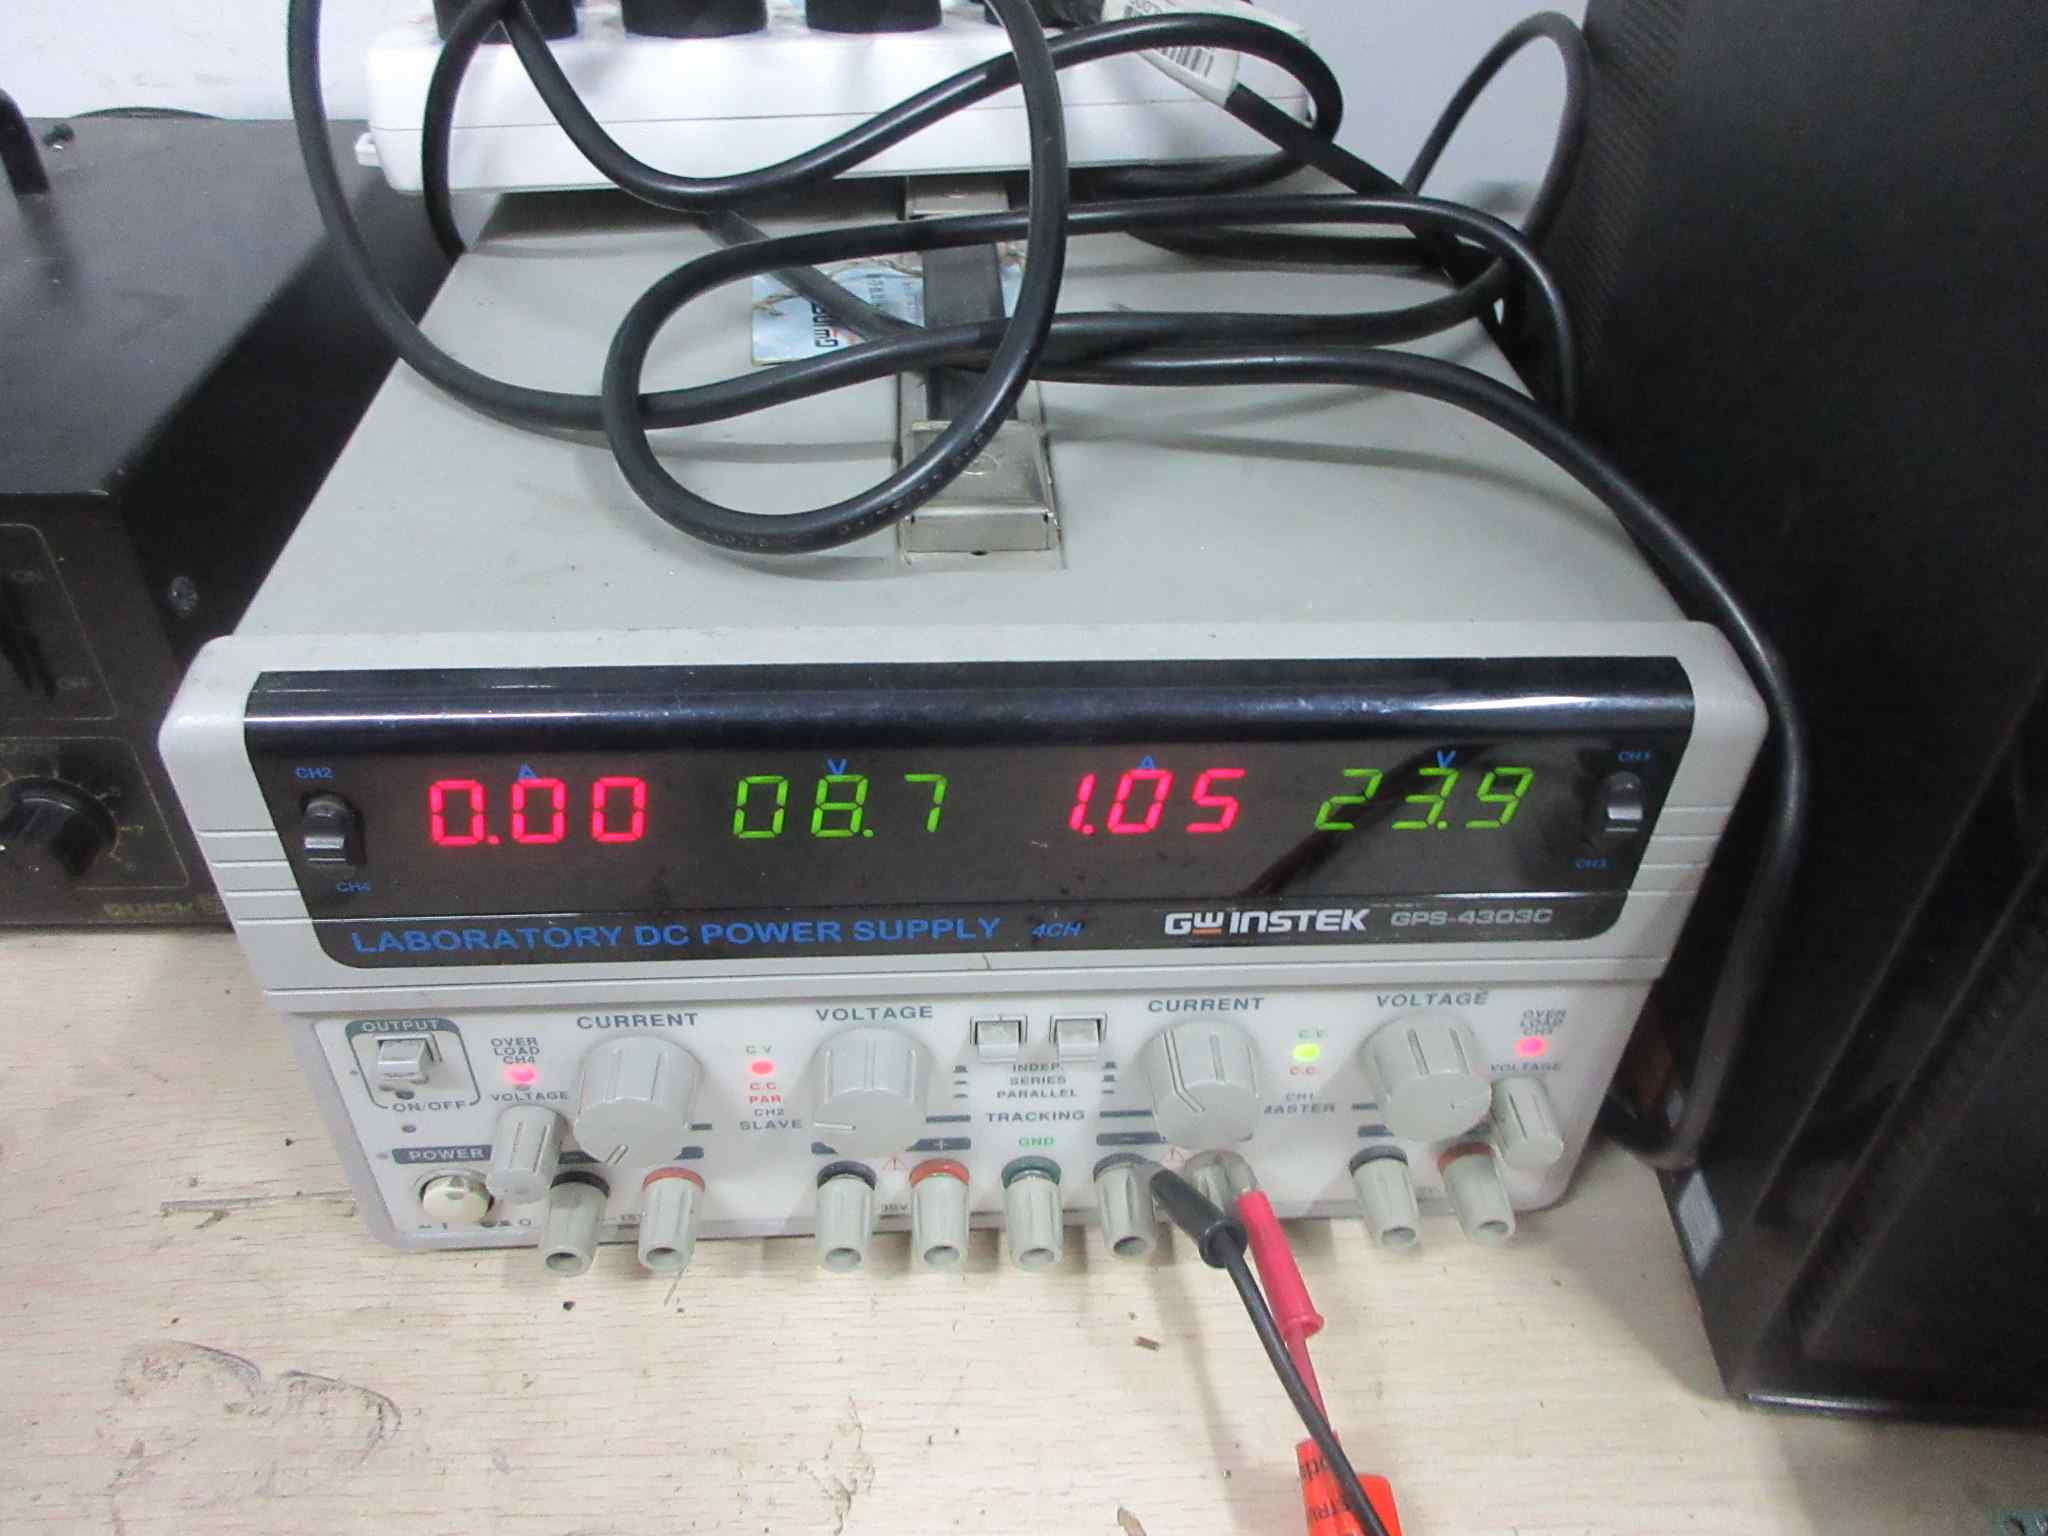 Laboratory DC Power Supply
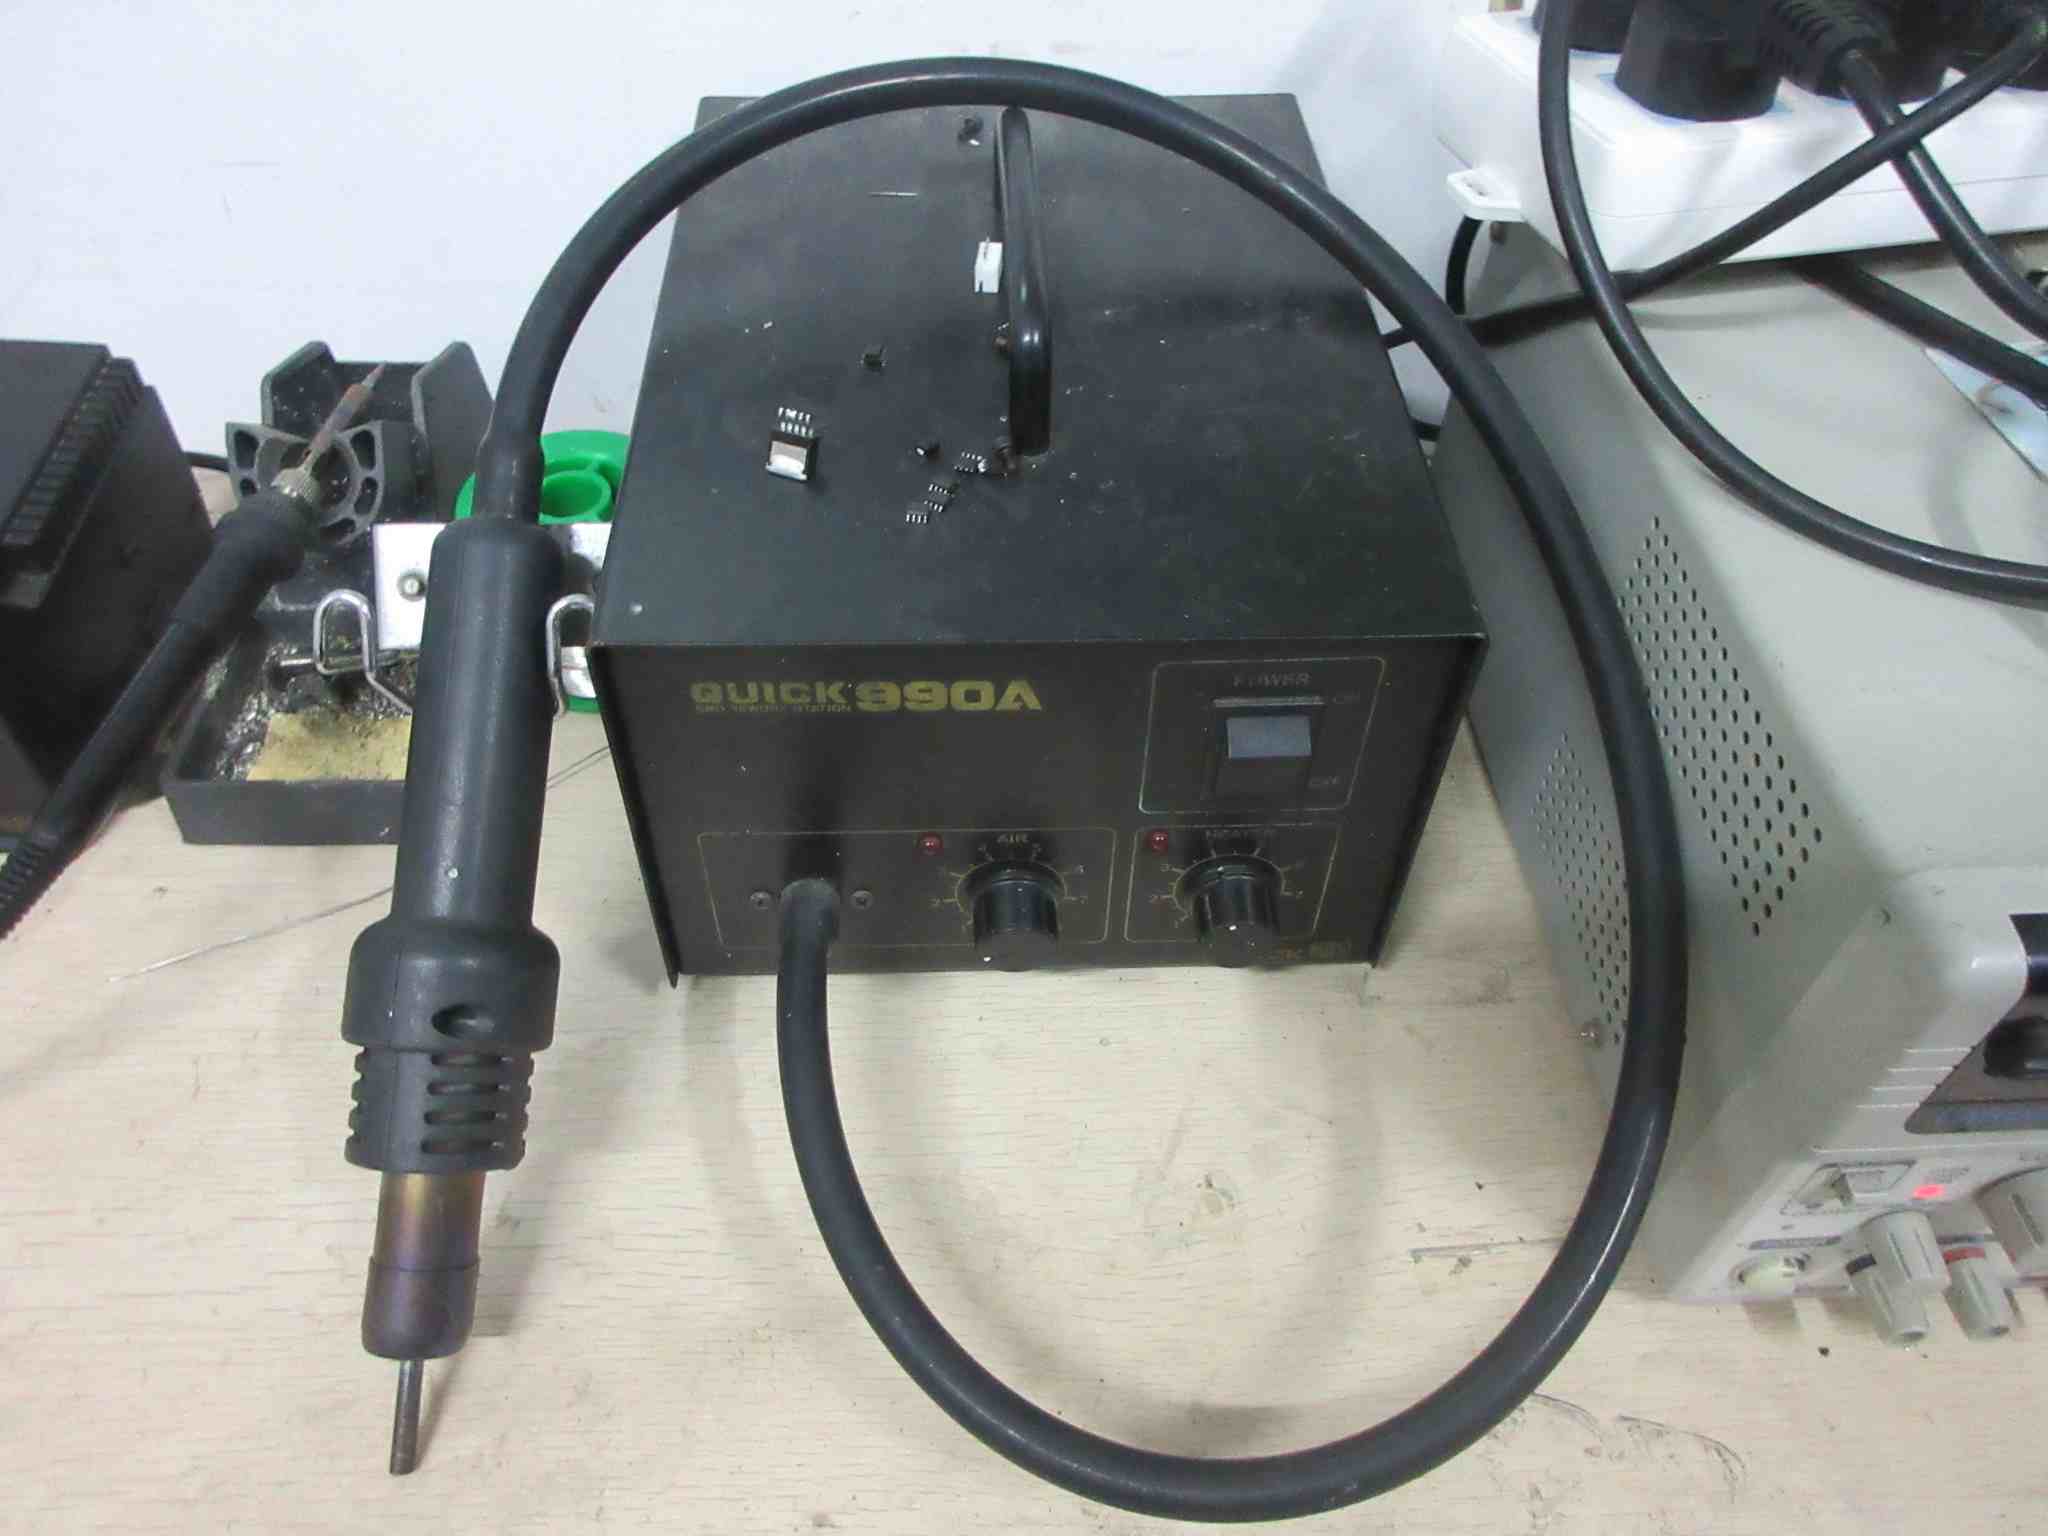 Heat Fun
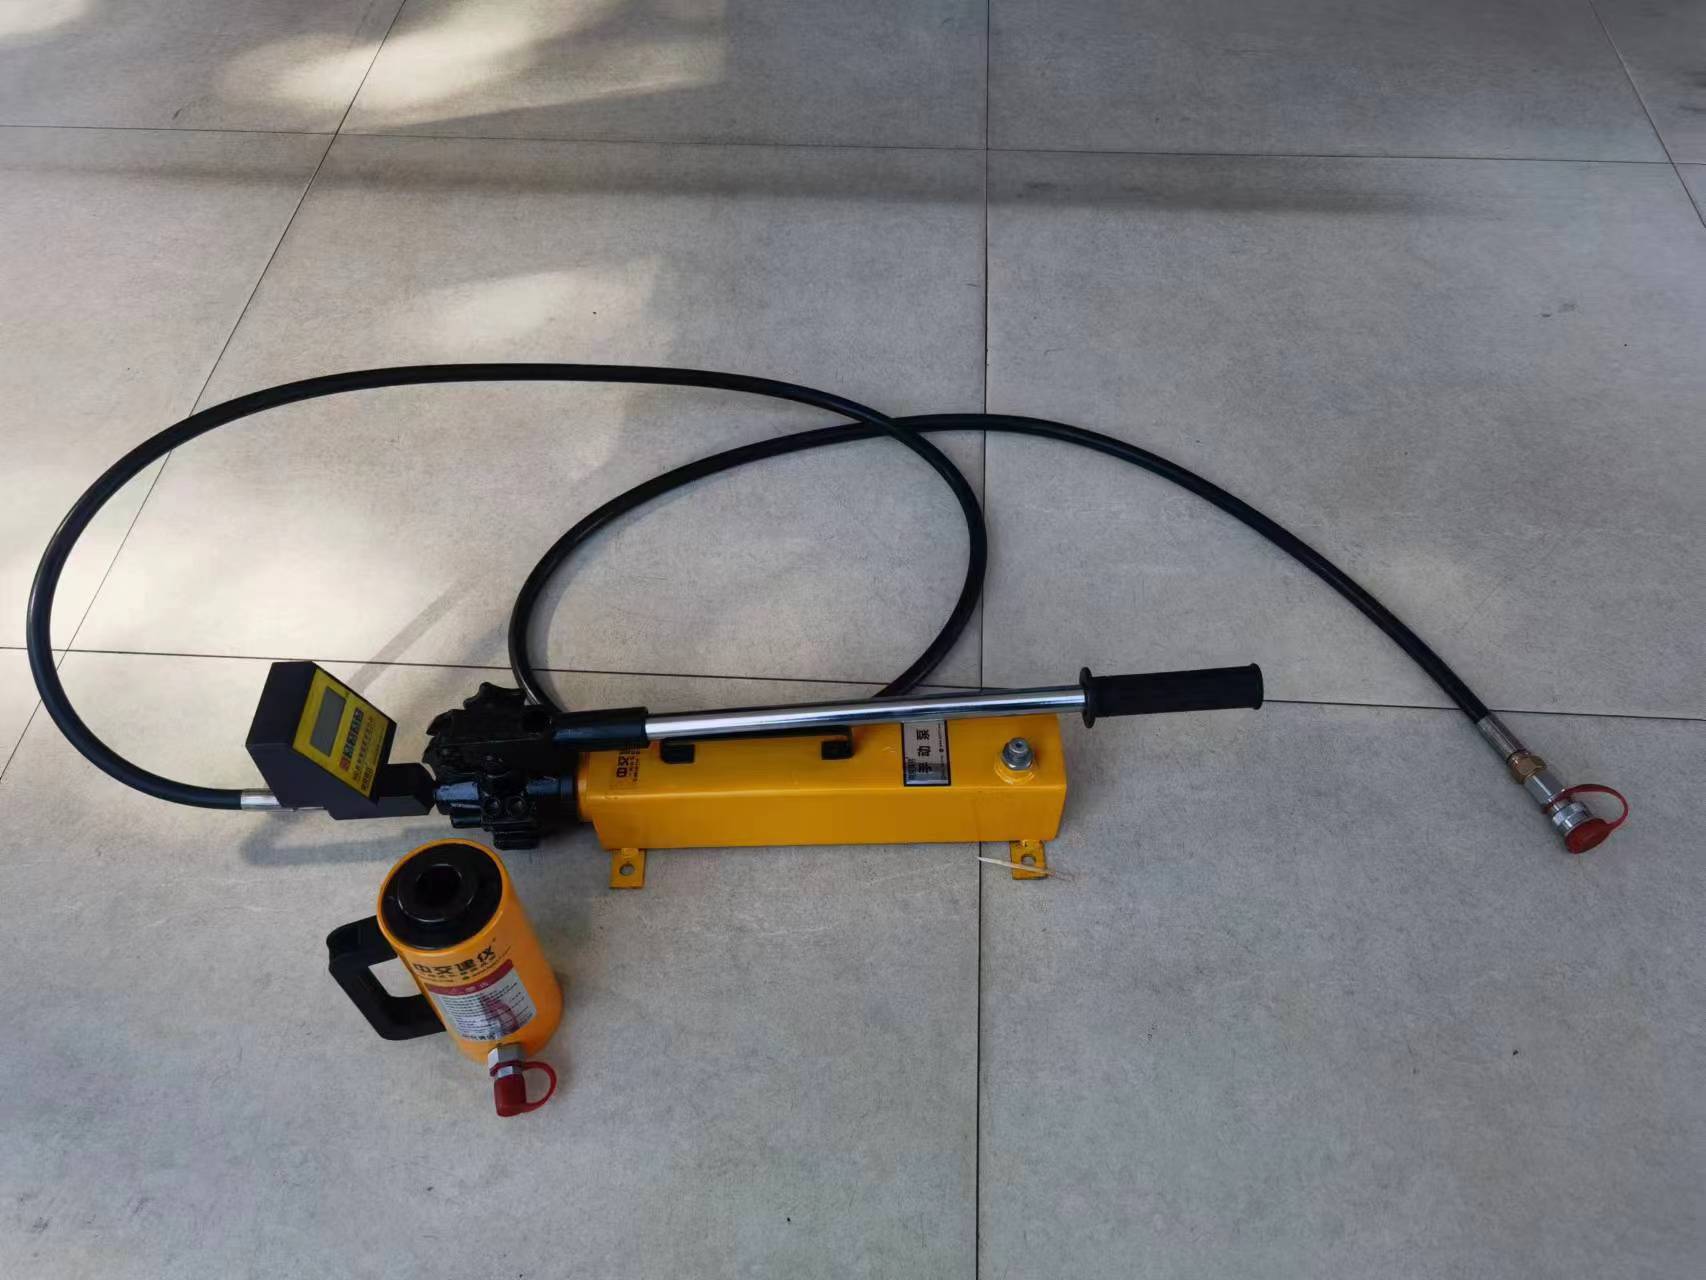 Digital Display Bolt Drawing Instrument
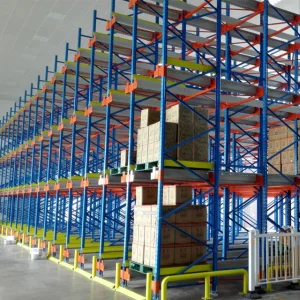
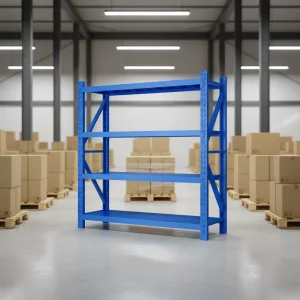
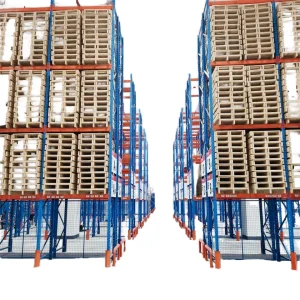
Explore our complete range of certified medium-duty storage racks, laser-guided automated forklifts, and corrosion-protected solutions.
Expert answers regarding custom OEM cold chain logistics solutions, structural specifications, and international shipping standards.
Cold chain storage facilities operate under sub-zero temperatures (down to -30°C) and high humidity. Standard steels become brittle under thermal contraction, and conventional coatings peel off due to condensation. Shenzhen Sunli utilizes specially treated cold-resistant alloy steels combined with multi-layer electrostatic anti-corrosion powder coatings to ensure structural integrity and safety in refrigerated environments.
Yes. As a direct manufacturer with an established 38,000 m² production facility and 28 experienced R&D engineers, we fully support OEM and ODM customization. We tailor upright heights, beam lengths, layer load capacities (ranging from 300kg to 5000kg+ per level), and color powder coatings to meet exact project blueprints.
All our heavy-duty racking systems, automated AS/RS setups, and shelving products are manufactured under strict ISO9001 quality management protocols and hold CE certifications. Our 35 dedicated QC professionals perform rigorous raw material load tests and coating thickness inspections prior to export.
Thanks to our robust supply chain network of over 800 partners and fully automated rolling and welding lines, standard production lead time ranges from 15 to 25 days depending on order volume and specific customization requirements.
 SunliRack