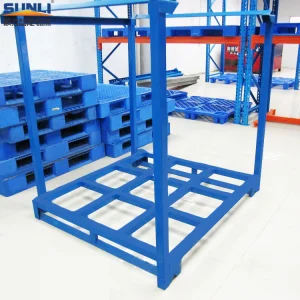
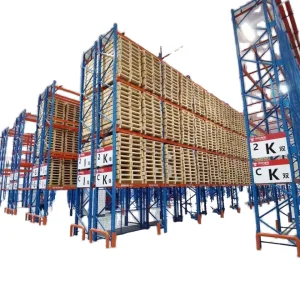
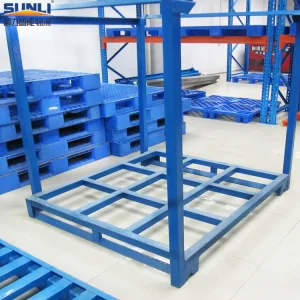
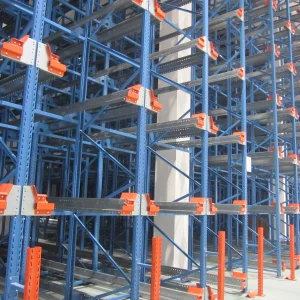
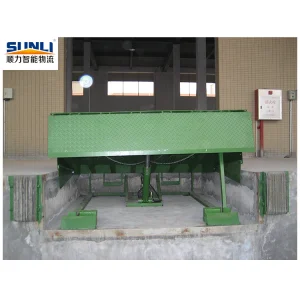
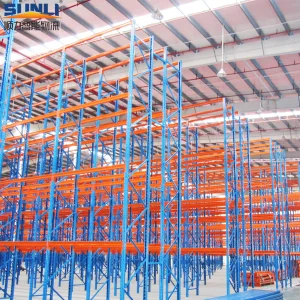
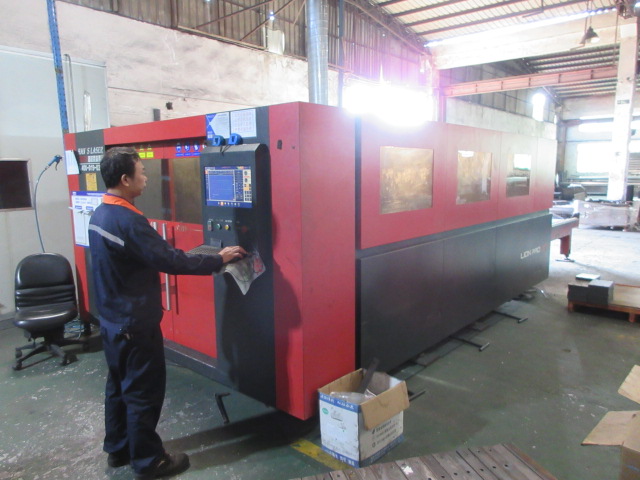
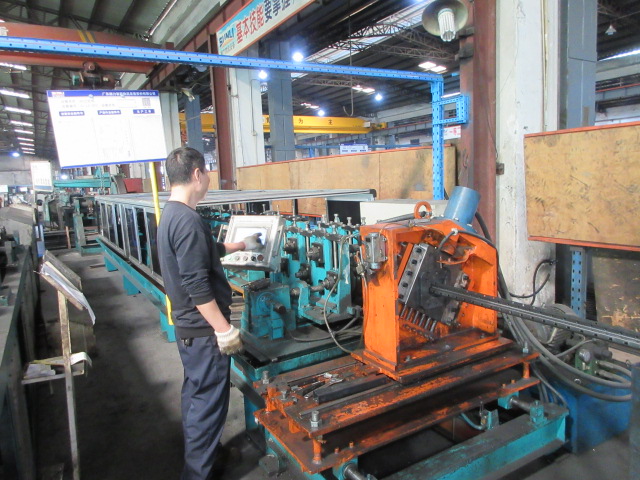
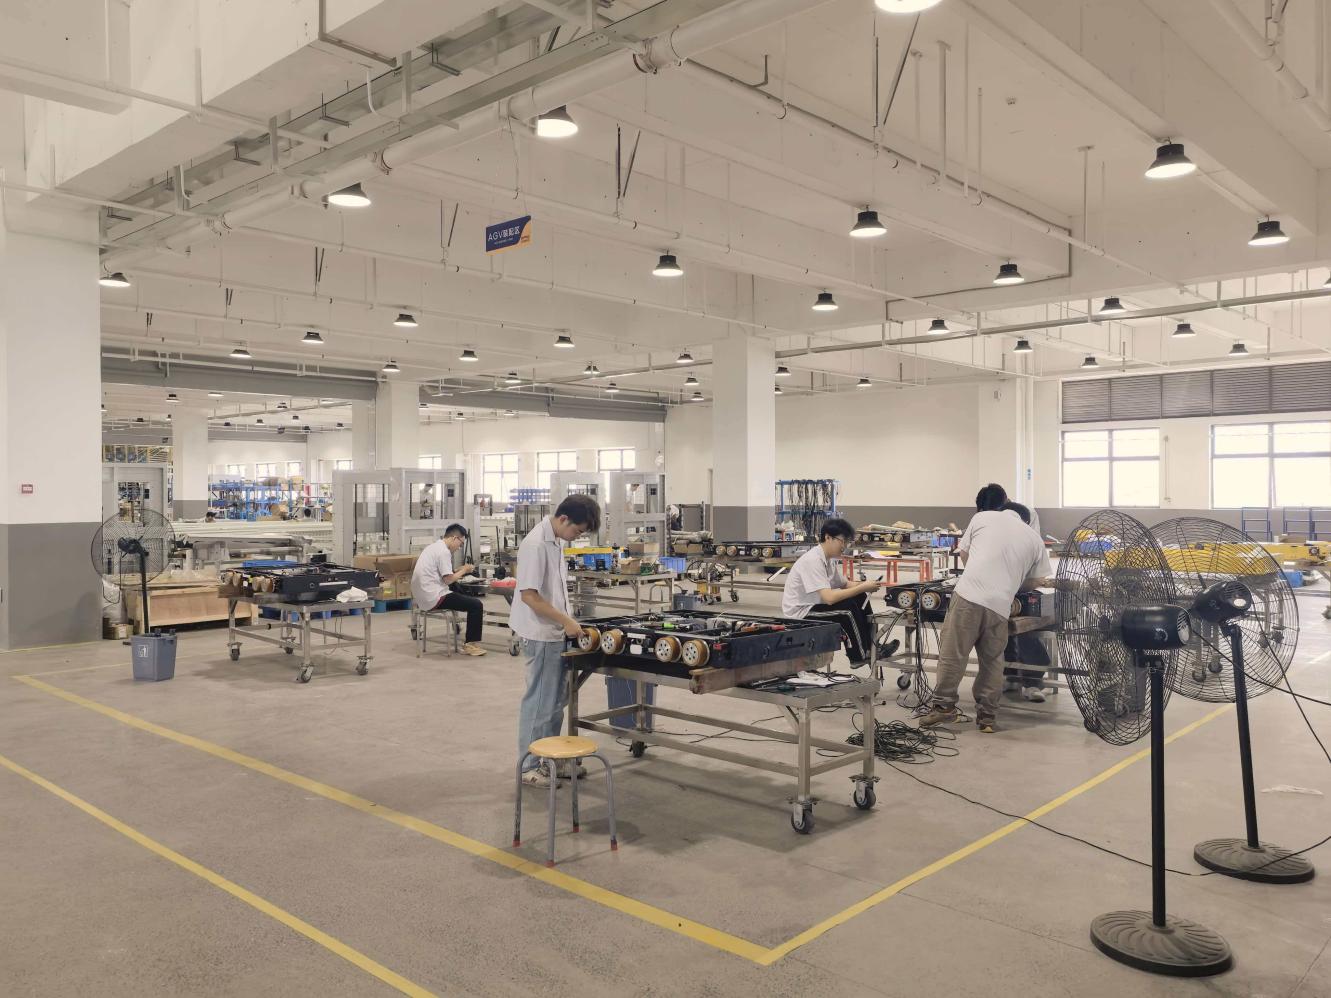
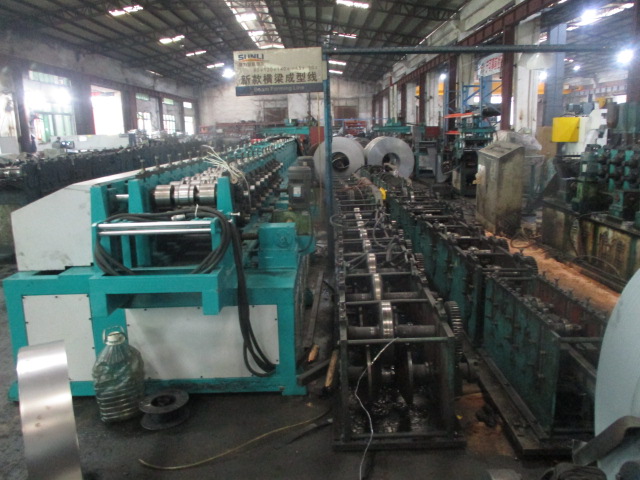
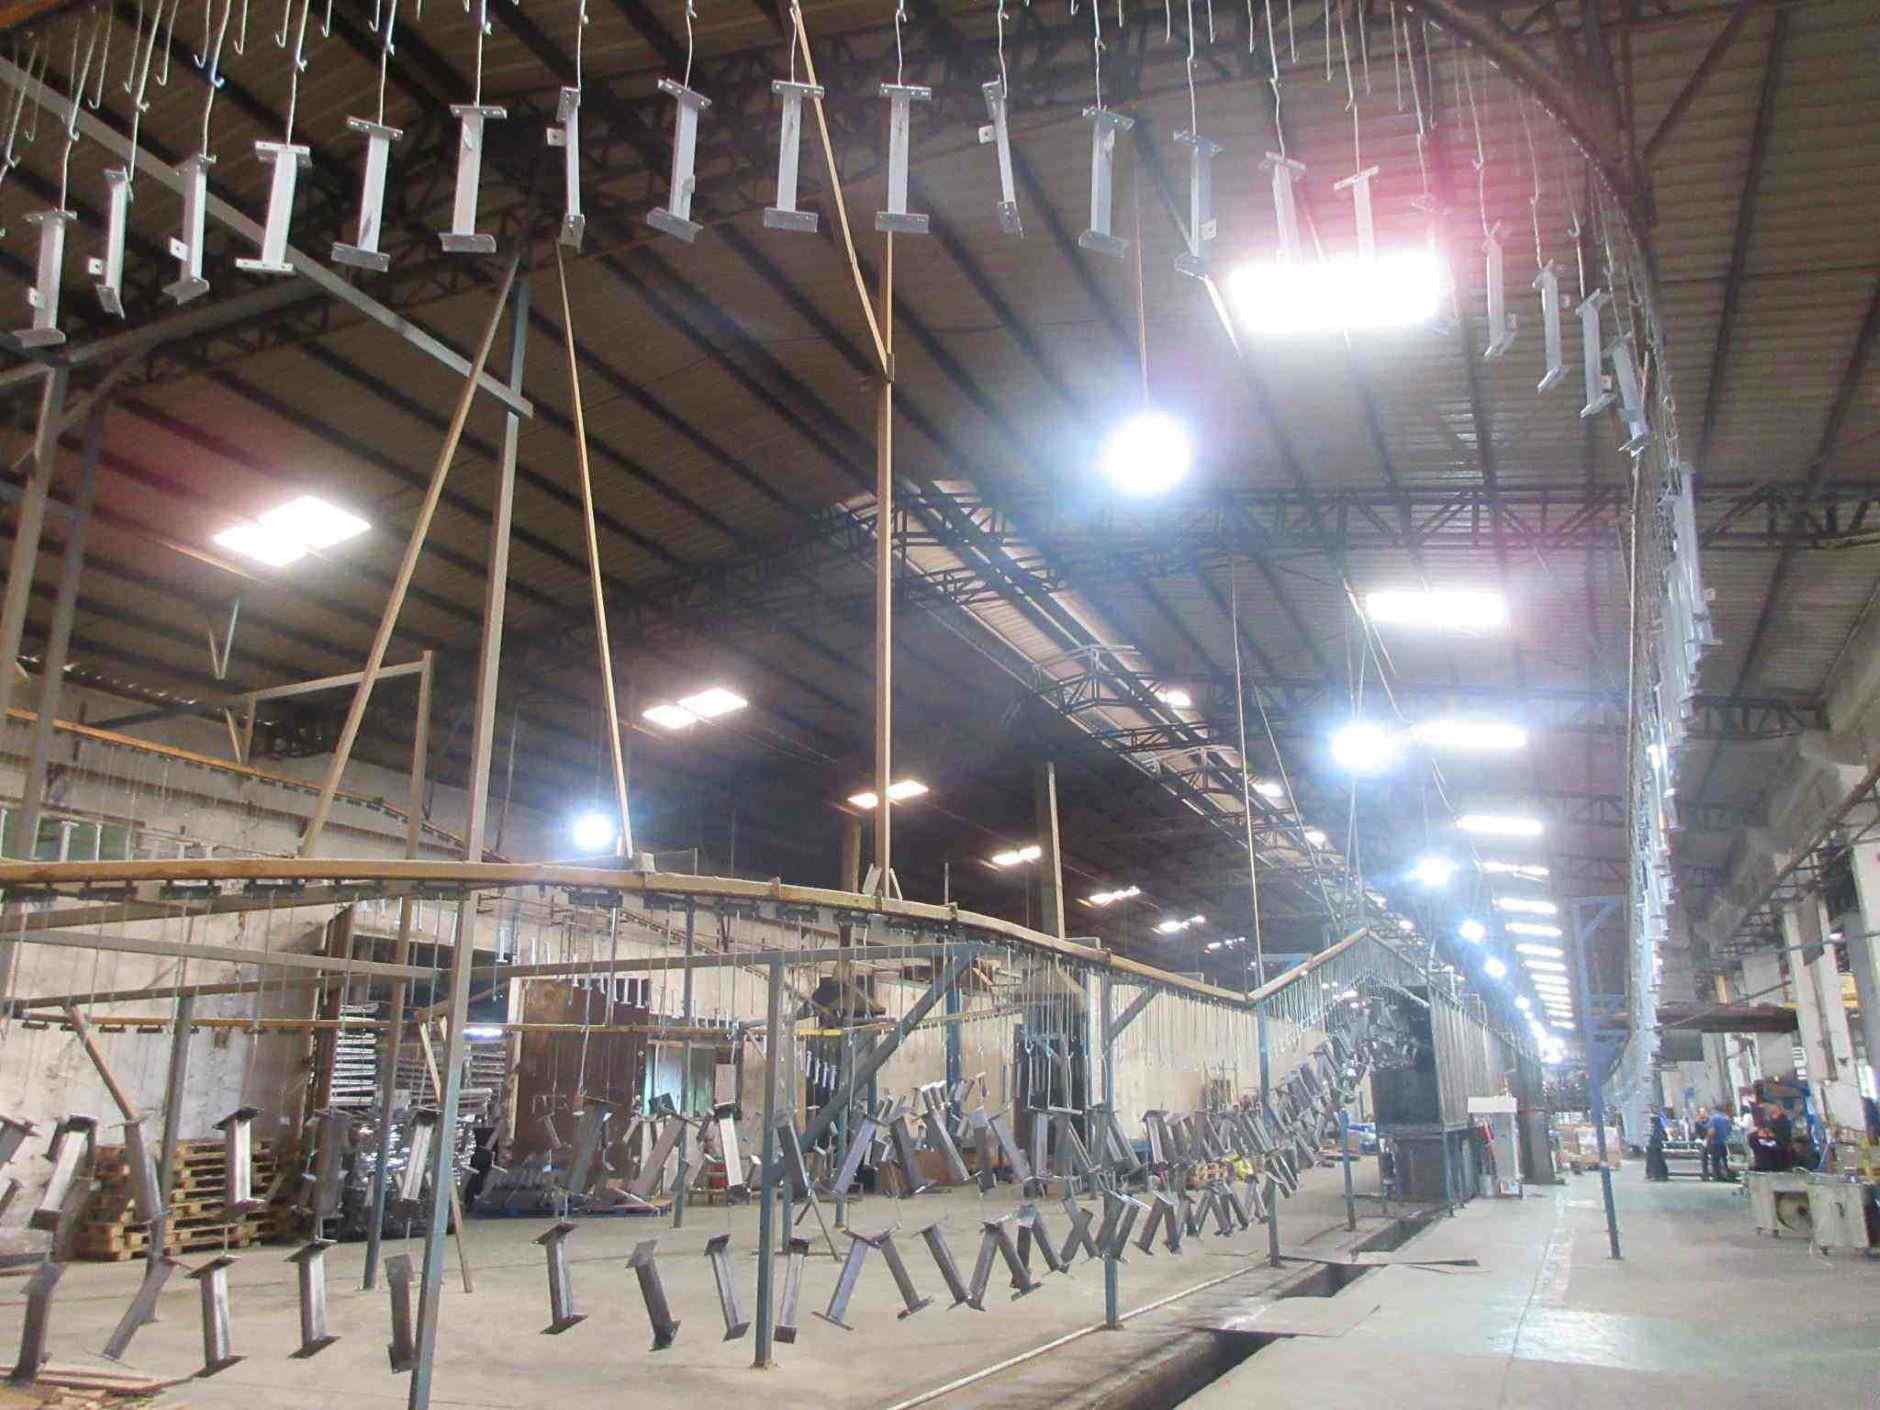
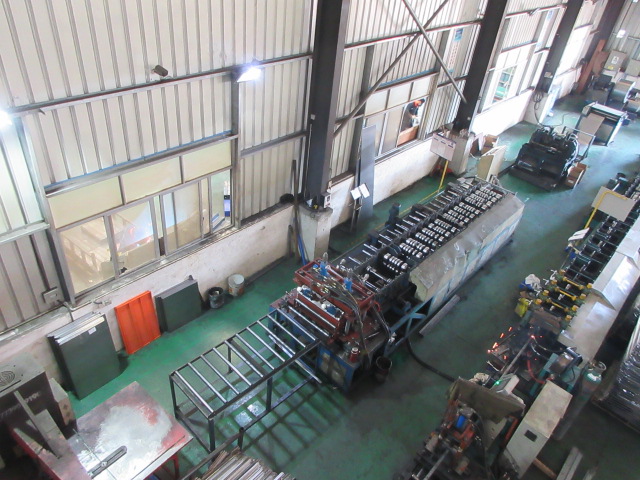
Established in 2015, Shenzhen Sunli Intelligent Logistics Equipment Co., Ltd. is a leading manufacturer specializing in heavy-duty industrial racking and smart warehouse storage solutions. Operating from a modern production facility spanning 38,000 m², we leverage over 12 years of industry experience and 8 years of international trade expertise to serve global logistics and industrial sectors. Our high-performance storage solutions generate an annual export revenue ranging between $18 million and $25 million, with core markets spanning North America, Western Europe, Southeast Asia, and the Middle East.
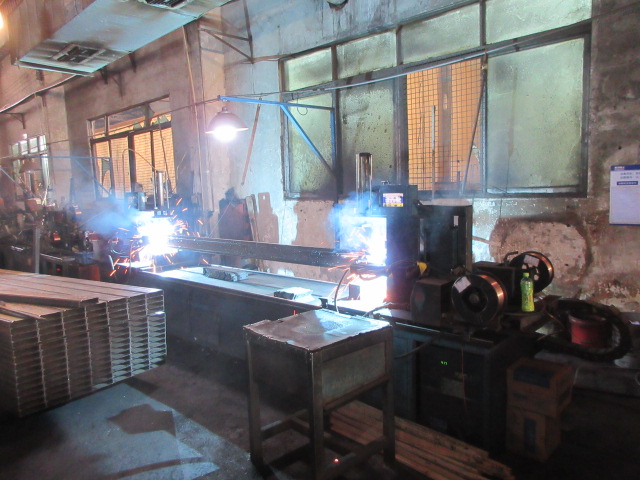
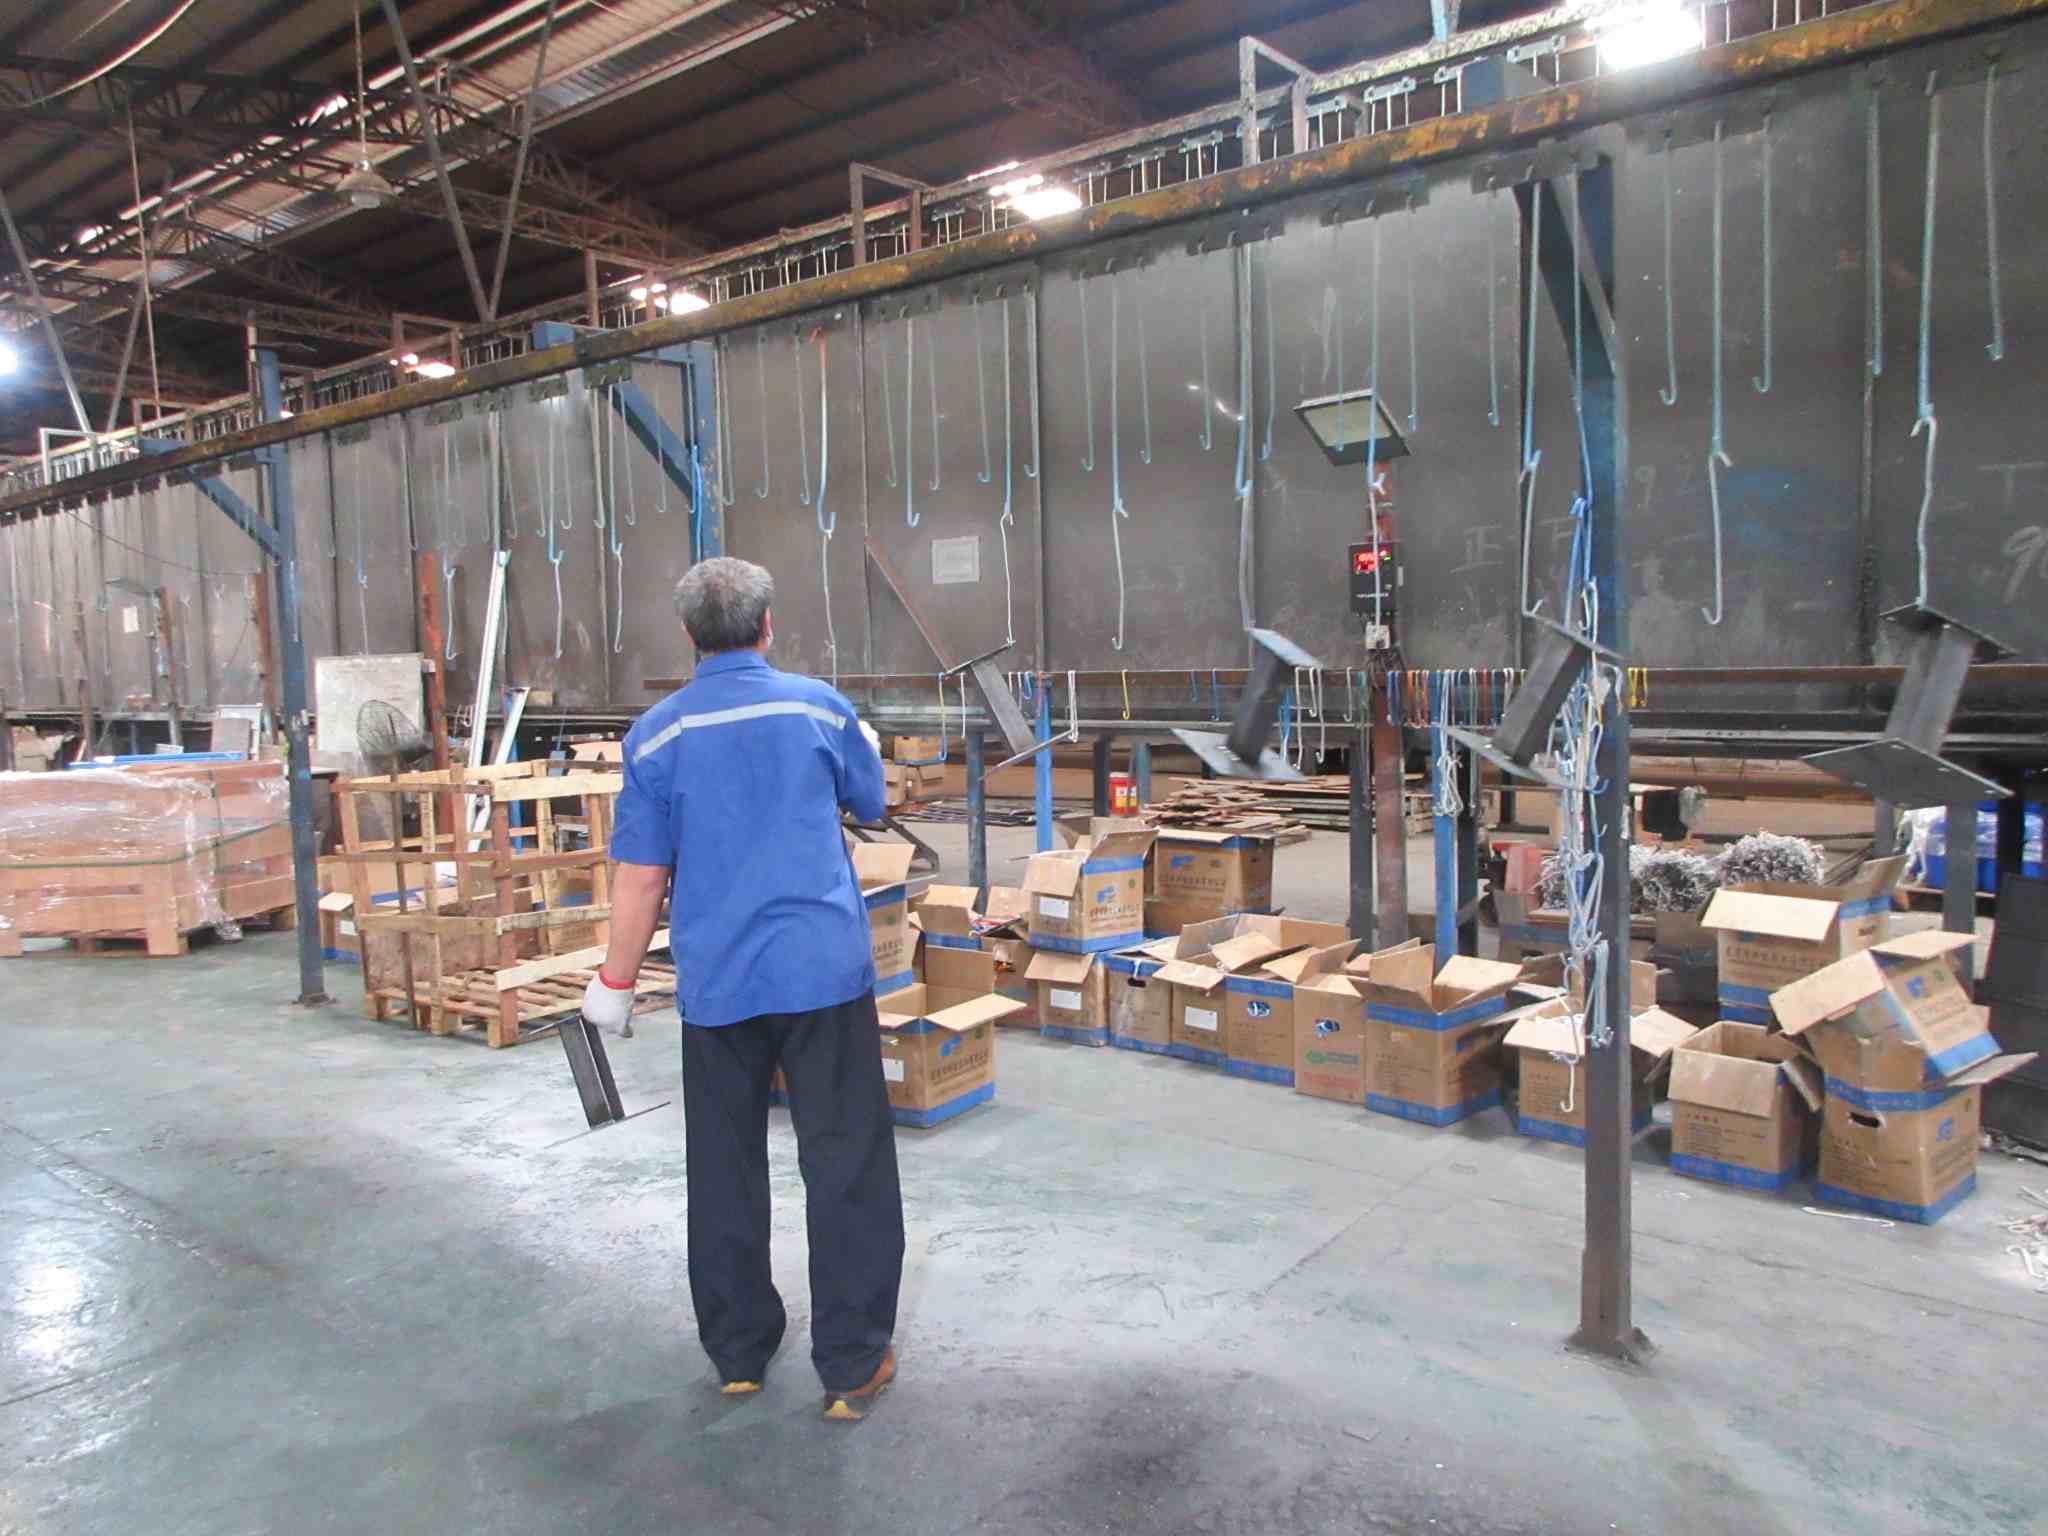
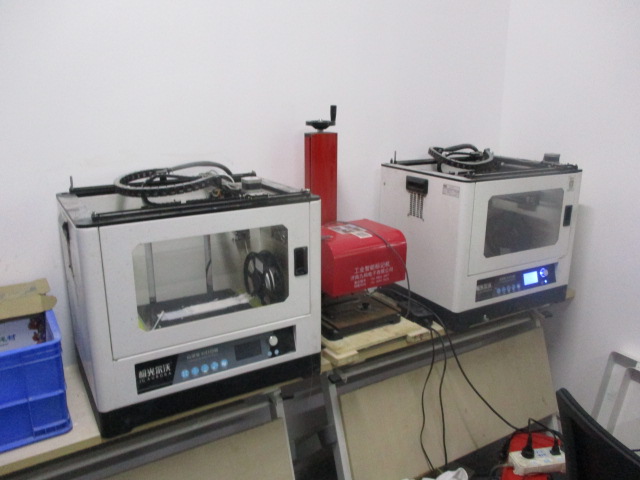
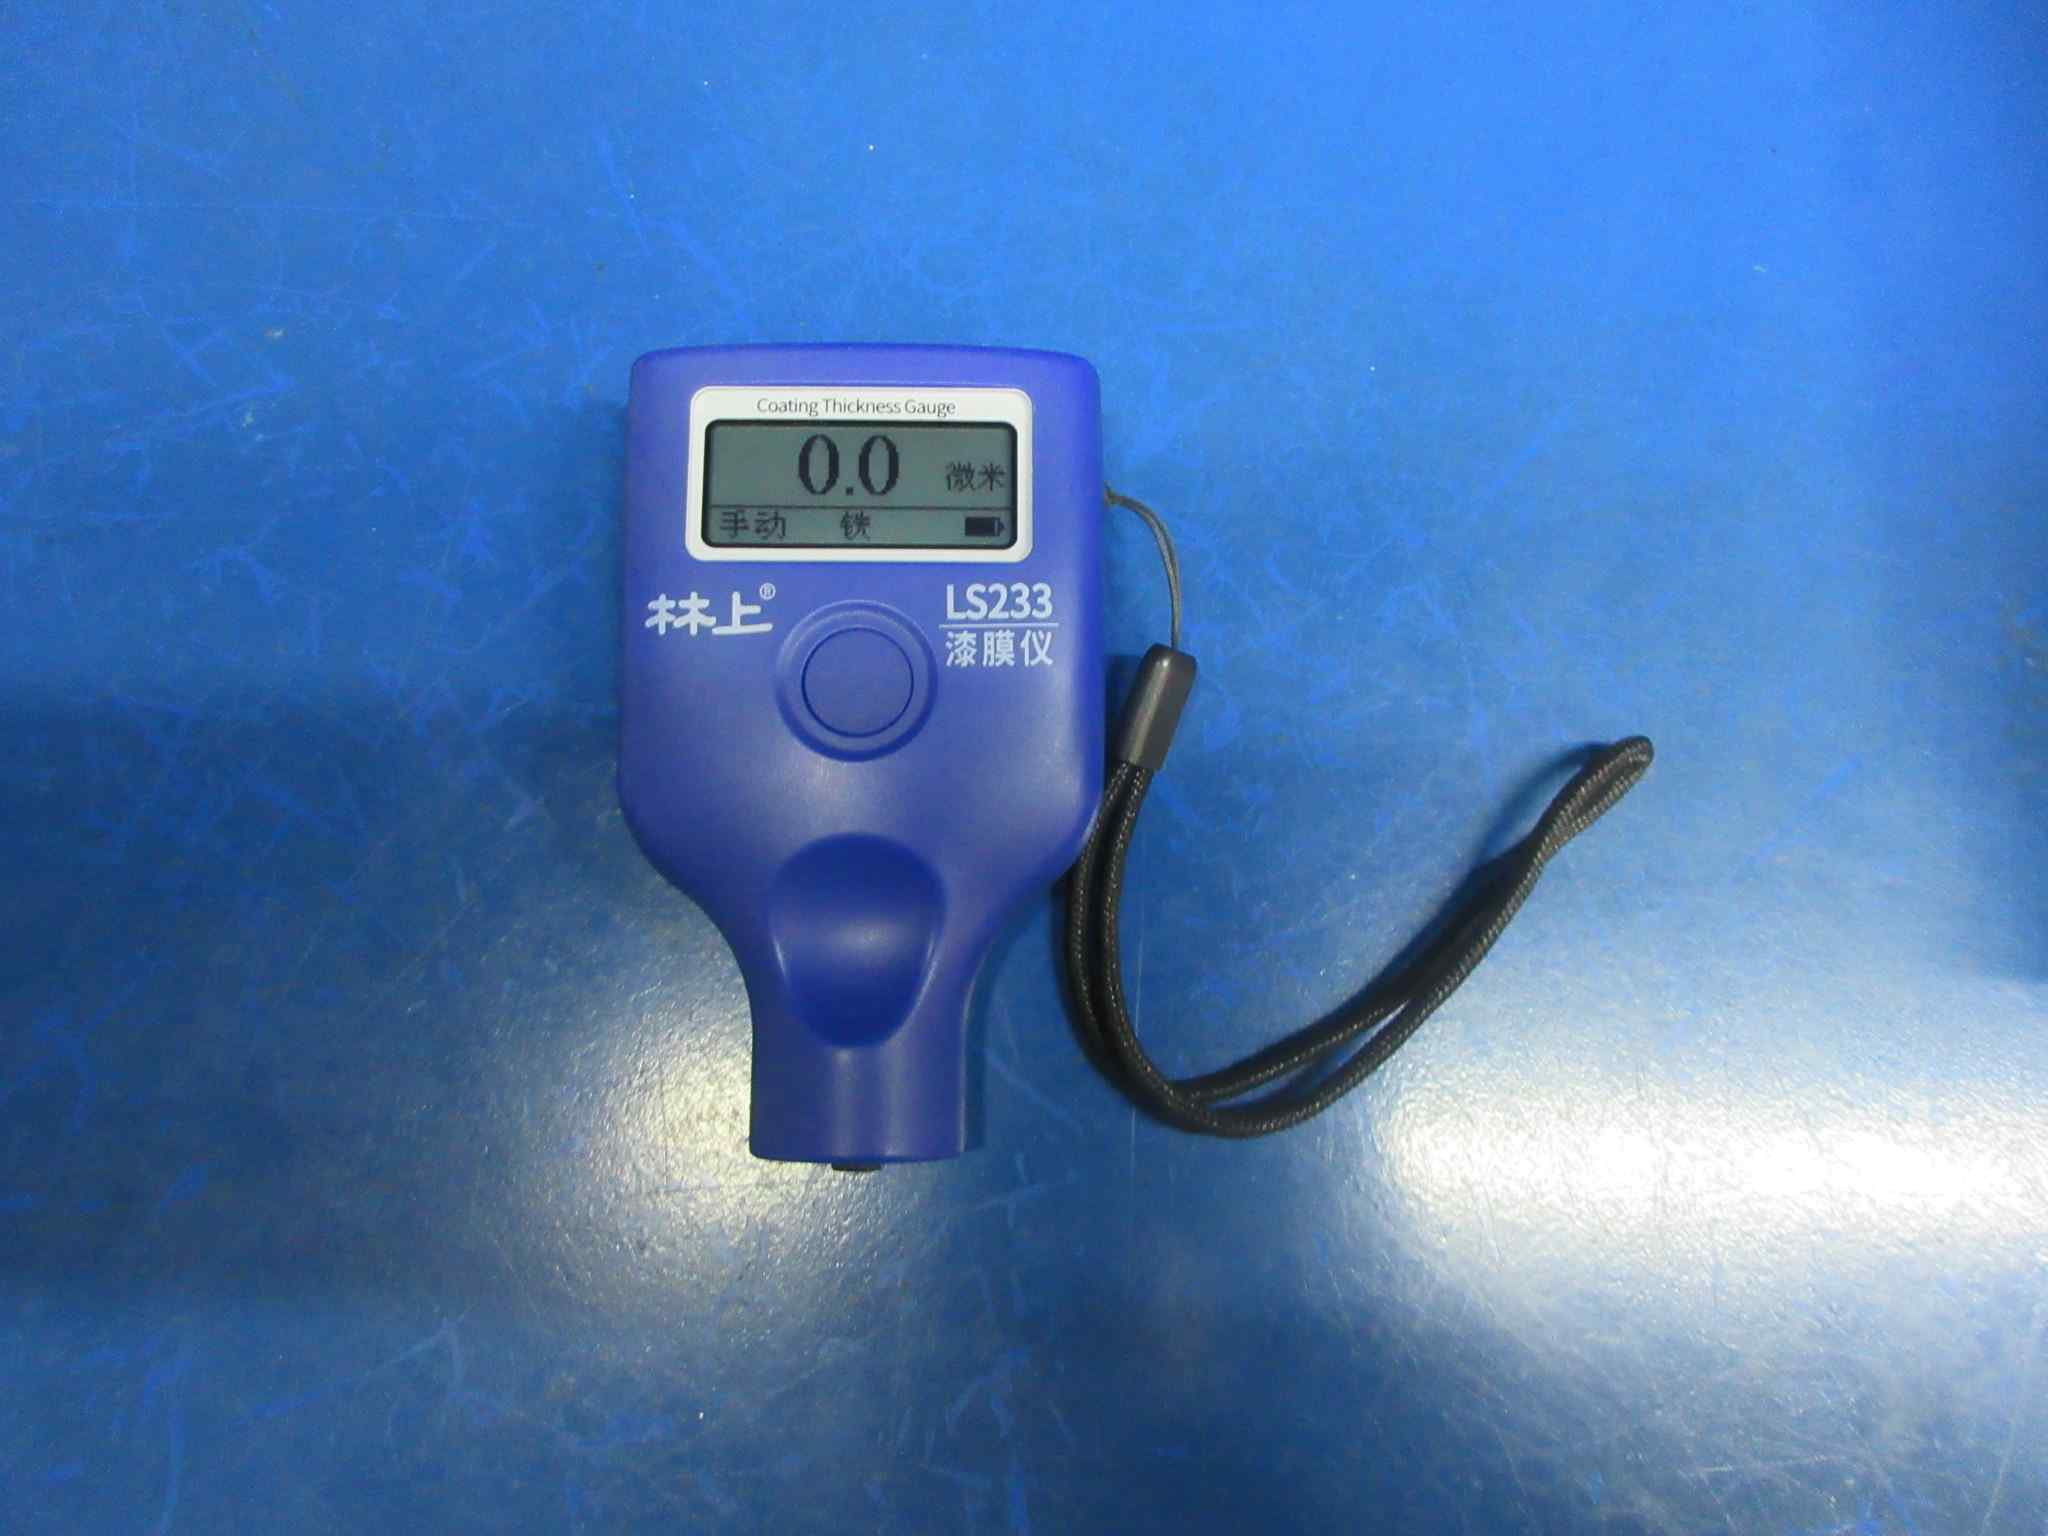
Quality and precision are central to our operations. Our dynamic team of 35 dedicated QC professionals implements rigorous product inspection methods, including full raw material load-bearing analysis, high-precision weld seam testing, and comprehensive anti-corrosion powder-coating thickness checks. Driven by strong R&D capabilities, our team of 28 skilled R&D engineers continuously innovates to meet evolving supply chain requirements, introducing over 120 new products and structural improvements annually.
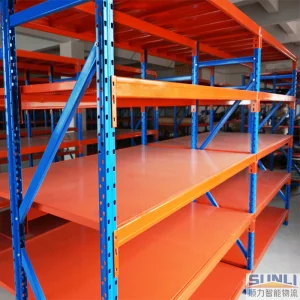
We offer extensive OEM/ODM custom options, including tailored load capacities, custom rack dimensions, color powder coatings, and fully integrated automated shuttle systems (AS/RS). Backed by a strong network of over 800 supply chain partners, we primarily partner with large-scale 3PL providers, industrial distributors, ecommerce logistics hubs, and global retail enterprises to deliver reliable, efficient, and scalable storage infrastructure worldwide.
Global supply chain managers face unprecedented pressures to optimize space utilization, slash transit vulnerabilities, and scale warehousing capabilities securely. Industrial shipping containers, heavy-duty racking, and automated storage and retrieval systems (AS/RS) form the structural backbone of modern cross-border logistics.
Enterprise procurement teams look for certified OEM/ODM manufacturers capable of delivering structural integrity under heavy loads, adherence to rigorous international standards (such as ISO, CE, and AS4084), and seamless integration with warehouse management systems (WMS). Sunli provides custom engineering specifications tailored to high-density storage and harsh operating environments.
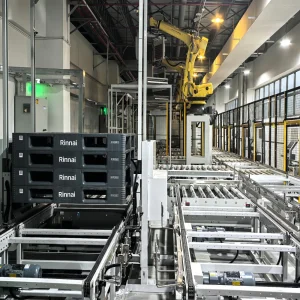
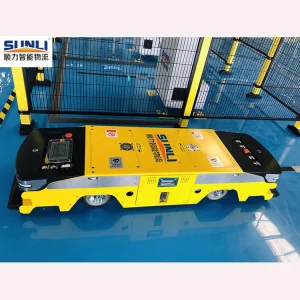
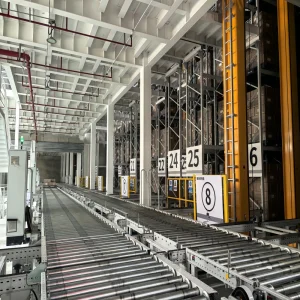
Our macro logistics ecosystem integrates modular steel containers, heavy pallet racking, automated guided vehicles (AGVs), and radio shuttle technology into a unified architecture. This eliminates operational bottlenecks, increases pick-and-pack efficiency by up to 45%, and guarantees structural safety across multi-tier distributions.
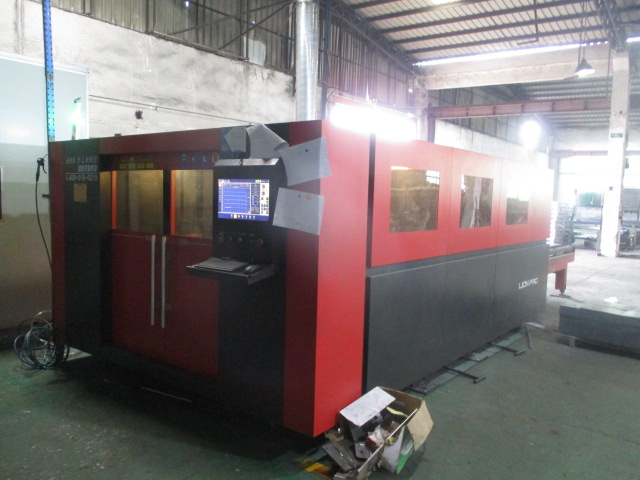
By leveraging Q235B high-grade structural steel and automated robotic welding lines, every component undergoes stringent stress testing to withstand dynamic load constraints, seismic safety requirements, and continuous industrial duty cycles.
As the logistics sector transitions toward autonomous lights-out warehousing, Sunli is pioneering next-generation smart storage frameworks. Our R&D division is actively deploying IoT-enabled sensors embedded within structural racks and shipping container modules, providing real-time data on load shifting, environmental humidity, and structural fatigue.
The integration of AI-driven predictive maintenance algorithms ensures zero downtime for automated material handling systems. Furthermore, our sustainable manufacturing initiative incorporates eco-friendly powder-coating formulations and solar-powered rolling lines, ensuring compliance with upcoming global carbon-neutral mandates and green supply chain standards.
Operating on a global scale demands localized compliance and responsive technical assistance. Sunli maintains regional engineering consultants across North America, Europe, and Asia-Pacific to assist with on-site installation planning, local building code verification, and seismic engineering calculations.
Our products comply with strict international regulatory standards, including FEM (European Federation of Materials Handling), RMI (Rack Manufacturers Institute), and ISO9001 quality management certifications. Clients benefit from end-to-end project management, custom export packaging, and dedicated after-sales maintenance support.
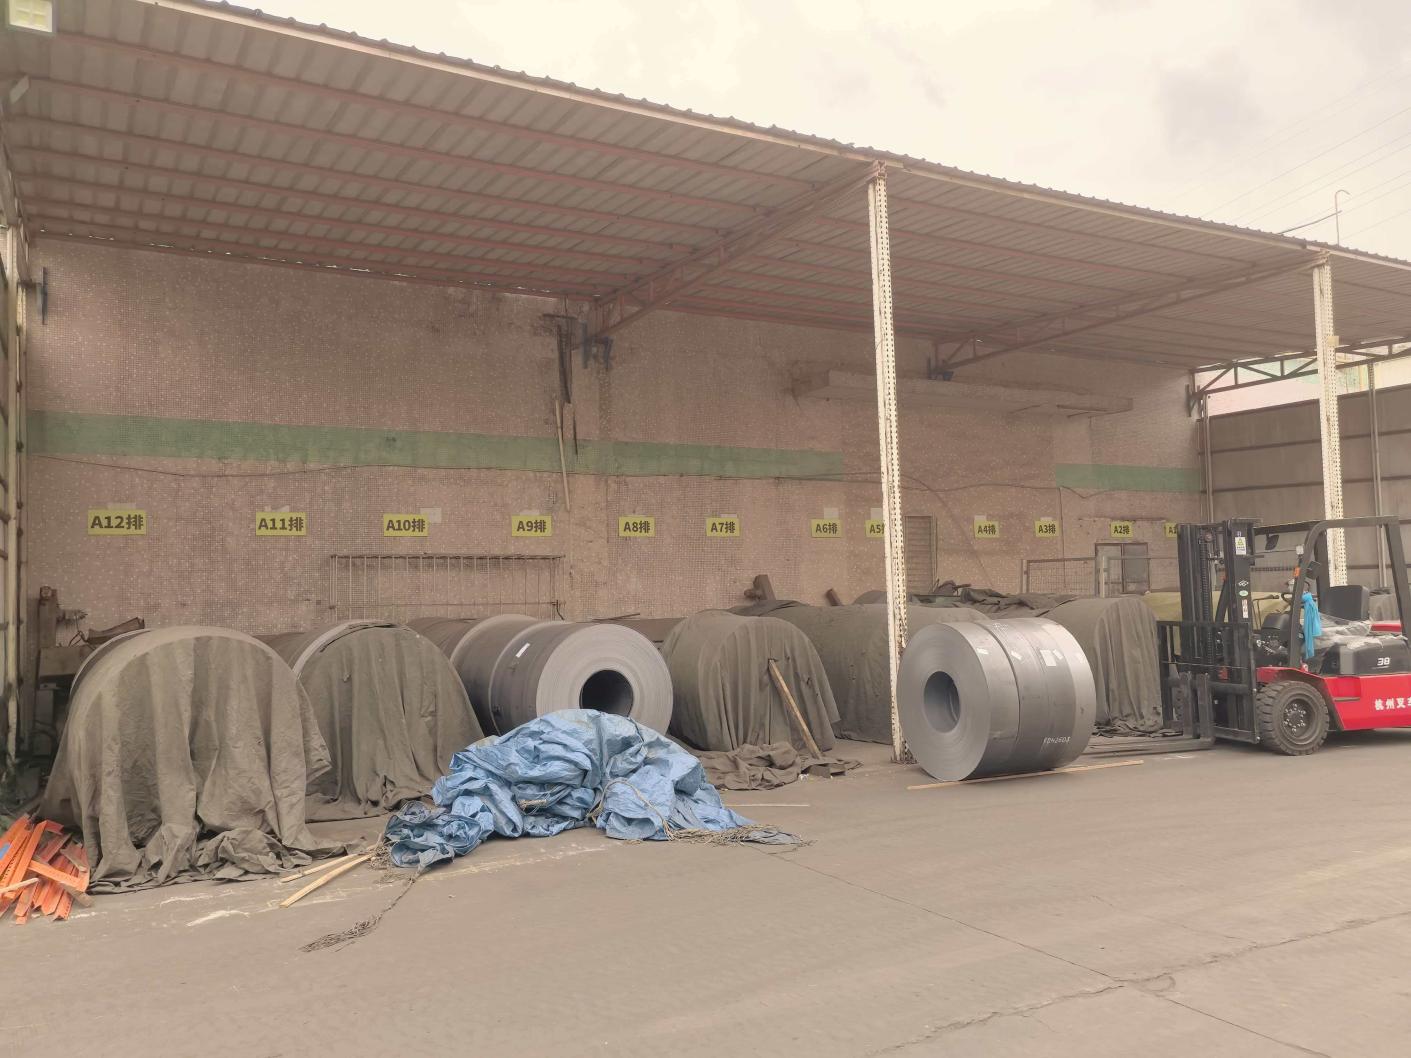
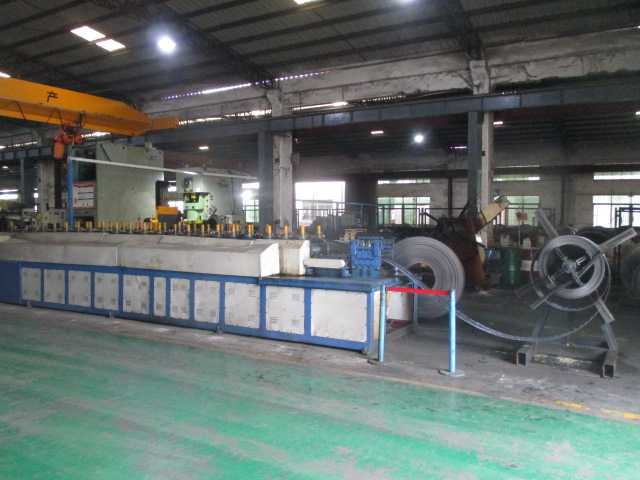
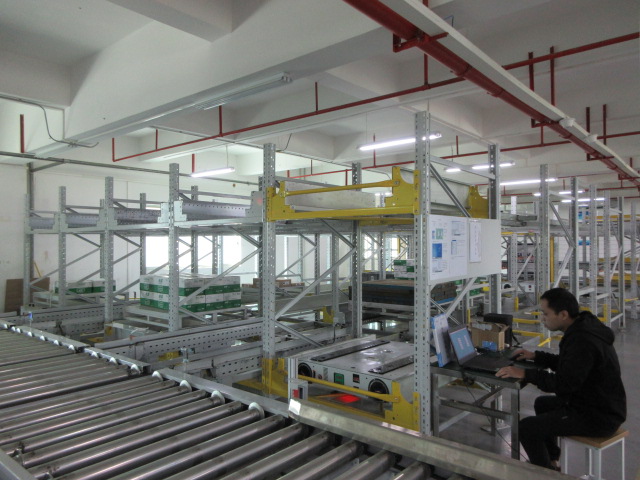
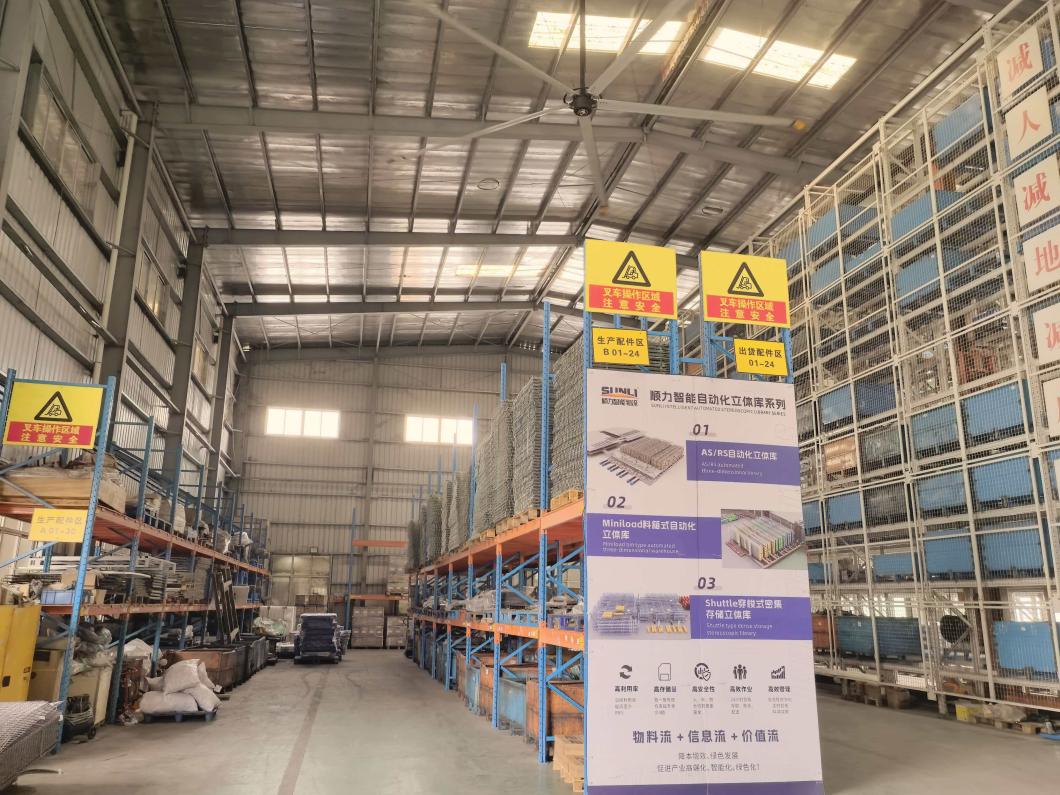
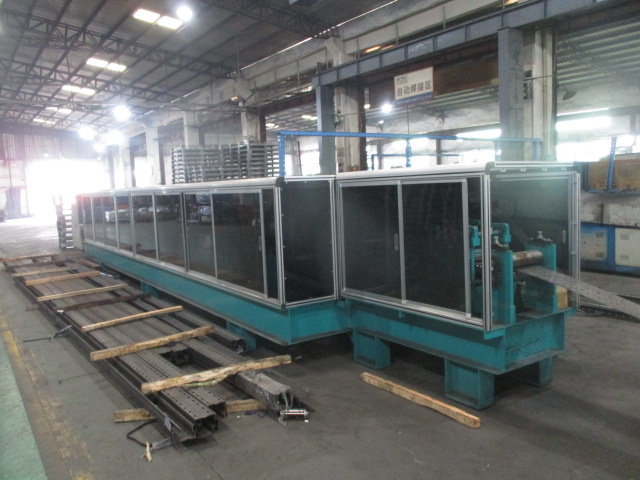
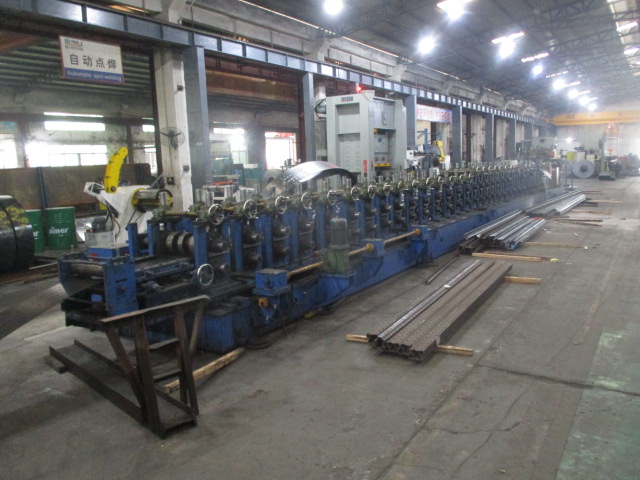
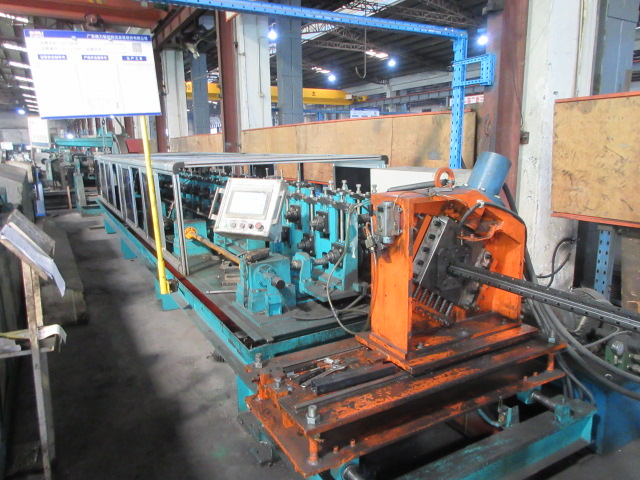
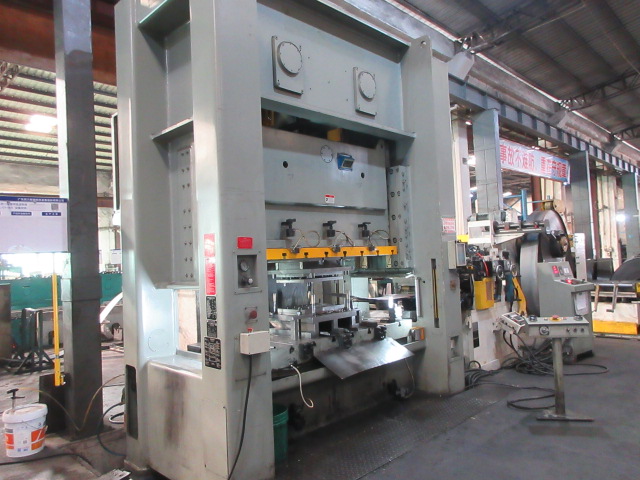
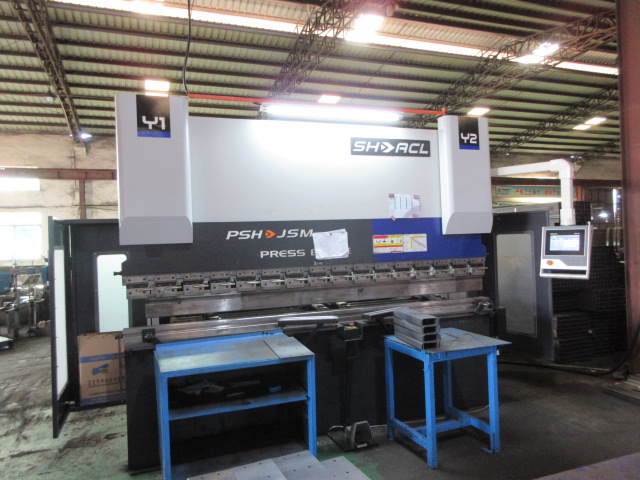
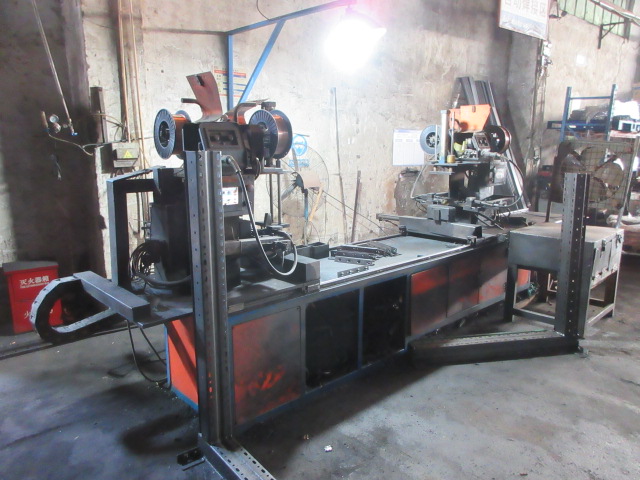
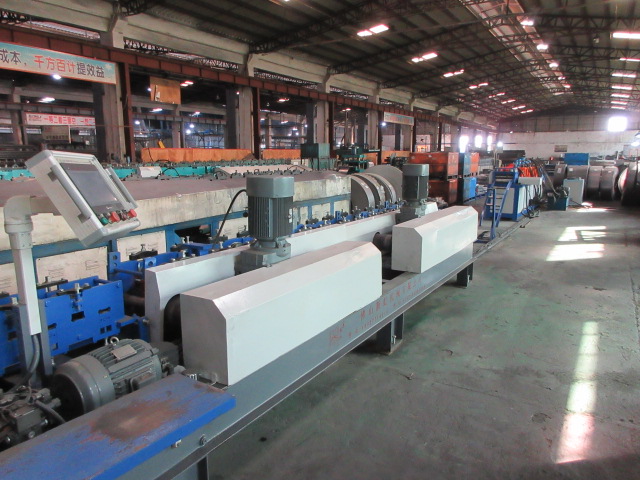
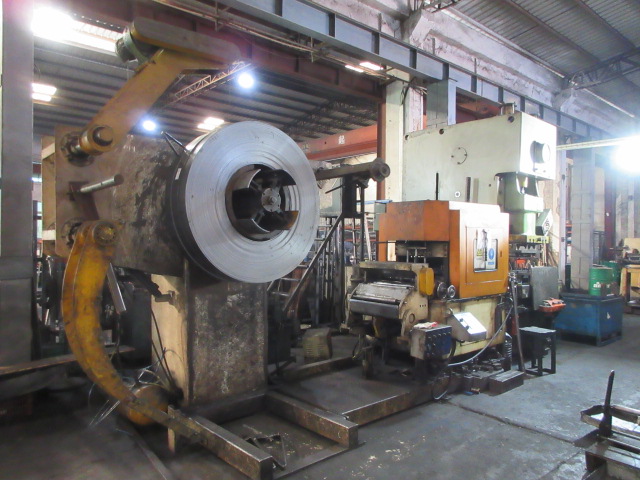
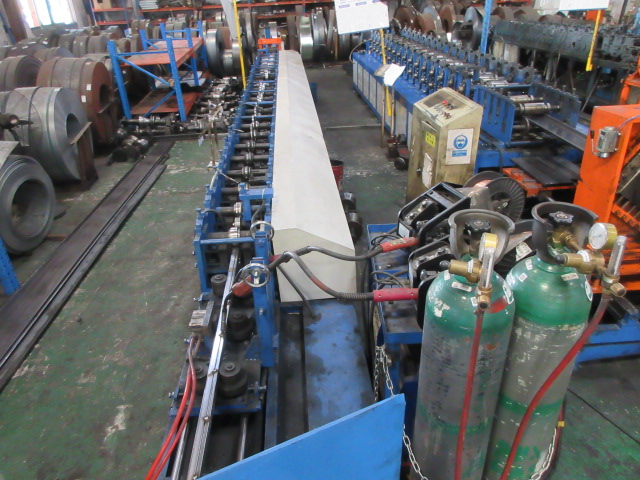
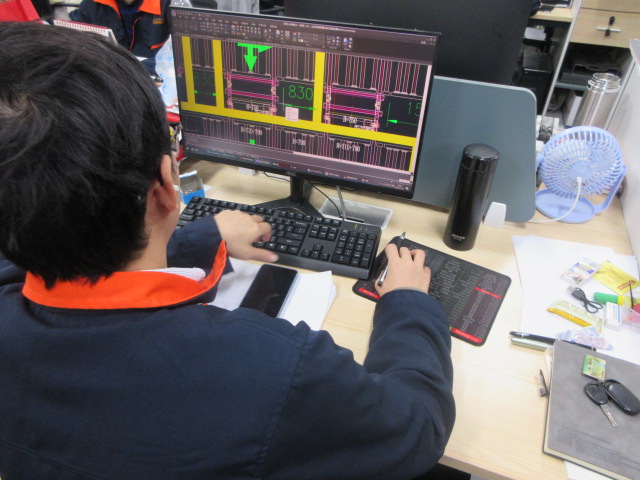
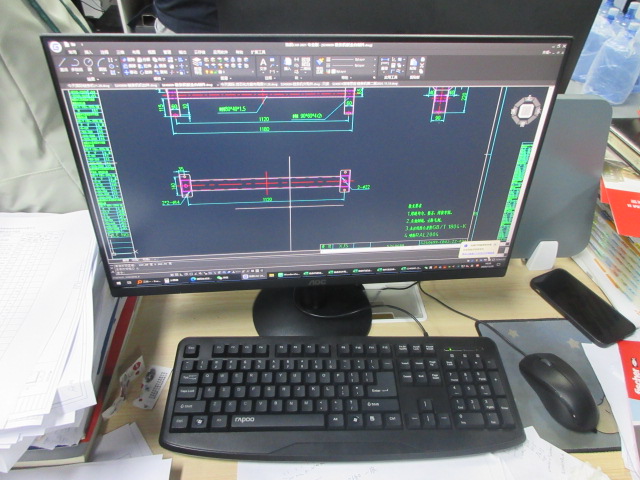
We provide full customization including tailored load capacities (up to 2000kg+ per tier), specialized dimensions, custom RAL color powder coating, corrosion-resistant alloy steel selection, and integration with automated AS/RS and radio shuttle systems.
Standard production lead times range from 15 to 30 days depending on order volume and customization complexity. Our 38,000 m² facility and 800+ supply chain partners ensure rapid turnaround and stable global shipping.
Our 35-member QC team conducts raw material load testing, precision weld seam analysis, and coating thickness checks. Our manufacturing processes comply with ISO9001, FEM, and RMI international quality and safety benchmarks.
We partner with large-scale 3PL providers, industrial distributors, and retail hubs by delivering scalable warehouse infrastructure, local engineering support, seismic calculations, and robust after-sales installation guidance.
 SunliRack